/author/lin-qiaoyu-international-sales-manager/

News
Products & Solutions
CONTACT US

+86-18068757376

blk@jsblk.com

No. 29 North Tongjiang Road, Xinbei District, Changzhou City, Jiangsu Province, China
Vacuum freeze-drying is one of the most demanding technologies used to stabilize temperature-sensitive products. It enables water removal at low temperature while preserving structure, activity, reconstitution performance, and other critical quality attributes. However, successful freeze-drying development requires more than a vacuum chamber and a refrigeration unit. Researchers need accurate shelf-temperature control, reliable condensation capacity, stable vacuum performance, repeatable process conditions, hygienic construction, and a practical path from laboratory experimentation to pilot and commercial production.
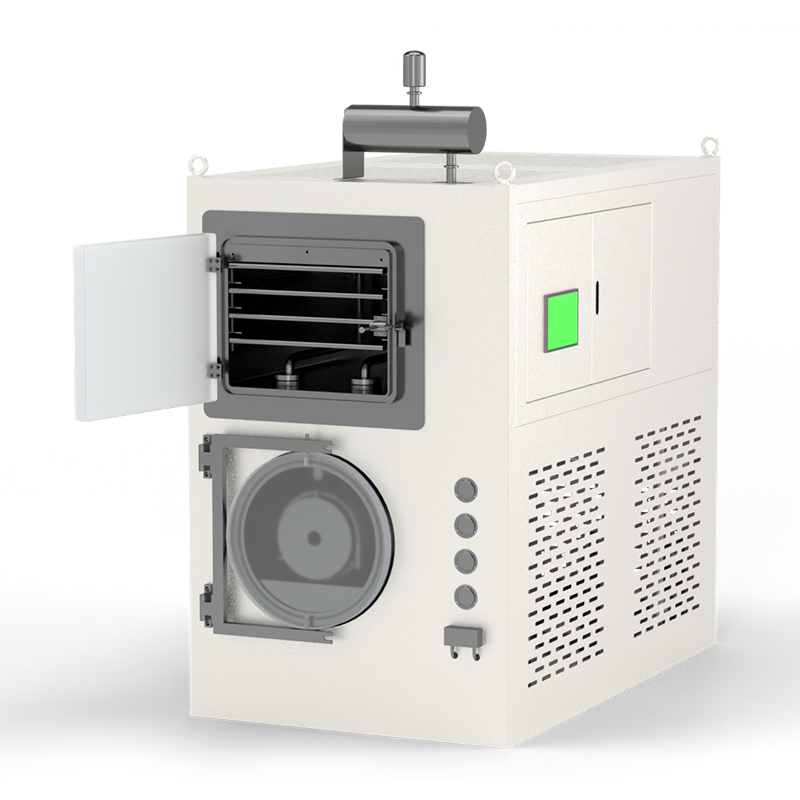
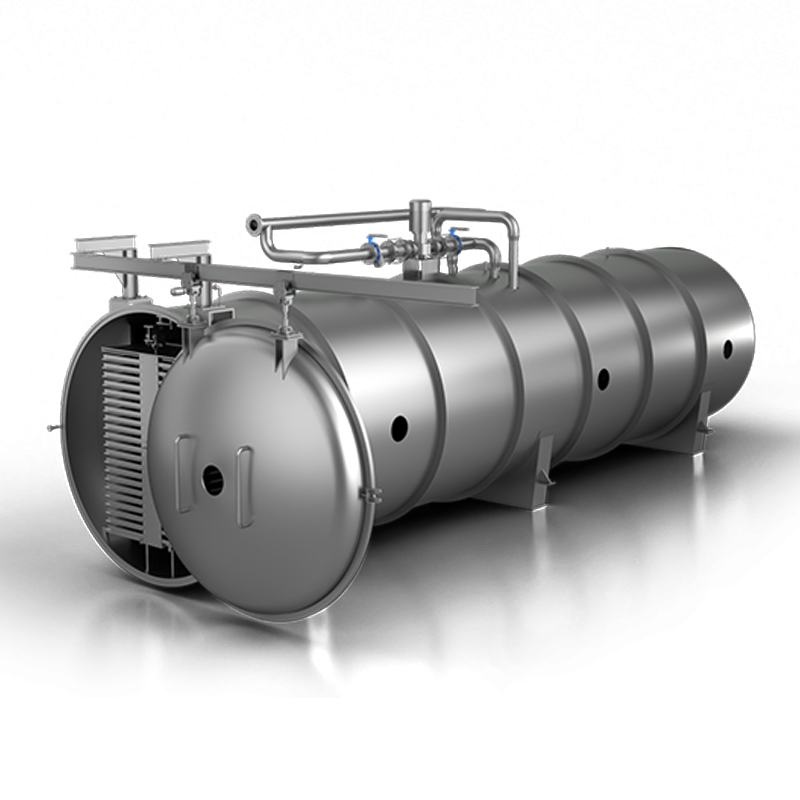
The BLK-FD-2 R&D scale vacuum freeze dryer is designed to address these requirements. With a 2 square meter freeze-drying area, a typical loading capacity of 20 kilograms, and a liquid loading capacity of 40 liters, it provides a substantial development platform for pharmaceutical, biotechnology, food, nutraceutical, chemical, and biological sample applications. Its configuration bridges the gap between small laboratory freeze dryers and large industrial lyophilizers, allowing development teams to generate more representative process data before committing to full-scale production equipment.
Manufactured by Jiangsu BoLaiKe Refrigeration Science and Technology Development Co., Ltd., the BLK-FD-2 combines industrial-style engineering with the flexibility expected from research equipment. It can be configured with integrated or separate pre-freezing and drying functions, uses bidirectional silicone-oil circulation for shelf heating and cooling, and incorporates a patented cold-trap design intended to improve water-capture performance. These characteristics make the system suitable for process screening, formulation development, scale-up studies, pilot production, and selected small-batch manufacturing operations.
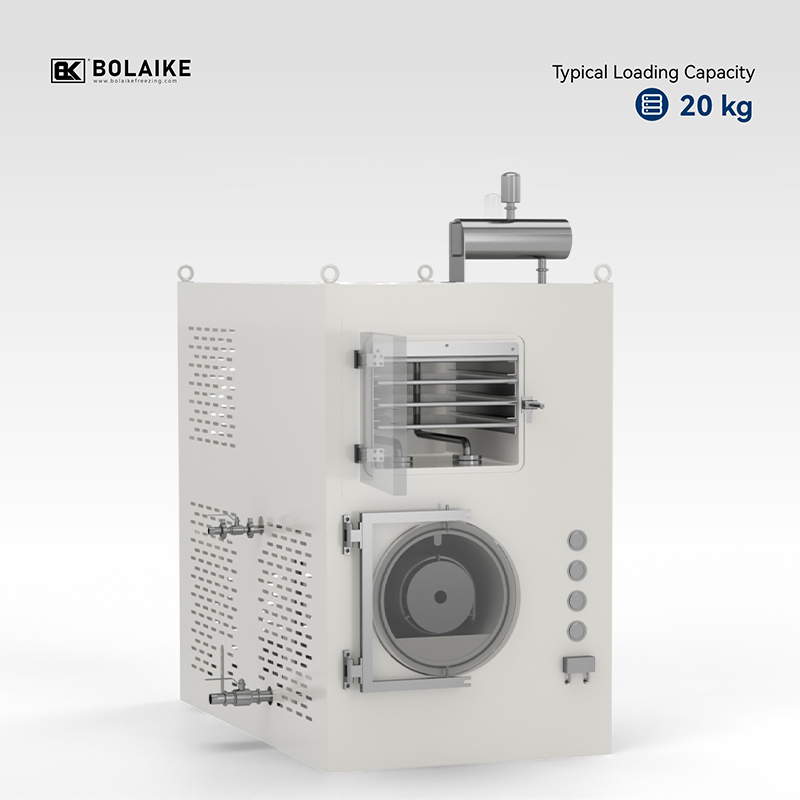
BLK-FD-2
Freeze-drying, also called lyophilization, generally consists of three main stages: freezing, primary drying, and secondary drying. During freezing, the product is cooled until most of its free water forms ice. During primary drying, the chamber pressure is reduced and controlled heat is supplied to the product. Ice then sublimates directly into vapor and is captured on a low-temperature condenser. During secondary drying, additional bound moisture is removed to achieve the required residual-moisture level and storage stability.
Each stage influences the final product. The freezing rate can affect ice-crystal size, pore structure, cake appearance, reconstitution time, and biological activity. Primary drying determines whether the product remains below its critical temperature and whether collapse or melt-back occurs. Secondary drying affects residual moisture, potency, stability, and shelf life. Because these factors interact, a development freeze dryer must provide accurate and repeatable control rather than simply delivering low temperature and vacuum.
Small laboratory units are useful for early formulation screening, but their limited loading area may not adequately represent industrial heat and mass transfer conditions. Large production systems, by contrast, require major capital investment and are not always practical for exploratory work. The BLK-FD-2 occupies the intermediate development range. Its 2 square meter shelf area permits larger and more representative batches, while its research-oriented controls and flexible configuration support experimentation with different formulations, vial loads, trays, cycle recipes, and process parameters.
This scale is particularly valuable for pharmaceutical and biotechnology organizations. A development team can evaluate a formulation with a batch size large enough to identify nonuniformity, edge effects, loading patterns, and condenser-load limitations before transferring the process to a manufacturing freeze dryer. The resulting knowledge can reduce scale-up uncertainty, improve cycle design, and help establish a more robust control strategy.
The BLK-FD-2 is engineered as a square-integral vacuum freeze dryer with a compact but substantial footprint. Its principal specifications are summarized below.
| Parameter | BLK-FD-2 Specification |
|---|---|
| Product category | Experimental freeze dryer |
| Freeze-drying area | 2 square meters |
| Typical loading capacity | 20 kilograms |
| Liquid loading capacity | 40 liters |
| Overall dimensions | 1,800 × 1,000 × 2,000 millimeters |
| Shelf-temperature range | -55°C to +80°C |
| Refrigeration-panel temperature | Minimum -70°C |
| Ultimate vacuum | Less than or equal to 10 Pa, depending on stated test condition |
| Heating and cooling method | Silicone-oil bidirectional circulation with electric heating |
| Typical installed power | Approximately 7 kW |
The combination of a 2 square meter tray area and a 20 kilogram typical load provides a useful ratio between development flexibility and operating practicality. The 40 liter liquid capacity is also important for formulations that must be evaluated at a meaningful batch volume. Depending on fill depth, container format, product density, and process design, users can adapt the chamber to vials, trays, bottles, bulk material, or other suitable product containers.
The stated shelf range from -55°C to +80°C supports both freezing and drying operations. The lower range is suitable for many aqueous formulations and biological products, while the upper range provides flexibility for secondary drying and for products requiring elevated desorption temperatures. The minimum refrigeration-panel temperature of -70°C supports efficient vapor condensation and helps protect vacuum stability during high-moisture stages.
The stated ultimate vacuum of less than or equal to 10 Pa is an empty-chamber performance reference. Actual operating pressure depends on product load, vapor generation, condenser temperature, pump condition, chamber sealing, valve configuration, and the selected recipe. This distinction is important when establishing process expectations. A properly designed freeze dryer should not only reach a low pressure in an empty chamber; it should maintain a controlled and stable pressure under realistic production or development loads.
Temperature uniformity is one of the most important performance characteristics in a freeze dryer. If shelves do not remain sufficiently uniform, identical containers may experience different freezing and drying conditions. These variations can produce differences in cake appearance, residual moisture, reconstitution behavior, potency, and cycle duration.
The BLK-FD-2 uses a bidirectional silicone-oil circulation heating system. The circulation medium transfers thermal energy across the shelves, allowing the system to provide both cooling and heating through a controlled fluid circuit. Bidirectional circulation helps reduce temperature gradients associated with single-direction flow. The stated inter-shelf temperature deviation is controlled within ±0.5°C, supporting more consistent conditions across the shelf stack.
Silicone oil is widely used in temperature-control systems because it can operate over a broad temperature range and provide stable heat transfer. In a freeze-dryer application, the same circulation concept can support rapid transition from freezing to primary drying and then to secondary drying. This reduces the need for separate thermal systems and simplifies recipe management.
For pharmaceutical development, shelf uniformity is particularly valuable when comparing formulations or optimizing cycle parameters. Researchers can attribute observed product differences more confidently to formulation or process changes rather than uncontrolled equipment variability. In scale-up studies, uniform shelf behavior also helps establish a more defensible relationship between laboratory data and larger production equipment.
The thermal system is complemented by controlled vacuum operation. During primary drying, pressure and shelf temperature must be coordinated so that the product remains below its critical temperature. A stable thermal and vacuum environment helps prevent collapse, melt-back, excessive drying time, and product damage. The BLK-FD-2 is therefore not simply a low-temperature dryer; it is a process platform intended to support controlled heat and mass transfer.
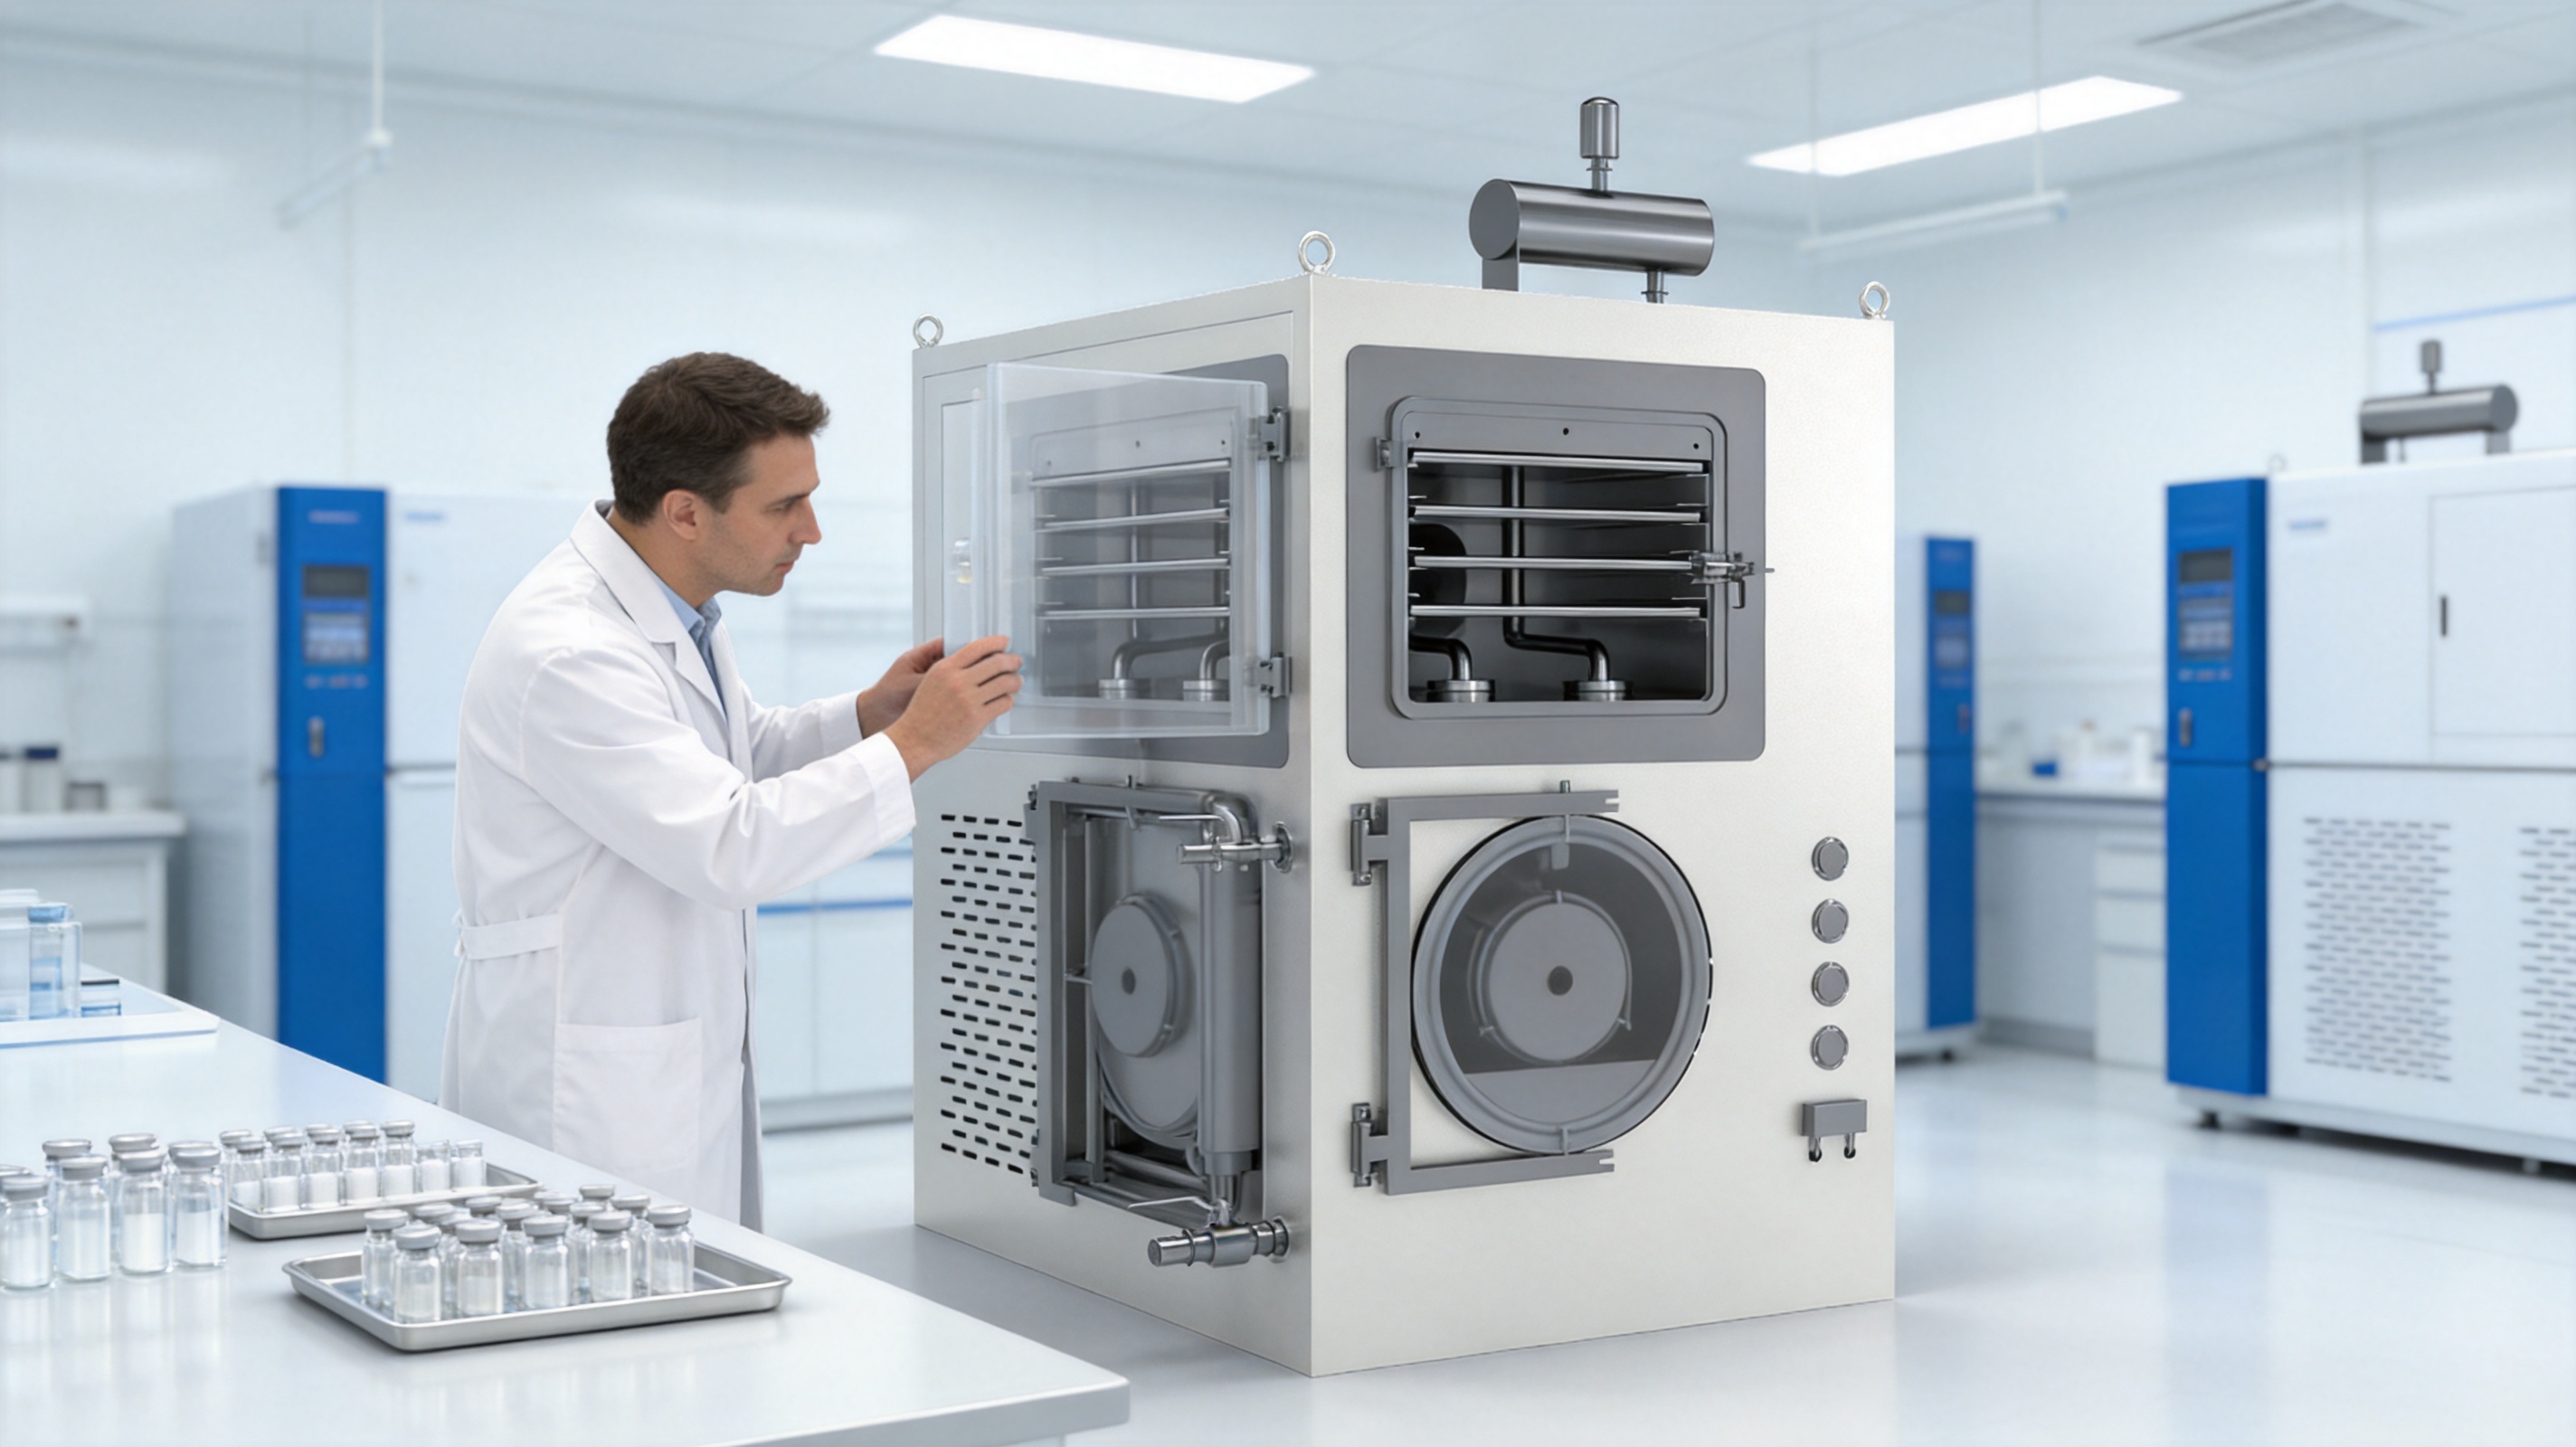
The condenser, or cold trap, is a central component of any vacuum freeze dryer. It receives water vapor sublimated from the product and converts that vapor into ice on a low-temperature surface. The condenser must have sufficient surface area, refrigeration capacity, and thermal performance to capture vapor efficiently throughout the cycle.
The BLK-FD-2 incorporates a patented cold-trap design with a stated 100% improvement in water-capture efficiency. This performance claim refers to the design’s ability to enhance water-vapor capture compared with the relevant conventional configuration or baseline. In practical terms, improved capture can help maintain a more stable chamber environment during high-load primary drying.
A capable cold trap offers several advantages. First, it reduces the risk that vapor will migrate toward the vacuum pump. Second, it supports more stable pressure control when the product releases large amounts of moisture. Third, it can reduce the possibility of fractionation or uneven drying caused by inadequate condenser performance. Fourth, it may contribute to shorter or more predictable cycles by maintaining a stronger driving force for sublimation.
The system’s refrigeration panel can reach a minimum temperature of -70°C. This provides the low-temperature surface required for condensing water vapor under vacuum. The cooling capacity is matched to the development-scale chamber and its intended loading range. A correctly matched condenser is especially important when testing high-solid formulations, deep fills, biological materials, or products with high initial water content.
Compared with basic laboratory freeze dryers that may be optimized for very small batches, a larger development system must manage a substantially higher vapor load. The BLK-FD-2 is designed with this requirement in mind. Its condenser and vacuum architecture are intended to support development work that more closely resembles pilot-scale conditions.
Freeze-drying equipment can be arranged in several ways. Some systems perform freezing and drying in a single chamber. Others use a separate pre-freezing unit, cold room, or dedicated freezer before the product is transferred to the drying chamber. Each arrangement has advantages depending on the product, container, process, and facility layout.
The BLK-FD-2 is available with integrated or separate pre-freezing and drying configurations. This flexibility allows users to select a configuration that reflects their process-development objectives. An integrated configuration can simplify operation by reducing product handling between freezing and drying. It can also reduce exposure to ambient conditions and help maintain a continuous controlled process.
A separate pre-freezing configuration may be advantageous when the development program requires specialized freezing profiles, high throughput in the freezing stage, or independent optimization of freezing and drying. It can also help organizations simulate an existing production process in which product freezing occurs in a separate area. By offering both approaches, the equipment can support different facility designs and process philosophies.
The ability to simulate industrial production processes is a significant advantage over highly limited benchtop equipment. Researchers can investigate loading patterns, freezing rates, shelf temperatures, transfer procedures, and product-handling risks in a system that has more representative capacity. This is useful when preparing for technology transfer, process validation, or the design of a future production line.
Configuration flexibility also supports contract development and manufacturing organizations. CDMOs frequently work with different product types and customer requirements. A system that can accommodate multiple process layouts allows the organization to serve a broader range of projects without purchasing a separate machine for every application.
Equipment used for pharmaceutical and bioprocessing development must be designed with cleaning, contamination control, material compatibility, and inspection in mind. The BLK-FD-2 is described as aligning with GMP principles in key areas of construction and connection design.
Product-contact surfaces use high-grade 316 stainless steel. This material is widely used in hygienic processing equipment because of its corrosion resistance, durability, and suitability for contact with many pharmaceutical and biological formulations. The stated surface roughness is Ra ≤0.4 micrometers, which provides a smooth finish intended to reduce the retention of product residues and facilitate cleaning.
Hygienic-grade connection methods, including quick-release clamp connections, are used to avoid hard-to-clean structures such as exposed threads in product-contact areas. Smooth, accessible connections can reduce dead spaces and simplify inspection. They may also support faster changeover between development batches, which is valuable in laboratories and multi-product facilities.
Sealing materials are selected to meet applicable FDA requirements. Proper seal selection is essential because seals may be exposed to low temperatures, elevated temperatures, vacuum, cleaning agents, and repeated thermal cycling. A suitable sealing system helps protect product integrity and supports stable vacuum performance.
These features do not replace the need for site-specific qualification, cleaning validation, sterilization assessment, or regulatory review. However, they provide a stronger starting point than equipment designed only for general industrial drying. For organizations developing aseptic products, vaccines, injectables, cell-based materials, or biologics, hygienic construction can reduce future adaptation work and support a more efficient transition toward compliant production.
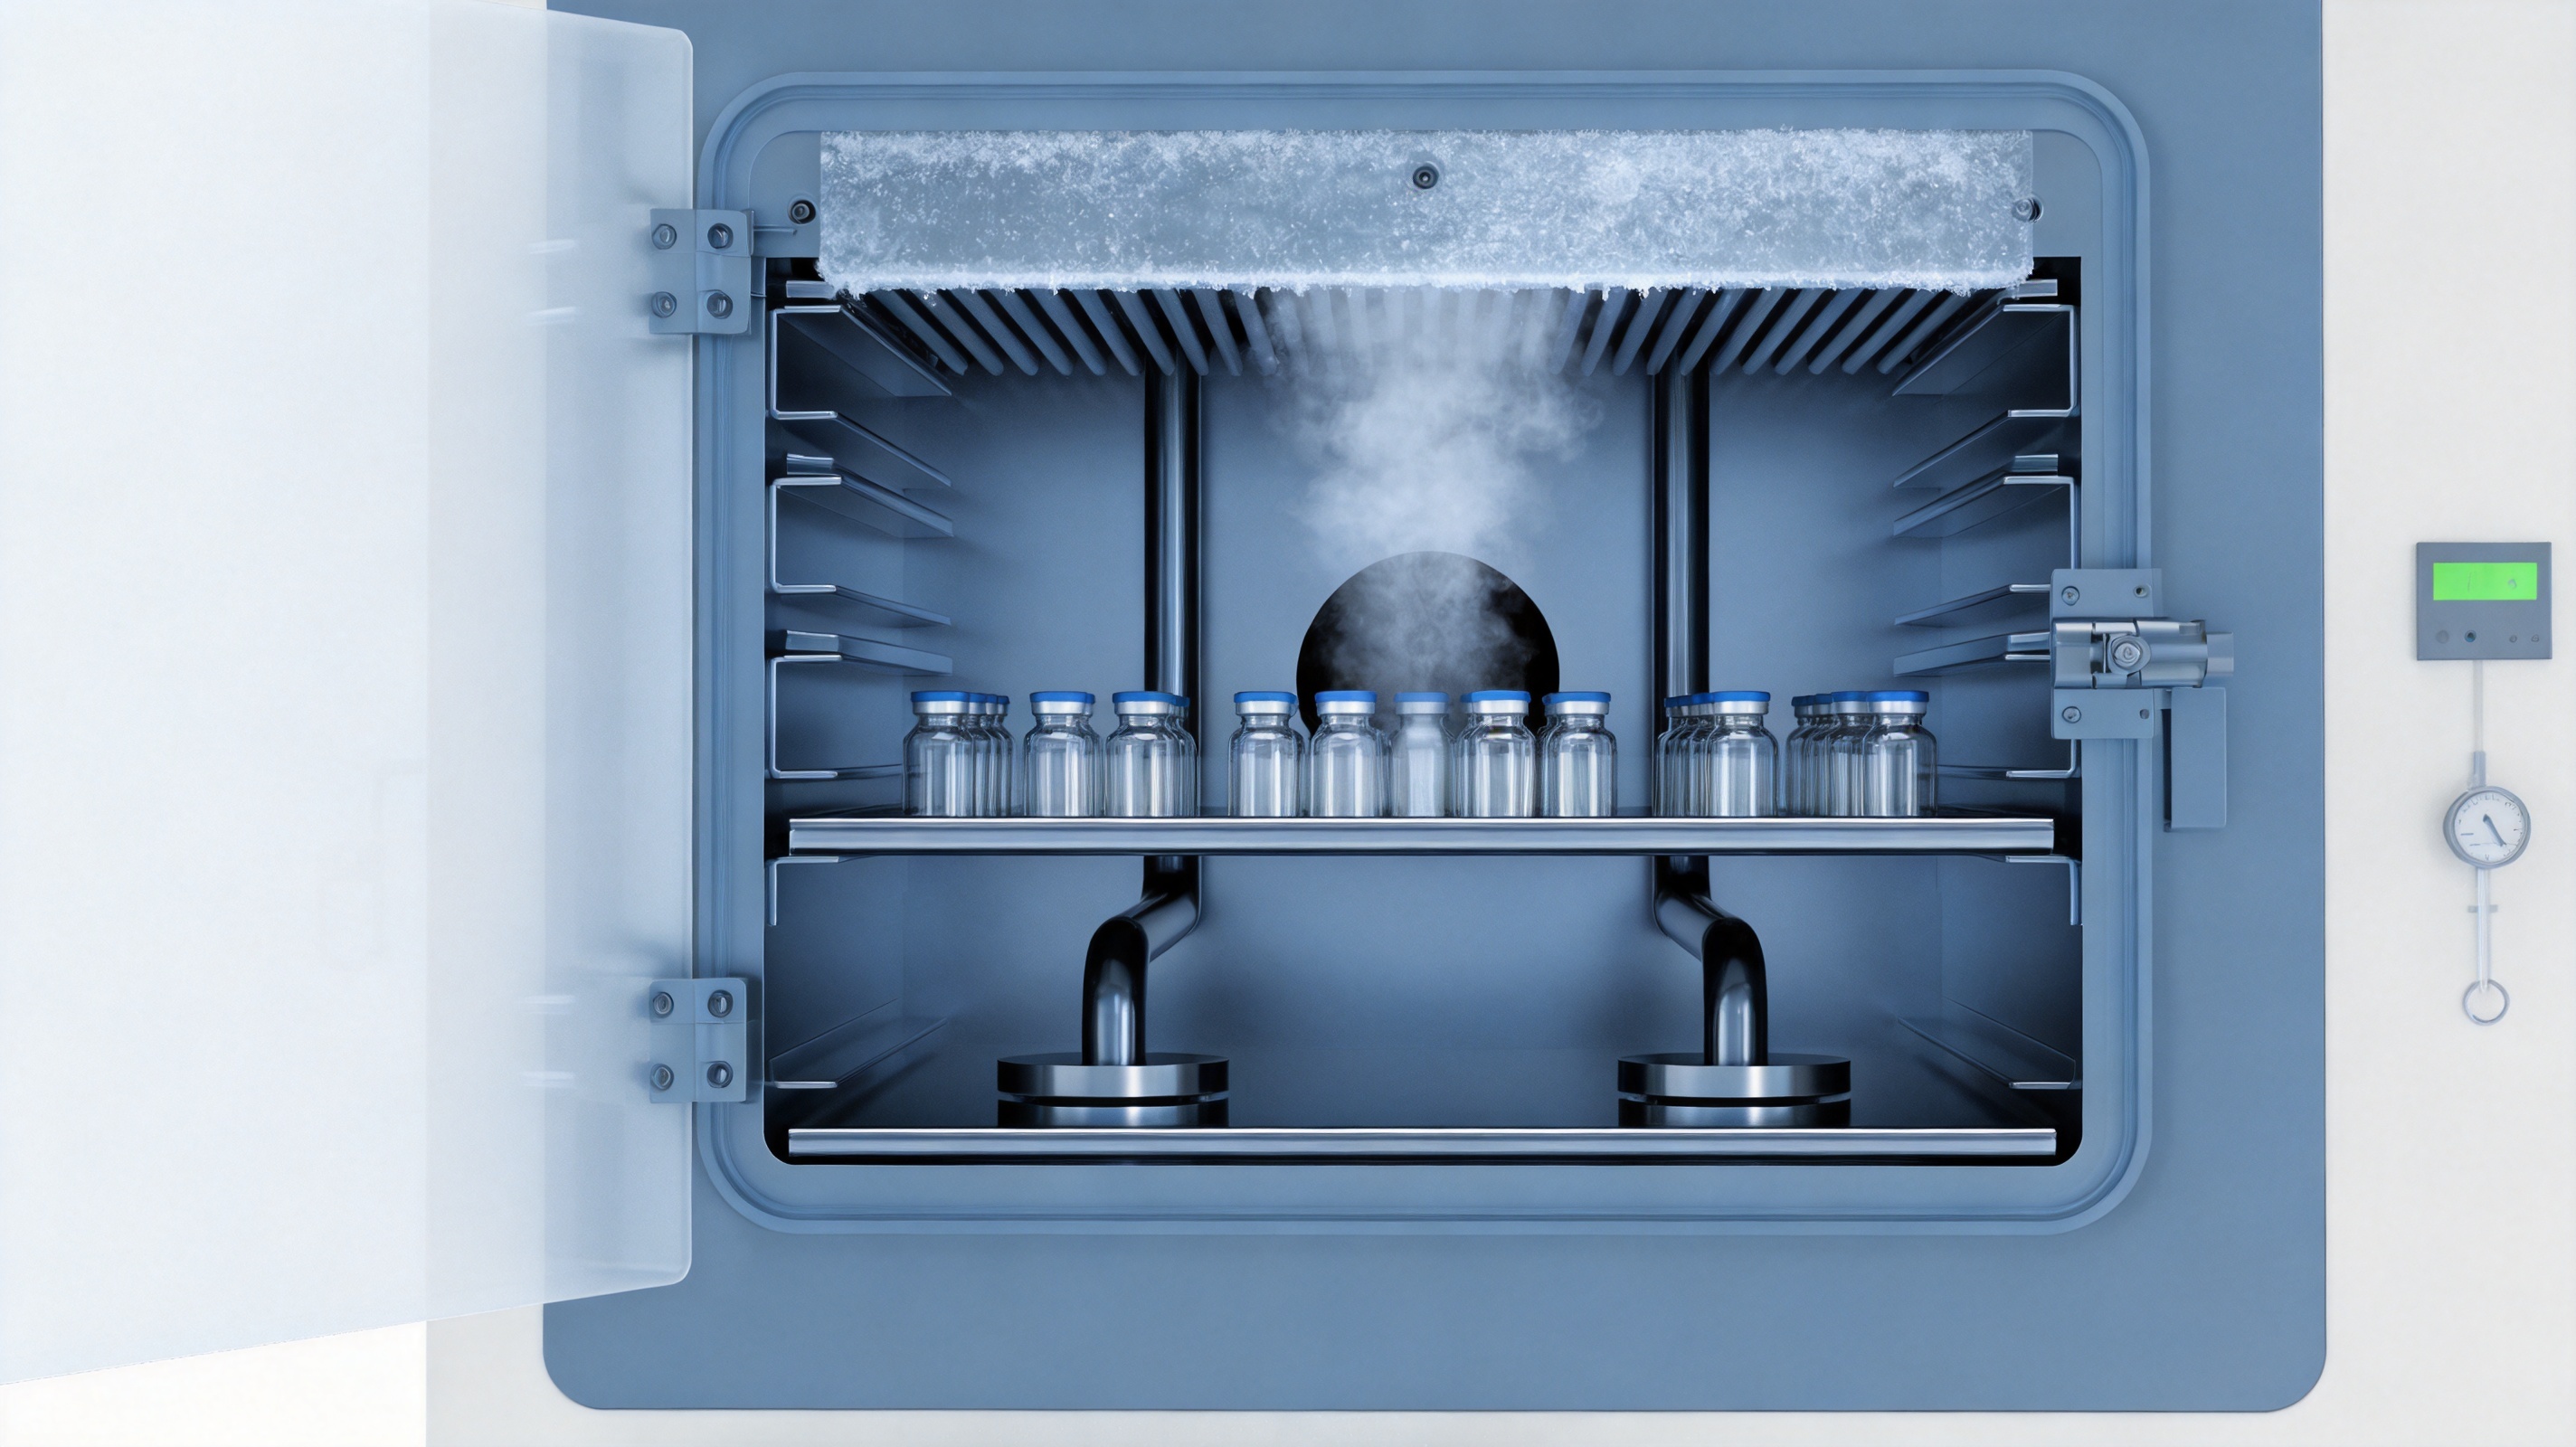
The BLK-FD-2 is suitable for formulation screening and freeze-drying cycle development for a broad range of pharmaceutical products. Potential applications include vaccines, monoclonal antibodies, enzymes, hormones, gene-therapy-related materials, and other protein-based drugs. These products often require carefully controlled thermal exposure because their biological activity can be affected by freezing, dehydration, oxidation, aggregation, or excessive residual moisture.
During development, researchers can use the system to evaluate excipient combinations, formulation concentration, fill volume, container type, freezing profile, primary-drying pressure, shelf-temperature ramps, and secondary-drying conditions. The 2 square meter shelf area allows the team to observe whether the process remains uniform across a larger batch rather than relying only on a few laboratory containers.
For injectable formulations, the system can support research involving lipid bodies, nanoparticles, microspheres, antibiotics, toxic drugs, and other sensitive preparations. Freeze-drying may improve storage stability and simplify distribution when a liquid formulation cannot maintain the required quality over time. The equipment’s controlled temperature and vacuum environment provide a platform for studying the relationship between process conditions and final product performance.
Biological sample preservation is another important area. Researchers may investigate long-term preservation strategies for stem cells, bacterial strains, viral vectors, tissue-engineering materials, bone-derived materials, skin matrices, and other biological samples. Each material has unique requirements, so the ability to adjust freezing and drying conditions is essential.
Freeze-drying can also be used in diagnostic research, laboratory reagents, reference materials, and specialized chemical products. In these applications, the goals may include improving transport stability, extending shelf life, enabling room-temperature handling, or maintaining a precisely controlled solid-state structure.
Although the BLK-FD-2 is strongly suited to pharmaceutical and biochemical research, its capabilities also support food and nutraceutical development. Freeze-drying is used for fruits, vegetables, herbs, coffee ingredients, probiotic materials, functional foods, nutritional supplements, and high-value specialty products.
For food products, the process can preserve shape, color, aroma, flavor, and porous structure more effectively than many conventional drying methods. Removing water at low temperature helps reduce thermal damage. The resulting dry product can often be rehydrated quickly, making it useful for premium foods, emergency nutrition, ingredients, and convenience products.
Nutraceutical manufacturers can use the equipment to evaluate botanical extracts, vitamins, enzymes, probiotics, and other heat-sensitive ingredients. Process development can focus on residual moisture, flowability, reconstitution, active-ingredient retention, and storage stability. The development-scale capacity helps bridge the gap between laboratory formulation work and commercial batch planning.
Specialty chemical materials may also benefit from freeze-drying when porosity, particle structure, low bulk density, or low-temperature processing is required. The ability to control shelf temperature, chamber pressure, and condenser conditions provides a versatile platform for investigating materials that are unsuitable for spray drying, tray drying, or conventional evaporation.
Energy consumption is a major consideration in freeze-drying because the process involves refrigeration, vacuum generation, shelf-temperature control, and long operating cycles. Energy efficiency affects operating cost, equipment utilization, facility design, and environmental performance.
The equipment platform developed by Bolaike incorporates an integrated energy-efficient structure. Instead of relying on completely duplicated refrigeration systems for cold storage and freeze-drying functions, the integrated design enables shared refrigeration circuits for cooling and drying processes. Sharing major refrigeration resources can reduce system losses, simplify the equipment architecture, and improve overall utilization of the refrigeration system.
The manufacturer reports energy-consumption reductions of approximately 20% to 40% under relevant operating conditions and a potential reduction in single-batch cycle time of approximately 15% to 25%. Actual savings depend on product load, cycle recipe, ambient conditions, condenser operation, compressor loading, and comparison baseline. Nevertheless, the design direction is important: efficient refrigeration and vapor management can reduce both direct utility consumption and the indirect cost of long cycle times.
A related cold-energy recovery system is designed to reuse residual cold energy from refrigeration media. In a conventional arrangement, cold energy may be used once and then discharged, forcing compressors to work harder during the next cycle. By pre-cooling the next cycle’s refrigeration media with residual cold energy, the system can reduce compressor load. The manufacturer reports potential compressor-load reductions of approximately 20% to 30% for this function.
Energy-saving technologies are valuable in research facilities as well as production plants. A development laboratory may operate many small or medium batches each month, and the cumulative utility demand can become significant. Reduced cycle time also improves equipment availability, allowing more experiments or batches to be completed without expanding the installed equipment base.
Modern freeze-drying development requires more than manual adjustment of temperature and vacuum. Researchers need repeatable recipes, recorded process parameters, alarm management, and the ability to monitor equipment status. The BLK-FD-2 can be integrated with an intelligent central control system that manages the operational status of connected equipment.
A centralized system can coordinate refrigeration, shelf-temperature circulation, vacuum generation, valves, defrosting, and other operating functions. This reduces the need for operators to manage each subsystem independently. It also supports more consistent execution of validated or approved recipes.
Remote monitoring through a mobile application is available as an optional or configurable function. Remote access can help maintenance teams observe equipment status, review alarms, and respond to abnormal conditions more quickly. It is especially useful when the freeze dryer operates in a controlled facility where responsible personnel may not remain beside the equipment throughout a long cycle.
Multiple language options can be customized to accommodate international users and multinational organizations. The operation screen can also be positioned on the front or side according to facility requirements. This seemingly simple design option can improve operator ergonomics, visibility, and integration with room layouts.
For development laboratories, data management is just as important as physical control. Users should establish procedures for recording batch information, shelf temperature, product temperature, chamber pressure, condenser temperature, cycle events, alarms, and deviations. A properly configured control and data system can strengthen development reports and support technology-transfer packages.
The BLK-FD-2 has several characteristics that distinguish it from basic laboratory freeze dryers and from conventional development systems. Its principal advantage is balance. It offers a larger and more industrially representative processing area than a small benchtop machine while remaining compact enough for research, pilot, and small-batch environments.
Many entry-level laboratory freeze dryers are designed primarily for simple sample preservation. They may have limited shelf area, less sophisticated thermal circulation, smaller condensers, and fewer options for simulating production procedures. Such equipment can be useful for early feasibility work but may not reveal the heat-transfer and vapor-load challenges that emerge during scale-up.
At the other end of the market, large production lyophilizers may provide excellent capacity but require substantial space, utilities, capital investment, and qualification resources. They are not always suitable for fast formulation screening or frequent recipe changes. The BLK-FD-2 provides an intermediate alternative that can generate more realistic process information without immediately committing to a full production line.
Compared with systems that use a simple one-direction heating circuit, the BLK-FD-2’s bidirectional silicone-oil circulation is intended to improve shelf uniformity. Compared with systems that rely on a basic condenser, its patented cold-trap structure is designed to enhance water capture. Compared with equipment that separates all refrigeration functions, its integrated energy-saving architecture is intended to reduce duplication and operating losses.
The equipment also offers advantages in process flexibility. Integrated or separate pre-freezing configurations allow the user to select a layout that reflects the target process. Hygienic materials and connections provide a better foundation for pharmaceutical and biological applications than general-purpose drying equipment. Optional mobility, including a swivel-caster design, makes the unit easier to reposition within a laboratory or pilot area.
These advantages should be evaluated through site acceptance testing, performance qualification, product-specific trials, and a comparison with the user’s own baseline equipment. No freeze dryer is universally superior for every formulation. The strongest selection is the one that matches the product’s thermal sensitivity, batch size, container format, facility utilities, compliance expectations, and future production pathway.
The performance of a freeze dryer depends on the quality of its design, fabrication, assembly, testing, and service support. Bolaike operates as a specialized refrigeration and vacuum freeze-drying equipment manufacturer with capabilities covering research and development, engineering, sales, installation, commissioning, and after-sales service.
The company traces its refrigeration experience to 2003 and was established as Jiangsu BoLaiKe Refrigeration Science and Technology Development Co., Ltd. in 2014. Its product development activities focus on vacuum freeze-drying and refrigeration equipment for food, pharmaceutical, biological, chemical, and related industries.
An integrated engineering team can provide advantages over fragmented procurement arrangements. When refrigeration design, vacuum systems, shelf circulation, controls, chamber fabrication, installation, and commissioning are coordinated by one organization, interface risks may be reduced. This can simplify technical communication and make it easier to resolve performance issues during commissioning.
Bolaike has developed partnerships with universities and research institutions, including agricultural and engineering research organizations. Such cooperation can support application-oriented development and provide insight into the practical needs of research laboratories, pilot plants, and production facilities.
The company reports more than 100 national invention and utility model patents. Its portfolio includes technologies related to energy efficiency, refrigeration integration, cold-energy recovery, condenser design, and freeze-drying equipment. Patents alone do not guarantee suitability for a particular process, but they indicate a continued investment in equipment innovation.
The manufacturer also reports export experience in more than 30 countries and regions. International project experience can be valuable when equipment must be adapted to different electrical standards, facility layouts, documentation requirements, operating languages, and service expectations.
The company has moved into a modern manufacturing base covering approximately 24,000 square meters. A dedicated manufacturing facility can support more controlled fabrication, assembly, inspection, and testing than a small workshop. For customers purchasing development equipment, manufacturing infrastructure is important because it affects delivery consistency, spare-parts support, customization capability, and long-term service.
Before installing the BLK-FD-2, users should confirm room dimensions, floor loading, door access, electrical supply, ventilation, drainage, vacuum-pump requirements, cooling conditions, and service clearances. The stated equipment dimensions are approximately 1,800 millimeters in length, 1,000 millimeters in width, and 2,000 millimeters in height. Additional clearance may be required for maintenance, loading, unloading, and connection of utilities.
The installation area should be clean, stable, and suitable for the intended product category. Pharmaceutical and biological applications may require classified areas, controlled environmental conditions, or special material-transfer procedures. The room design should consider heat released by refrigeration equipment, noise, operator movement, and access for service personnel.
Commissioning typically includes inspection of mechanical connections, electrical systems, refrigeration circuits, vacuum performance, shelf-temperature behavior, condenser temperature, control functions, alarm functions, and safety interlocks. Users should agree with the supplier on factory-acceptance testing and site-acceptance testing criteria before delivery.
For regulated applications, qualification may include design qualification, installation qualification, operational qualification, and performance qualification. The specific documentation package depends on the intended use, local regulations, internal quality systems, and product risk assessment. Equipment features such as hygienic construction and control records can support qualification, but the customer remains responsible for defining and executing the applicable validation strategy.
Routine maintenance should include inspection of seals, vacuum lines, valves, refrigeration components, pumps, sensors, oil-circulation components, and control-system alarms. Condenser defrosting and cleaning should be performed according to the product and facility procedures. Preventive maintenance is particularly important because gradual loss of vacuum performance or refrigeration capacity may not be obvious until it affects a batch.
A structured process-development program can make effective use of the equipment. The first step is to characterize the formulation, including solids content, freezing behavior, glass-transition or collapse temperature, eutectic behavior, viscosity, fill volume, container geometry, and target residual moisture.
The next step is to define the freezing strategy. Researchers may compare controlled cooling rates, shelf-temperature ramps, nucleation approaches, hold times, and final freezing temperatures. The objective is to obtain a frozen structure that supports efficient sublimation while protecting the product’s critical attributes.
Primary drying development should identify a safe operating region for shelf temperature and chamber pressure. The product temperature should remain below its critical limit while the process maintains an acceptable sublimation rate. Thermocouples, pressure measurements, comparative pressure methods, endpoint indicators, and product inspection can all contribute to the assessment.
Secondary drying can then be optimized to achieve the target residual-moisture range without unnecessary thermal exposure. A higher secondary-drying temperature may shorten the cycle but could affect product stability. A lower temperature may better protect the product but increase operating time. The BLK-FD-2’s shelf-temperature range provides flexibility for exploring this balance.
After the cycle is established, users should conduct repeatability studies. Multiple runs can help determine the effects of batch loading, shelf position, fill-volume variation, and normal equipment variability. The resulting data can support scale-up calculations and define appropriate process-control limits.
Purchasing a development-scale freeze dryer is not only an equipment decision; it is a process-development investment. Organizations that rely entirely on small laboratory units may face uncertainty when transferring a cycle to production. Organizations that outsource every experiment may lose time, flexibility, and control over proprietary formulations.
The BLK-FD-2 can help internal teams perform more work in-house. Pharmaceutical companies can screen formulations and establish cycles before engaging a production site. CDMOs can use the unit to support customer development projects. Universities and national laboratories can conduct applied research at a scale more relevant to industrial adoption. Food and nutraceutical manufacturers can develop premium products without immediately installing a commercial production line.
Using equipment with production-oriented design features during the research phase may reduce scale-up risks. Hygienic materials, representative shelf behavior, larger vapor loads, integrated controls, and flexible freezing configurations can help ensure that development knowledge remains relevant when the process moves to a larger system.
The equipment may also offer long-term value because it can serve multiple functions. A single unit can support formulation development, process optimization, pilot production, sample preservation, customer trials, and small-batch manufacturing. Optional mobility and configurable control features further extend its usefulness as the laboratory changes.
Before ordering a BLK-FD-2, customers should review the product and facility requirements in detail. Important questions include the desired batch size, product type, container format, target cycle time, freezing method, required level of automation, control-system language, documentation package, and applicable regulatory standards.
Customers should also clarify whether they need integrated or separate pre-freezing, whether the machine will be used for aseptic or non-aseptic products, whether steam sterilization or another sanitization method is required, and whether remote monitoring is necessary. The supplier should confirm the exact configuration, included instruments, vacuum-pump arrangement, refrigeration performance, control functions, and acceptance-test conditions.
For products with high water content or unusually high vapor release, condenser performance should be evaluated under representative loads rather than only under empty-chamber conditions. For sensitive biologics, users should request process trials or sample testing when possible. For facilities with limited utilities, installed power, cooling requirements, ventilation, and service access should be reviewed at an early stage.
Customers should also consider the future production pathway. If the long-term goal is a GMP pharmaceutical manufacturing process, it is beneficial to select development equipment with hygienic design, data-recording capability, and process behavior that can be correlated with larger systems. If the primary goal is food or nutraceutical production, loading flexibility, throughput, cleaning access, and operating cost may receive greater emphasis.
The 2 square meter freeze-drying area, 20 kilogram typical loading capacity, and 40 liter liquid loading capacity allow users to perform development work at a scale more meaningful than a small benchtop experiment.
The silicone-oil bidirectional circulation system, shelf-temperature range from -55°C to +80°C, inter-shelf deviation within ±0.5°C, and ultimate vacuum specification of less than or equal to 10 Pa support repeatable process development.
The patented cold-trap design and minimum refrigeration-panel temperature of -70°C are intended to improve water capture, maintain vacuum stability, and support demanding high-moisture cycles.
316 stainless-steel product-contact surfaces, Ra ≤0.4 micrometer surface roughness, hygienic connections, FDA-compliant sealing materials, configurable pre-freezing arrangements, energy-saving refrigeration architecture, and intelligent control options provide a strong foundation for pharmaceutical and biochemical applications.
The BLK-FD-2 is an R&D scale vacuum freeze dryer intended for pharmaceutical, biochemical, food, nutraceutical, chemical, and biological sample development. It is designed to bridge the gap between small laboratory freeze dryers and larger industrial production systems.
The freeze-drying area is 2 square meters. This provides enough shelf space for representative development batches and selected pilot-scale or small-batch production work.
The typical loading capacity is 20 kilograms, and the liquid loading capacity is 40 liters. Actual loading depends on product density, fill depth, container type, shelf arrangement, formulation characteristics, and the selected cycle.
Yes. Integrated or separate pre-freezing and drying configurations are available. The appropriate configuration depends on the user’s process, facility layout, product sensitivity, and scale-up strategy.
The shelf-temperature range is -55°C to +80°C. This range supports freezing, primary drying, and secondary drying for a wide variety of formulations.
The stated inter-shelf temperature deviation is controlled within ±0.5°C under the applicable test conditions. Actual uniformity should be verified during commissioning and qualification.
The refrigeration panel can reach a minimum temperature of -70°C. This low temperature supports condensation of water vapor during freeze-drying.
The stated ultimate vacuum is less than or equal to 10 Pa under the specified empty-chamber test condition. Operating pressure under product load depends on the formulation, vapor generation, chamber sealing, pump condition, and cycle parameters.
Yes. Its temperature control, vacuum performance, hygienic materials, 316 stainless-steel product-contact surfaces, smooth finish, and flexible configuration make it suitable for pharmaceutical and biochemical process development. Product-specific qualification and validation remain necessary.
Potential applications include vaccines, monoclonal antibodies, enzymes, hormones, gene-therapy-related materials, protein drugs, lipid bodies, nanoparticles, microspheres, antibiotics, toxic drug preparations, and other injectable or biological products.
Yes. It can support research into preservation of stem cells, bacterial strains, viral vectors, tissue-engineering materials, bone materials, skin matrices, and other biological samples, provided that the process is developed for the specific material.
The equipment platform includes an integrated energy-efficient refrigeration structure and a cold-energy recovery concept. The manufacturer reports potential energy and compressor-load reductions, although actual savings depend on the cycle, load, ambient conditions, and comparison baseline.
Remote monitoring through a mobile application is available as a configurable function. The control system can also support multiple languages and flexible placement of the operation screen.
Customization may be available for configuration, pre-freezing arrangement, control language, screen position, mobility options, and other project requirements. The final specification should be confirmed with the manufacturer before ordering.
The BLK-FD-2 is manufactured by Jiangsu BoLaiKe Refrigeration Science and Technology Development Co., Ltd., a Chinese specialist in vacuum freeze-drying and refrigeration equipment.
Users should check room dimensions, floor loading, electrical supply, ventilation, service clearance, vacuum-pump requirements, cooling conditions, drainage, access routes, and any applicable cleanroom or regulatory requirements.
The BLK-FD-2 is a versatile development-scale vacuum freeze dryer designed for organizations that need more than a basic laboratory machine but do not yet require a full industrial production system. Its 2 square meter freeze-drying area, 20 kilogram typical loading capacity, and 40 liter liquid capacity provide a practical scale for formulation work, process optimization, pilot studies, and selected small-batch operations.
Its main technical strengths include a broad shelf-temperature range, bidirectional silicone-oil circulation, inter-shelf temperature control within ±0.5°C, a minimum refrigeration-panel temperature of -70°C, a stated ultimate vacuum of less than or equal to 10 Pa, and a patented cold-trap design intended to improve water capture. Flexible integrated or separate pre-freezing configurations allow the system to reflect different industrial process models.
For pharmaceutical and biochemical users, hygienic construction is a major benefit. High-grade 316 stainless steel, Ra ≤0.4 micrometer product-contact surfaces, hygienic connections, and FDA-compliant sealing materials provide an equipment foundation aligned with GMP-oriented development practices. Energy-saving refrigeration, cold-energy recovery, intelligent control, remote monitoring, and optional mobility further increase its operational flexibility.
Bolaike’s manufacturing experience, integrated engineering capabilities, patent portfolio, research partnerships, export activity, and dedicated manufacturing base strengthen its ability to deliver customized freeze-drying solutions. The most important value of the BLK-FD-2, however, is its ability to connect laboratory research with future manufacturing. By generating more representative process data at development scale, it can help users reduce scale-up uncertainty, improve cycle robustness, and accelerate the transition from formulation concept to reliable production.
1. United States Pharmacopeia. General principles and guidance related to pharmaceutical freeze-drying and product stability.
2. International Society for Pharmaceutical Engineering. Good practice guidance for pharmaceutical manufacturing equipment and process validation.
3. European Medicines Agency. Guidance on the manufacture and quality control of biological and biotechnological products.
4. Food and Drug Administration. Current good manufacturing practice principles for pharmaceutical production and equipment design.
5. Rey, L., and May, J. C. Freeze-Drying and Cryogenic Processing in Pharmaceutical and Biological Applications.
6. Jennings, T. A. Lyophilization: Introduction and Basic Principles.
7. Technical product information for the BLK-FD-2 R&D scale vacuum freeze dryer.
8. Manufacturer technical materials concerning energy-efficient refrigeration, cold-energy recovery, hygienic equipment design, and vacuum freeze-drying systems.
 2026/05/28
 2026/05/28
2026/05/28


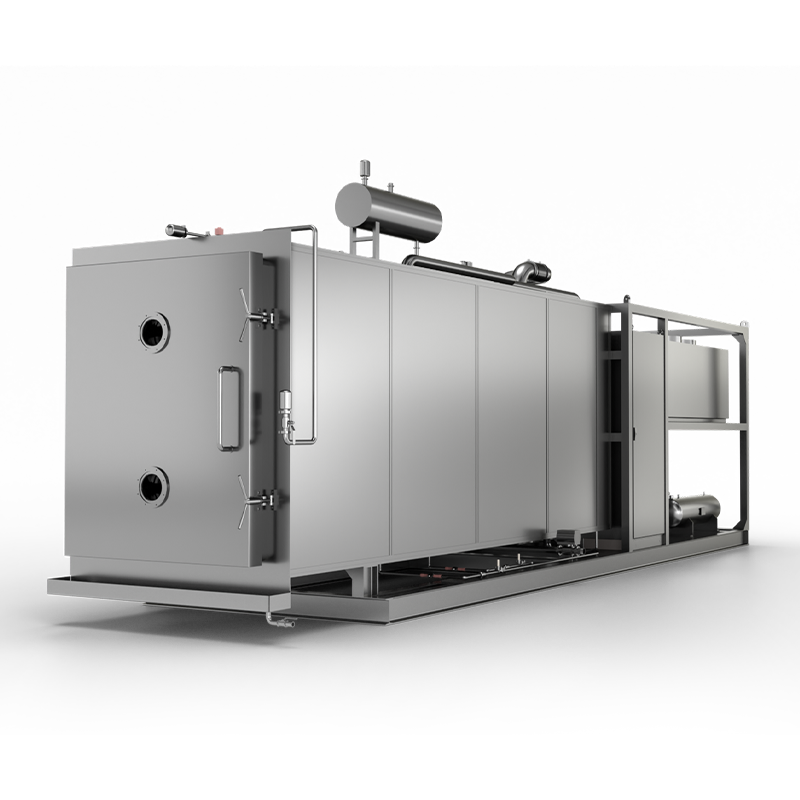
 Custom Industrial Lyophilizer Freeze Dryer Manufacturers


 English
 русский
 Español
 Français
 Deutsch
 عربى