/author/xu-anru-customer-support-and-service-coordinator/

News
Products & Solutions
CONTACT US

+86-18068757376

blk@jsblk.com

No. 29 North Tongjiang Road, Xinbei District, Changzhou City, Jiangsu Province, China
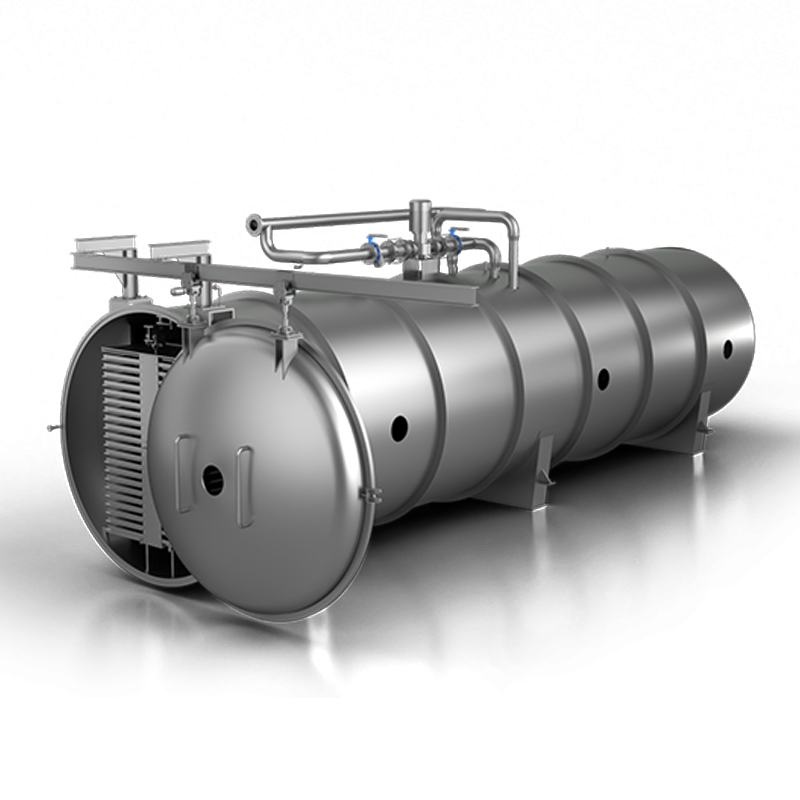
BLK-FD-200
Large-scale freeze-drying requires far more than simply increasing chamber dimensions. As production volumes grow, manufacturers must maintain precise temperature control, stable vacuum conditions, uniform product quality, dependable refrigeration, efficient water-vapor removal, and reliable operation over long production cycles. At the same time, rising energy costs, stricter quality expectations, and the need for flexible production have made equipment selection a strategic decision rather than a routine purchasing exercise.
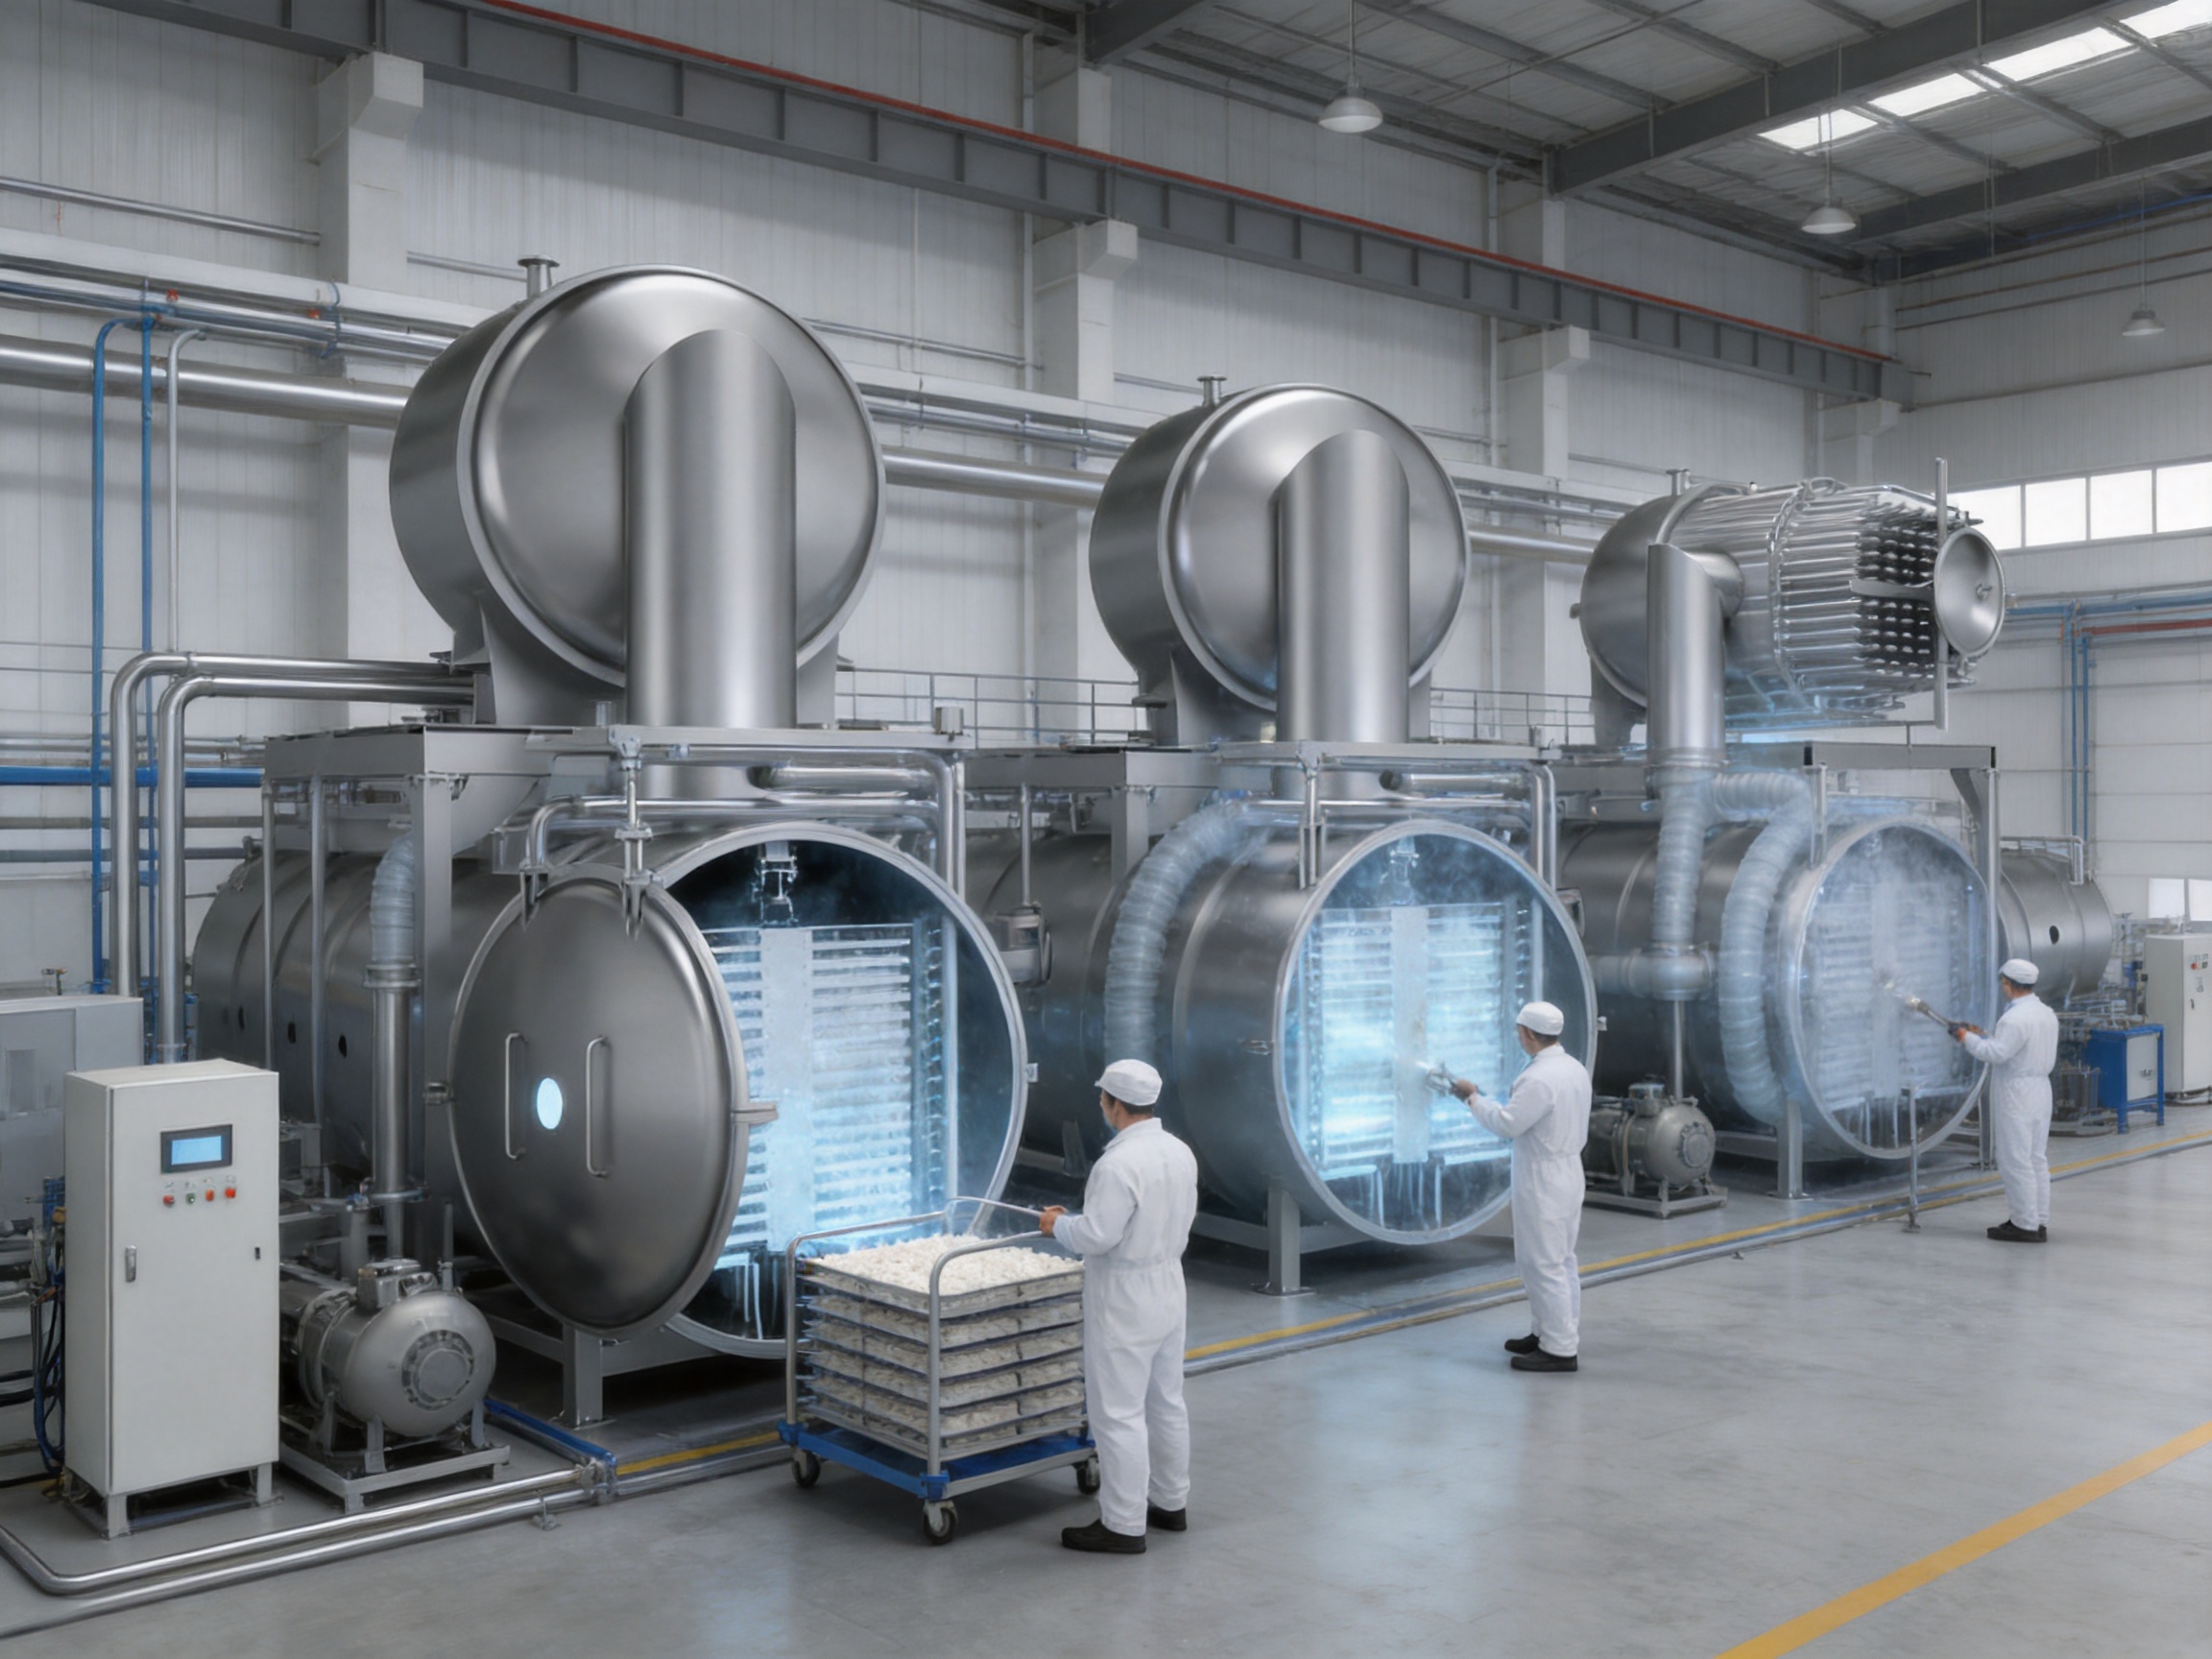
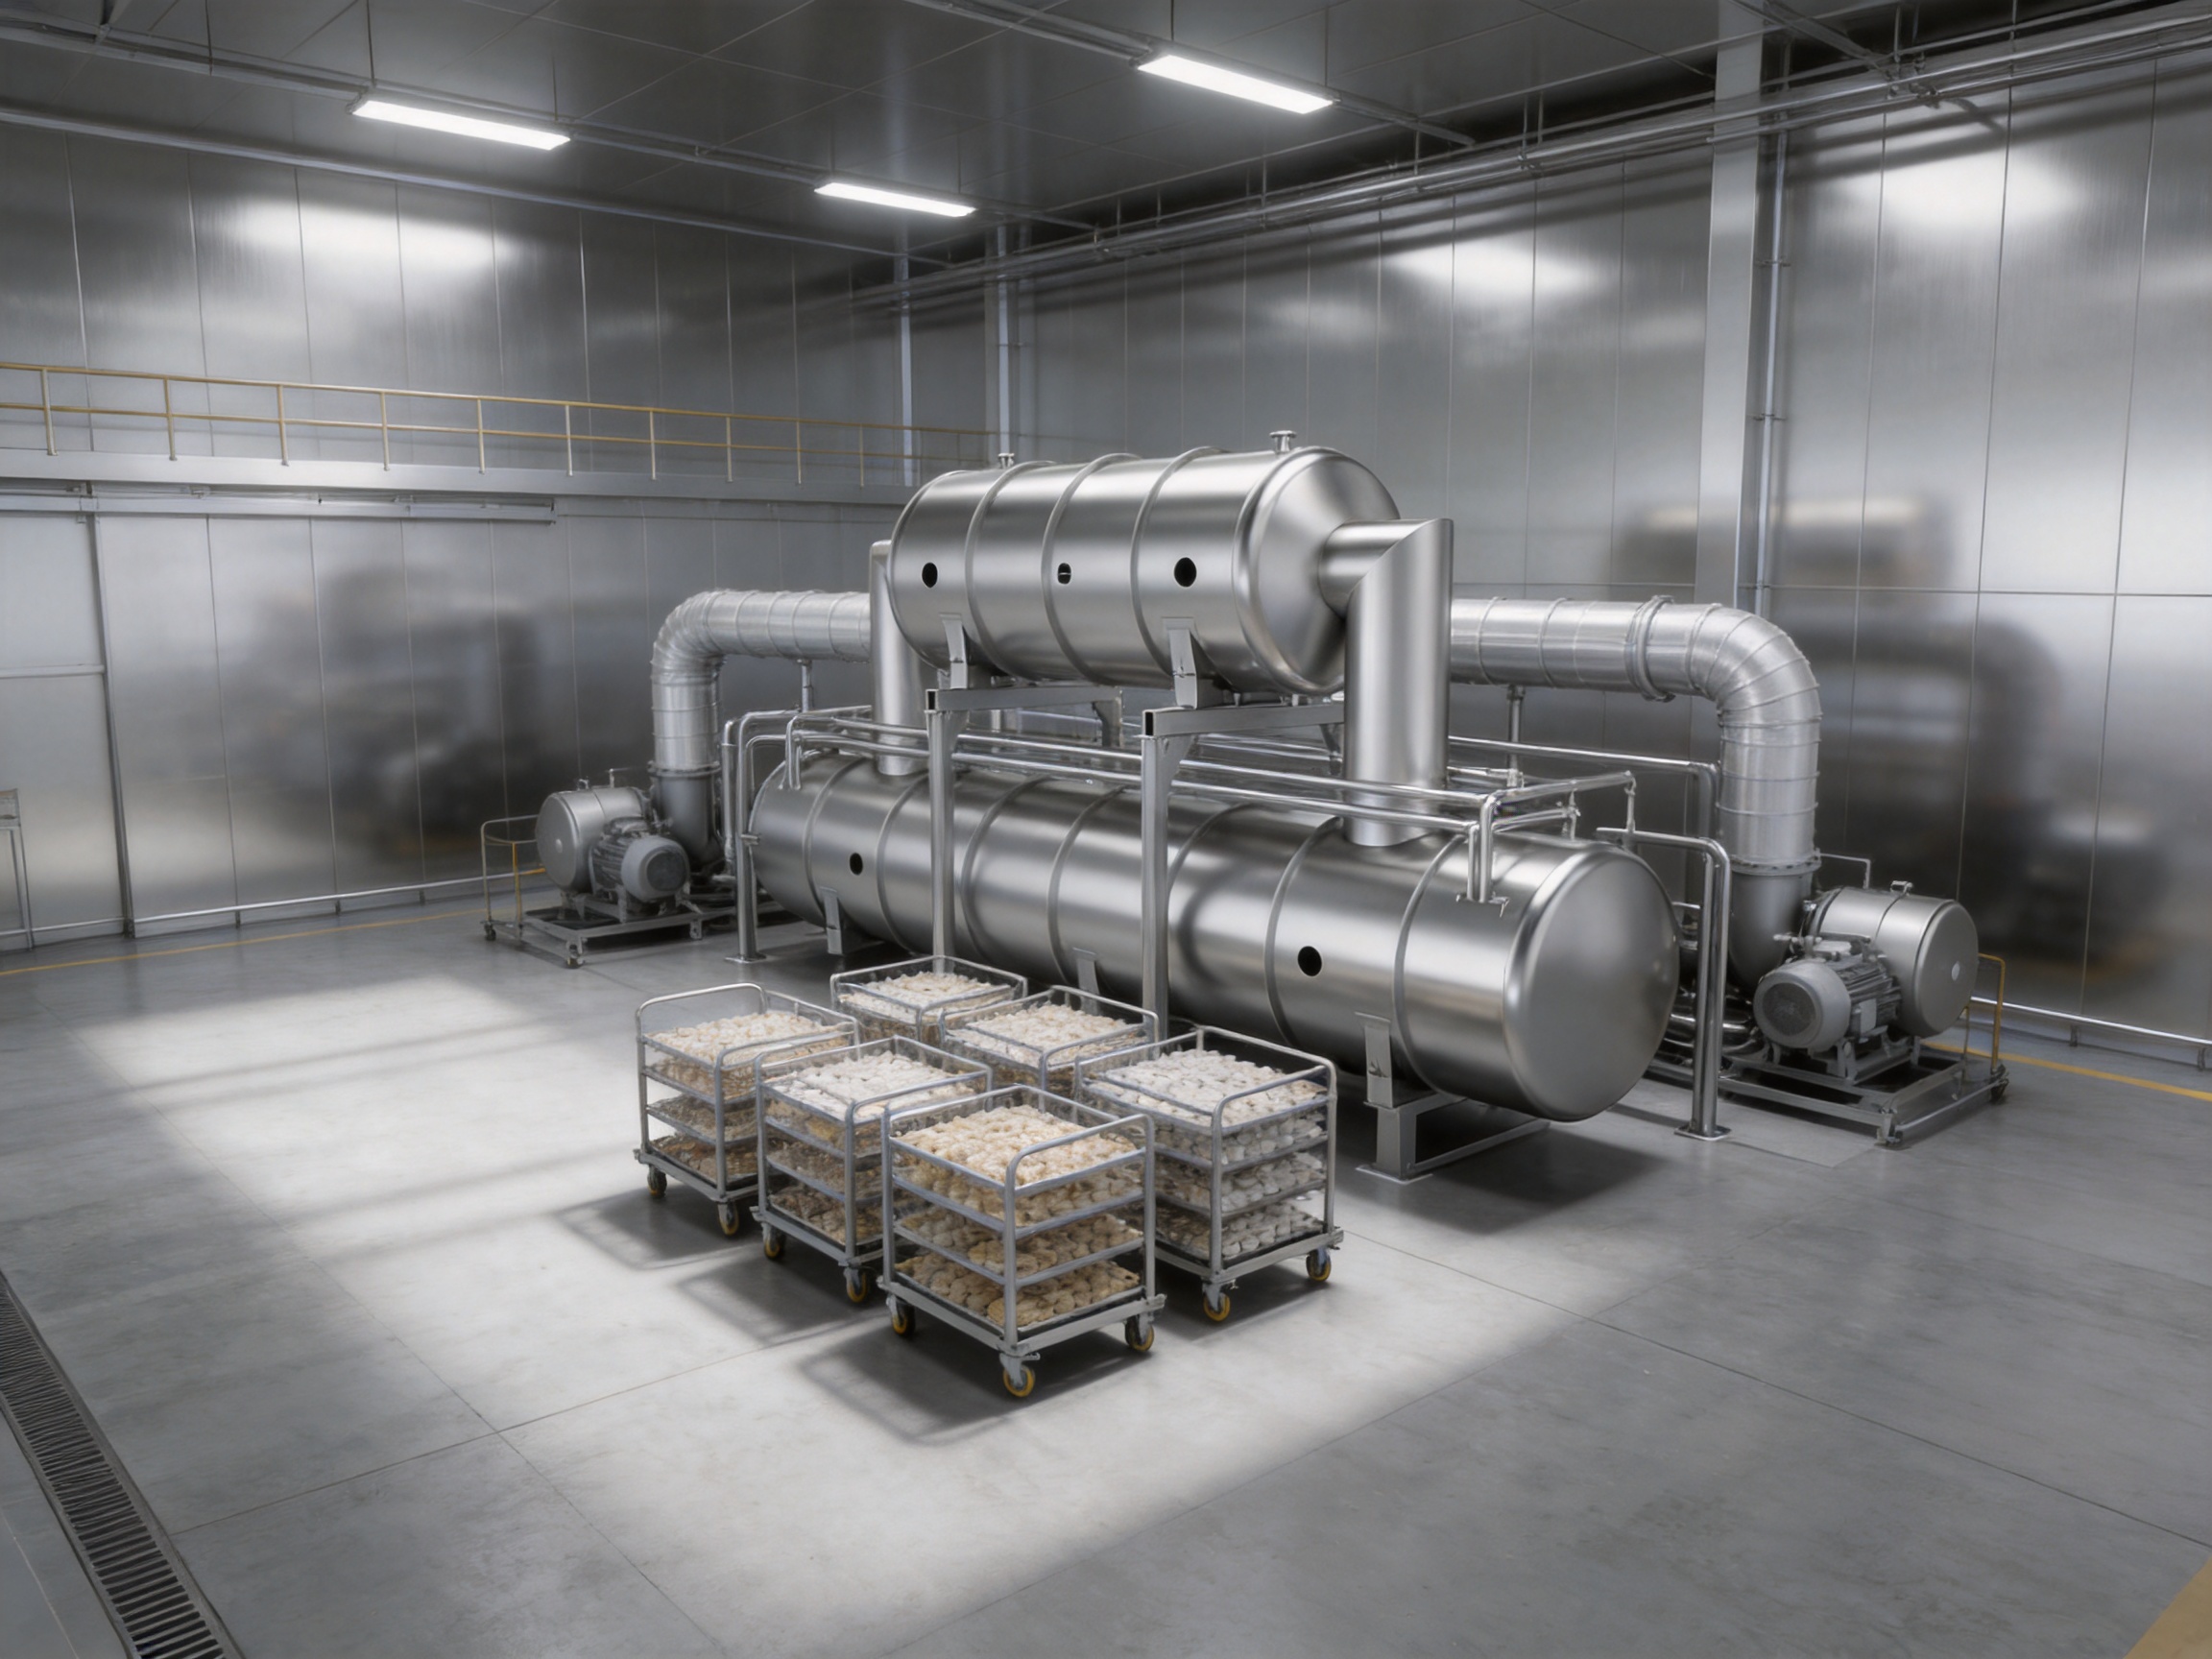
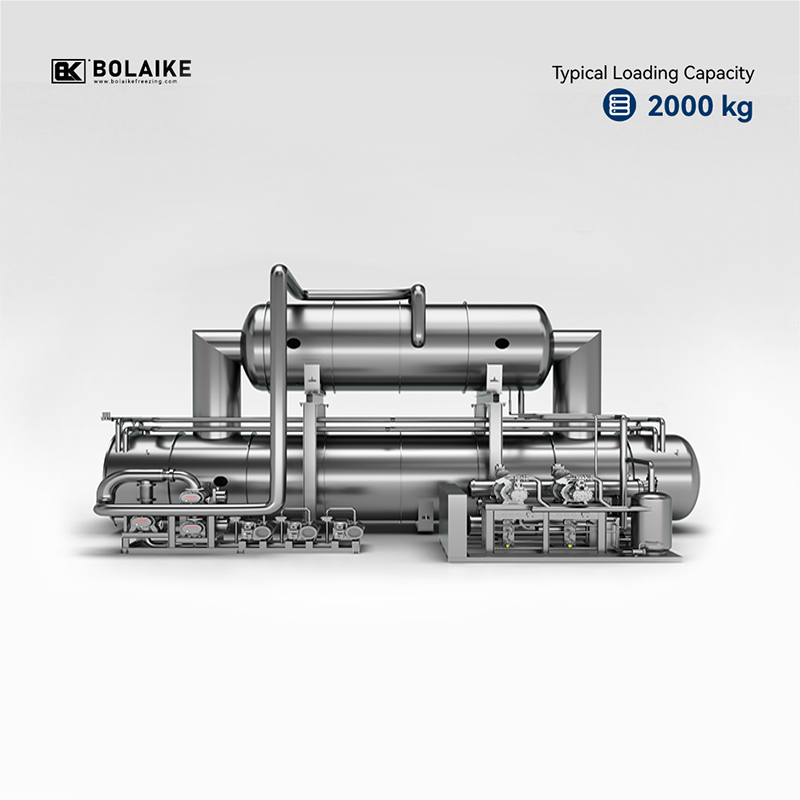
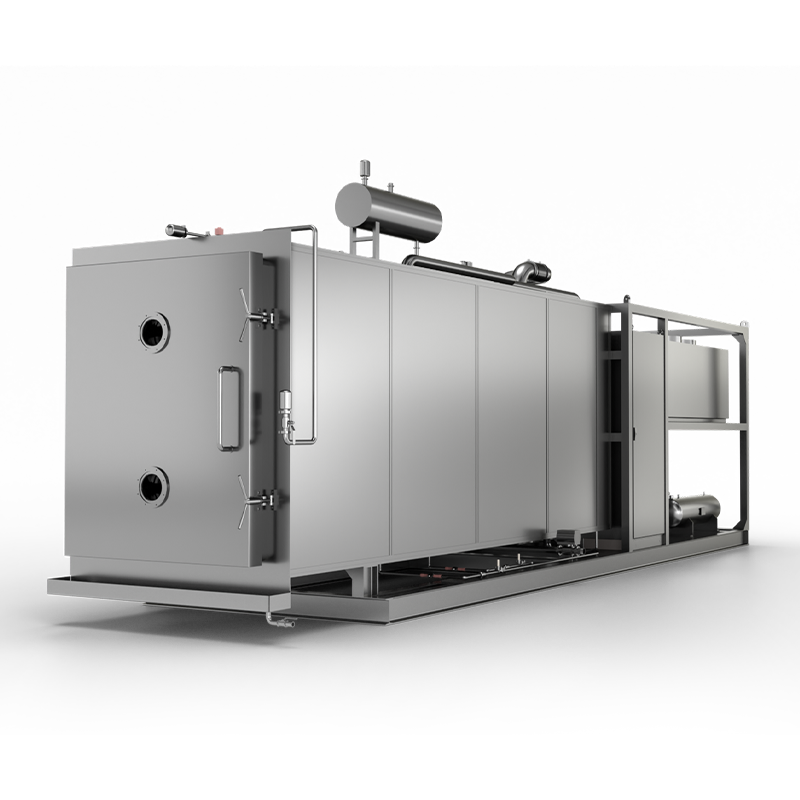
The BLK-FD-200 is a heavy-duty industrial freeze dryer designed for high-capacity processing in food, agricultural products, medicinal materials, health supplements, chemicals, biological supplies, and related industries. With a freeze-drying area of 202.2 square meters, a standard loading capacity of 2,000 kilograms, a liquid loading capacity of 4,000 liters, and an ultimate vacuum level of no more than 10 Pa, the system is engineered for demanding commercial and industrial applications.
Its design combines a cylindrical drying chamber, integrated cold recovery, intelligent control, high-uniformity heating plates, optional intermediate isolation technology, flexible refrigeration configurations, and production-oriented parallel operation. These features enable the equipment to deliver high throughput while helping users reduce energy consumption, shorten batch intervals, and maintain stable product quality.
Beyond its technical specifications, the value of the BLK-FD-200 lies in the manufacturing capabilities behind it. The equipment is produced by Jiangsu Bolaike Freezing Technology Development Co., Ltd., a Chinese high-tech enterprise specializing in vacuum freeze-drying and refrigeration equipment. The company combines research and development, engineering design, manufacturing, installation, commissioning, and after-sales service within one professional organization.
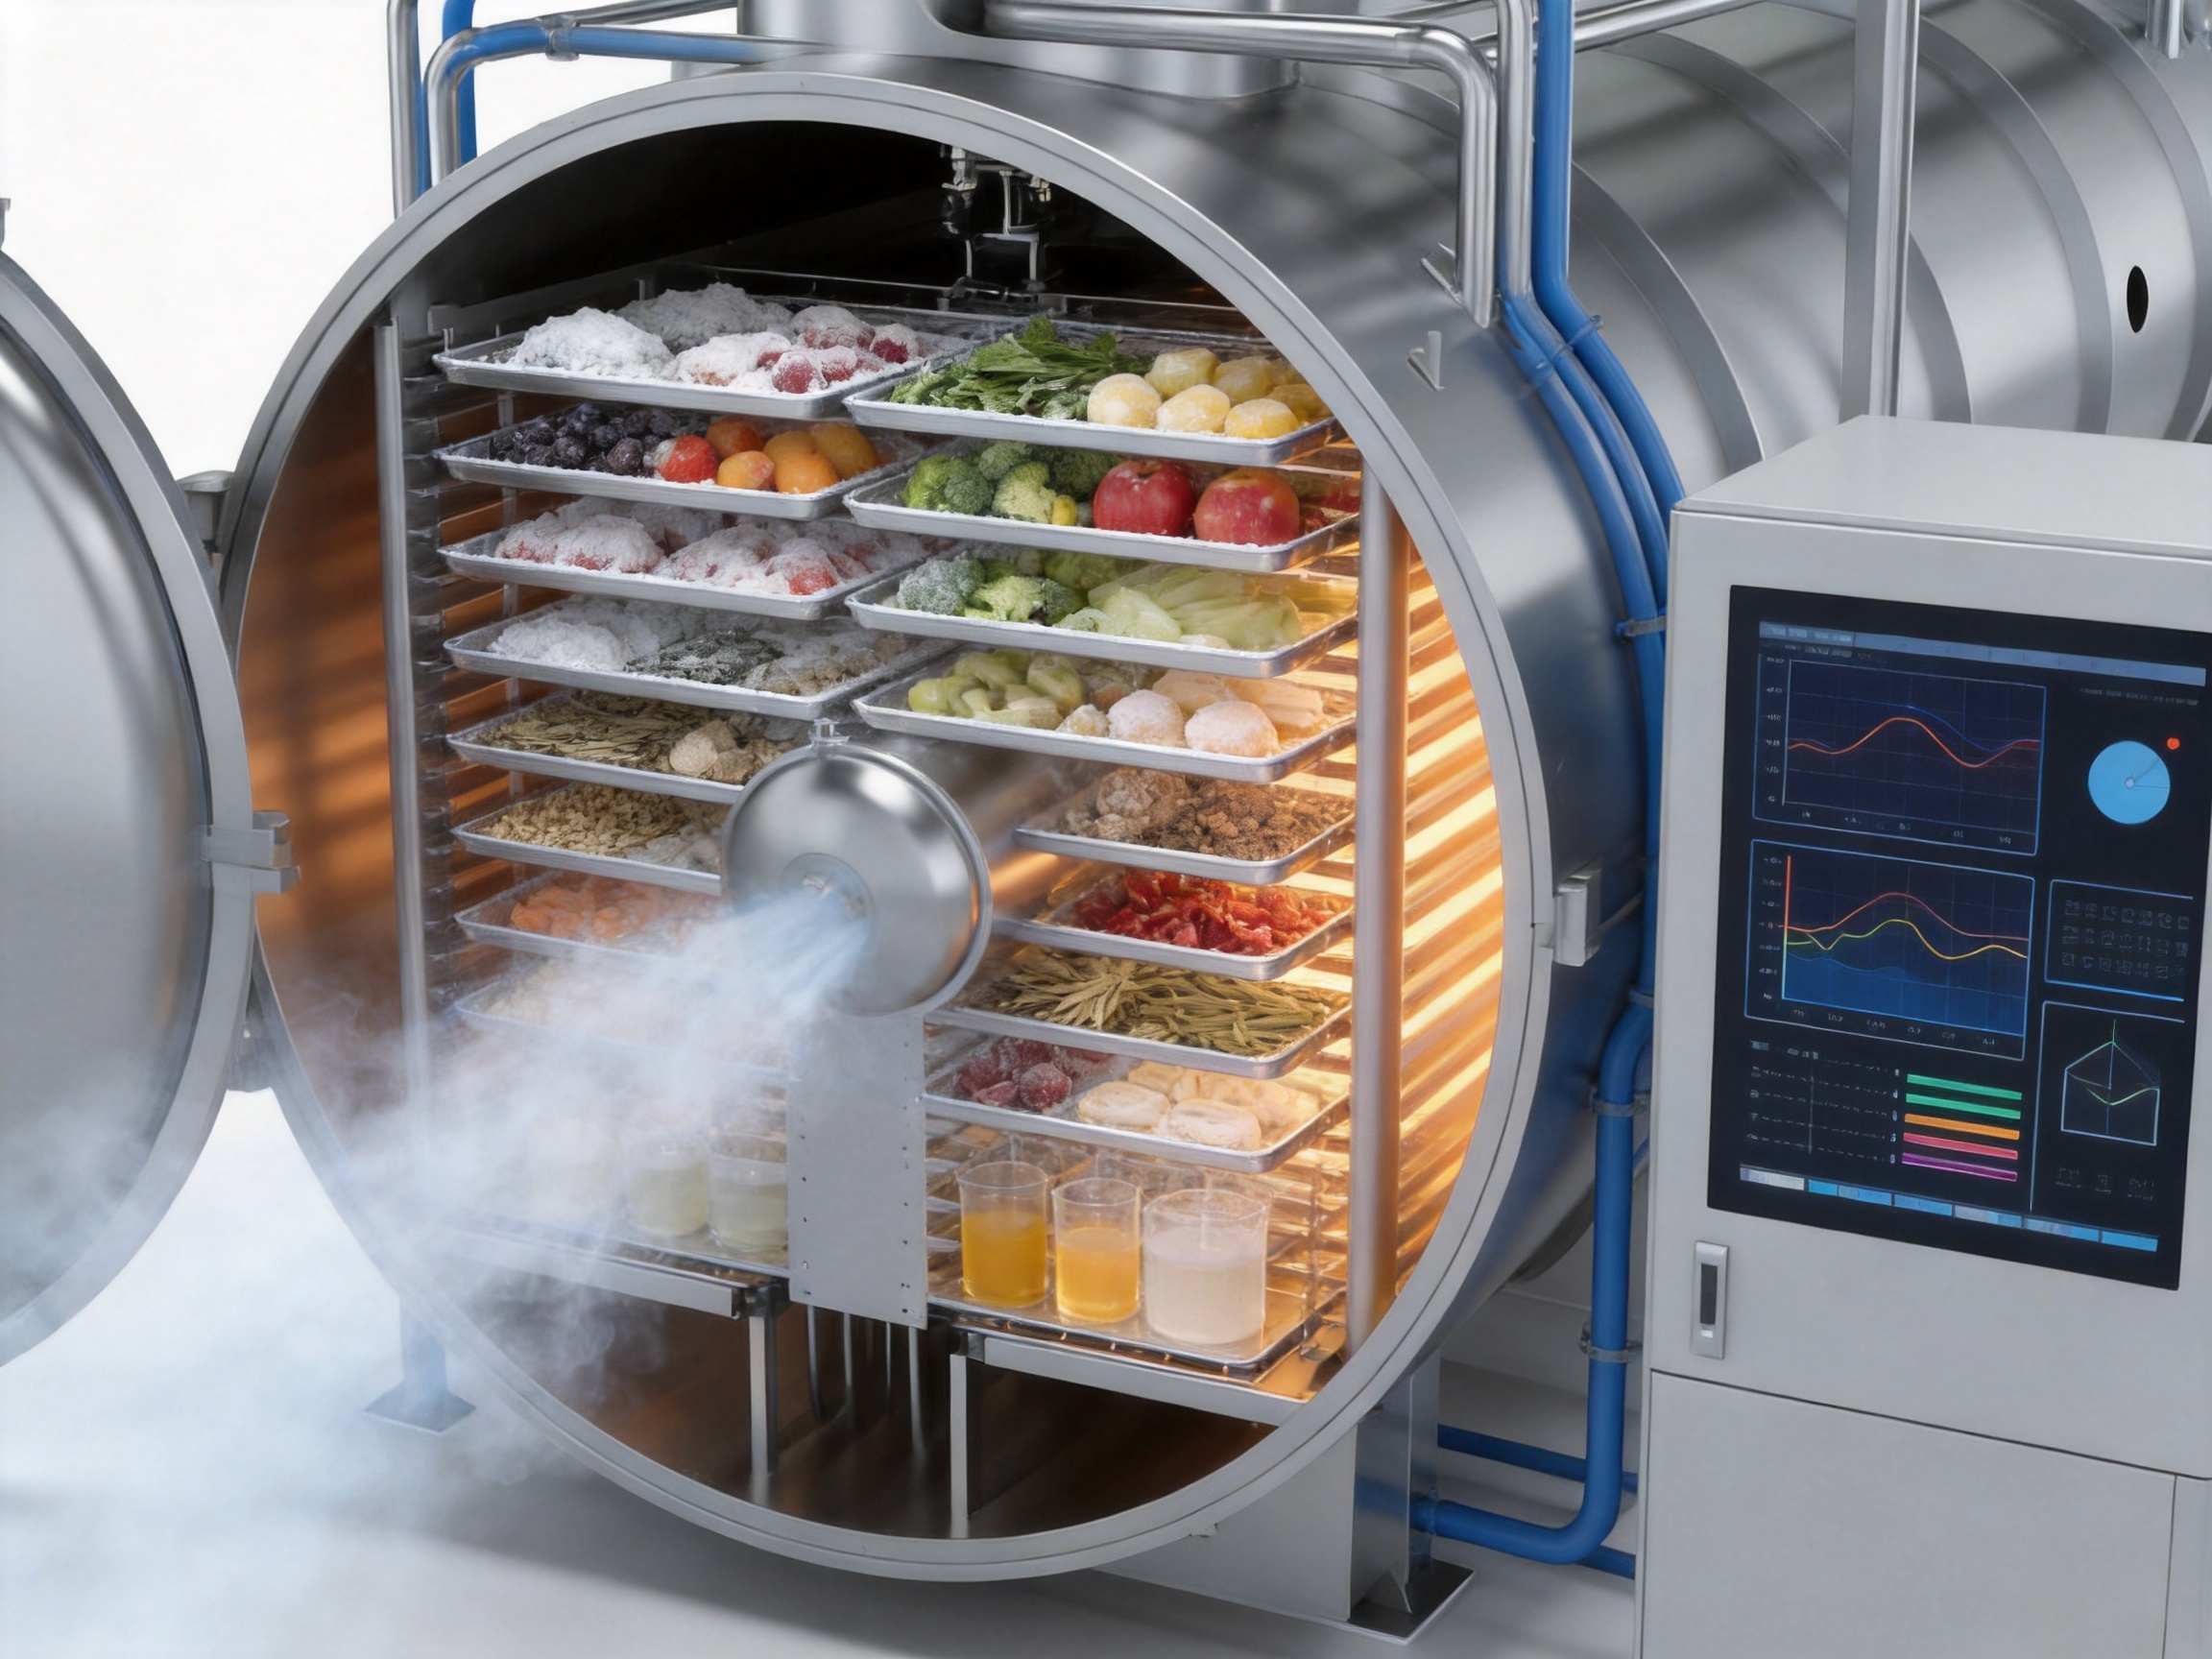
Freeze-drying, also called lyophilization, removes water from frozen products through sublimation under vacuum. The process normally involves three main stages: freezing, primary drying, and secondary drying. During primary drying, ice changes directly from a solid state into vapor. During secondary drying, remaining bound moisture is removed to achieve the required final moisture content.
Although the basic principle is straightforward, industrial execution is highly demanding. The product must remain frozen while sufficient heat is supplied to drive sublimation. If the temperature rises too quickly, the frozen structure may collapse, resulting in poor appearance, reduced rehydration performance, loss of texture, or damage to sensitive active ingredients. If heat transfer is too slow or uneven, cycle times increase and product moisture may vary from one tray position to another.
At a large production scale, small variations become significant. A temperature deviation of only a few degrees across a large shelf area can produce noticeable differences in moisture content, color, structure, or biological activity. Similarly, inadequate vacuum capacity can slow vapor removal and limit the amount of material that can be processed in a single batch.
The BLK-FD-200 addresses these challenges through a large but carefully controlled processing environment. Its shelf and heat-transfer design is intended to keep inter-shelf temperature deviation within approximately ±1°C. This level of uniformity supports repeatable drying conditions and helps operators achieve more consistent results throughout the chamber.
Large-scale equipment must also handle the practical challenges of loading, unloading, cleaning, maintenance, defrosting, and production scheduling. A machine that offers a large nominal capacity but requires long downtime between batches may not provide the expected output. For this reason, the BLK-FD-200 emphasizes not only chamber volume but also cycle management, cold-trap performance, shared vacuum technology, parallel operation, and intelligent system control.
The primary specifications of the BLK-FD-200 define it as a large-scale industrial freeze-drying system rather than a laboratory or pilot machine. Its capacity is suitable for manufacturers that need to process substantial quantities of products while maintaining controlled and repeatable conditions.
Specification |
BLK-FD-200 Value |
Production Significance |
Freeze-drying area |
202.2 m² |
Provides a large effective surface for commercial batch processing |
Standard loading capacity |
2,000 kg |
Supports high-volume production of solid or prepared materials |
Liquid loading capacity |
4,000 L |
Accommodates liquid formulations and high-volume feed preparation |
Ultimate vacuum level |
≤10 Pa |
Creates the low-pressure environment required for efficient sublimation |
Structural material |
8 mm thick 304 stainless steel |
Provides structural stability, corrosion resistance, and long service life |
Material trolley arrangement |
Typically accommodates eight sets |
Supports organized loading and unloading; manual or automatic options are available |
Heating options |
Electric or steam |
Allows the system to match available utilities and process requirements |
Actual throughput depends on the product, loading thickness, material density, initial moisture content, formulation, freezing characteristics, target residual moisture, and selected process parameters. The stated 2,000-kilogram standard loading capacity should therefore be evaluated alongside the product recipe and desired cycle time rather than treated as an identical output for every material.
The drying chamber is the central pressure boundary of a freeze dryer. It must tolerate repeated vacuum cycles, temperature changes, cleaning procedures, loading stresses, and long-term industrial use. Any weakness in the chamber structure can affect safety, vacuum stability, maintenance requirements, and product protection.
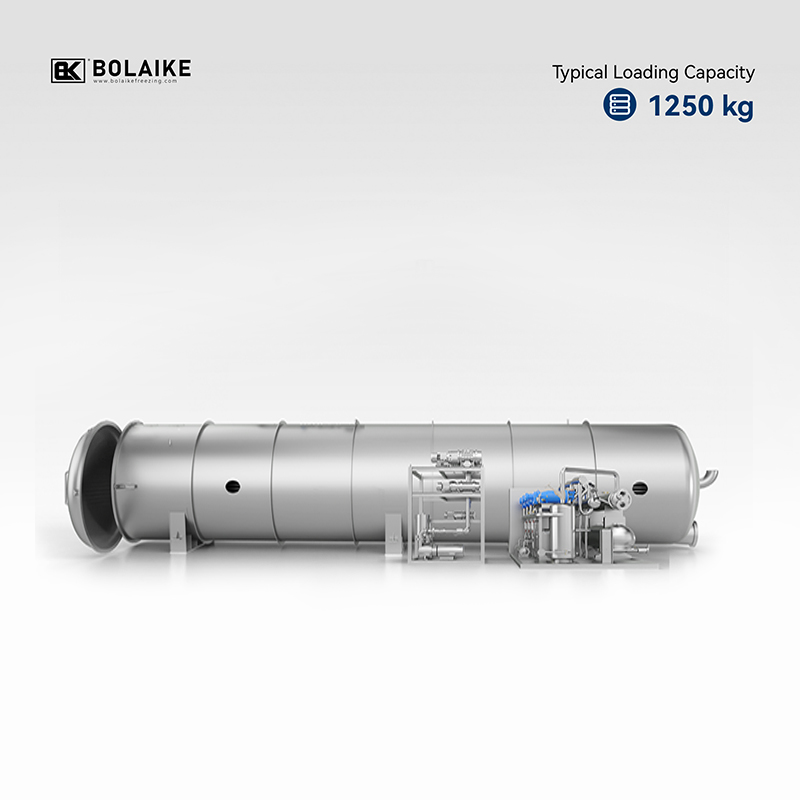
The BLK-FD-200 uses a cylindrical chamber structure designed for demanding vacuum operation. Cylindrical pressure vessels distribute mechanical stress efficiently and provide a robust geometry for maintaining chamber integrity under negative pressure. The chamber is constructed from 8-millimeter-thick 304 stainless steel, a widely used material for food, pharmaceutical, chemical, and biological processing equipment.
304 stainless steel offers a combination of corrosion resistance, strength, cleanability, and compatibility with many industrial products. Its smooth metallic surface can support hygienic production practices when paired with appropriate cleaning and sanitation procedures. The heavy-gauge construction also contributes to structural stability and helps the equipment withstand repeated operation over an extended service life.
The system typically accommodates eight sets of material trolleys. Manual and automatic trolley configurations can be selected according to the factory layout, labor model, product characteristics, and automation strategy. Trolley-based handling improves the organization of trays and allows production teams to move prepared materials into and out of the chamber in a controlled sequence.
Chamber and equipment layout positions can be customized. This is important because industrial freeze dryers are rarely installed in identical facilities. Some plants require a straight-line arrangement, while others need an L-shaped layout, external refrigeration units, separate cold-storage integration, cleanroom interfaces, or restricted access for maintenance. Custom positioning can simplify utility connections, improve personnel movement, and help the equipment fit into an existing production building.
Uniform heat transfer is one of the most important performance factors in freeze drying. During primary drying, heat must pass through the shelf or radiation plate into the frozen product. The supplied energy must be sufficient to support sublimation but controlled carefully enough to avoid product collapse or localized overheating.
The BLK-FD-200 uses one-piece radiation plates without welded joints. This construction approach reduces discontinuities in the plate surface and supports stable heat transfer. Welded joints can introduce local changes in thickness, thermal behavior, or surface geometry. A one-piece plate design helps create a more consistent contact and radiation environment across the product area.
The special heat-transfer-fluid circuit design is intended to keep inter-shelf temperature deviation within ±1°C. Consistent fluid circulation across the shelves helps limit hot spots and cold zones, allowing products positioned in different parts of the chamber to experience more similar process conditions.
For food products, this uniformity can help preserve shape, color, aroma, porosity, and rehydration properties. For medicinal herbs and health supplements, it can contribute to more consistent moisture removal and protection of heat-sensitive components. For biological supplies and other sensitive materials, stable shelf conditions support repeatability and reduce the risk of batch-to-batch variation.
Uniform heat transfer also benefits process development. When the equipment responds consistently, engineers can establish recipes with greater confidence. A process designed on one production day is more likely to behave similarly during later cycles, provided that the product formulation and loading conditions remain controlled.
Freeze drying depends on maintaining a sufficiently low pressure for ice sublimation. The ultimate vacuum level of the BLK-FD-200 is specified at no more than 10 Pa. This provides a low-pressure operating environment suitable for industrial sublimation processes.
Vacuum performance is determined by more than the nominal rating of the pump. Chamber volume, product load, moisture release rate, pipe dimensions, valve design, leakage control, cold-trap capacity, and pump configuration all influence actual process performance. During the most active part of primary drying, the system must continuously remove large quantities of water vapor without allowing pressure to rise beyond the process range.
The BLK-FD-200 can combine different vacuum pump technologies, including screw pumps with Roots pump sets, rotary vane pumps with Roots pump sets, and water-ring pumps with Roots pump sets. This modular approach allows the vacuum system to be matched to the required pumping speed, product characteristics, utility conditions, and maintenance preferences.
Variable-frequency control can adjust pump power according to the actual vacuum demand. Rather than operating all pumps continuously at maximum output, the system can regulate capacity as the product moves through different stages of drying. Intelligent variable-frequency combinations can reduce unnecessary energy consumption while maintaining the required vacuum conditions.
Effective vapor management also protects product quality. If vapor is not removed efficiently, pressure may rise, sublimation may slow, and product temperature may increase. A stable vacuum system helps maintain the balance between heat input and vapor removal throughout the cycle.
The refrigeration system performs several critical functions. It freezes the product, maintains low temperatures during the process, and captures sublimated water vapor in the cold trap. The cold trap must remain sufficiently cold to condense or freeze incoming vapor before it reaches the vacuum pumps.
The BLK-FD-200 supports multiple refrigeration panel configurations to meet different site conditions and process requirements. An external refrigeration system can be selected when the customer needs to separate heat-generating machinery from the production area, simplify service access, or integrate the freeze dryer with a larger utility plant. A built-in refrigeration configuration may be suitable when a compact equipment footprint and integrated arrangement are preferred.
A single refrigeration unit can supply cooling to both cold-storage equipment and freeze-drying equipment simultaneously. This configuration can help improve utility coordination and reduce the need for completely independent cooling systems. Intelligent variable-frequency refrigeration units can also dynamically manage the drying process of multiple freeze-drying devices.
This flexibility is particularly valuable for factories that expect future expansion. A system designed around shared refrigeration resources can potentially support additional equipment more efficiently than a collection of isolated units, subject to engineering review and confirmed utility capacity.
Energy consumption is one of the most important long-term operating costs associated with industrial freeze drying. Refrigeration compressors, vacuum pumps, heating systems, defrosting, cooling water, and auxiliary equipment can all contribute substantially to the total cost of production.
The BLK-FD-200 is equipped with residual cold recovery and intelligent control functions. Compared with traditional equipment, the standard configuration is described as capable of reducing energy consumption by approximately 10% to 15%. Depending on the selected system configuration, process design, operating conditions, and comparison baseline, broader energy-saving performance may reach approximately 20% to 40% in specific applications.
These figures should be evaluated through an application-specific energy assessment because actual savings depend on product type, cycle design, ambient conditions, utility prices, equipment loading, and operator practices. Nevertheless, the underlying energy-recovery technologies provide practical opportunities to reduce avoidable losses.
In a conventional refrigeration arrangement, some cold energy may be used once and then discharged or lost during system transitions. The cold-recovery system captures and reuses refrigeration capacity to pre-cool the next refrigeration stage. This reduces the continuous high-load demand placed on the compressors.
The stated design can reduce the overall compressor load by approximately 20% to 30% under suitable operating conditions. Lower compressor loading can reduce electricity consumption, improve equipment utilization, and potentially reduce thermal stress on refrigeration components.
Freeze-drying also involves the movement of heat through the heating and sublimation stages. In many traditional systems, excess heat is discharged. The heat-recovery design can reuse available heat, including steam heat where applicable, for material drying or related process requirements.
For materials requiring a heating temperature of no more than 35°C, the supplied technical material indicates that up to 99% of the relevant heating energy may be saved through heat recovery in the stated application context. When the required material heating temperature is below 80°C, approximately 10% of energy consumption may be saved through waste-heat-enhanced operation.
These figures are process-specific and should not be interpreted as universal performance guarantees. A detailed engineering review is required to determine the usable heat source, temperature level, recovery timing, and actual savings for each product.
The heat pump and economizer system is designed to improve compressor coefficient of performance, or COP. The stated system can increase compressor COP to approximately 4.8 to 5.9, representing a potential five- to six-fold improvement in energy efficiency compared with certain traditional freeze-drying arrangements.
A higher COP means that more useful heating or cooling effect can be obtained from each unit of electrical energy under defined operating conditions. This can help reduce operating cost and improve the overall environmental performance of the plant.
Large-scale freeze-drying equipment generates and manages a large amount of process information. Shelf temperatures, product temperatures, chamber pressure, refrigeration conditions, pump status, cold-trap behavior, valve positions, heating output, and cycle times must all be coordinated.
The BLK-FD-200 includes an intelligent central control system capable of managing the operational status of connected equipment. Centralized control can simplify production management by bringing major process functions into one coordinated operating environment.
Remote monitoring through a mobile application is supported. Remote access can allow authorized personnel to review equipment status, receive alerts, track operation, and respond more quickly to abnormal conditions. This is particularly useful for production facilities that operate continuously or have technical teams located away from the equipment room.
Multiple language options can be customized to support international users. A clear and familiar interface can reduce training time, improve operator confidence, and lower the possibility of errors caused by misunderstanding control instructions.
Intelligent variable-frequency control is applied to vacuum and refrigeration functions. This enables the system to match equipment output to actual process demand instead of using maximum capacity at all times. In addition to reducing energy consumption, demand-based operation can help limit unnecessary mechanical wear.
One of the strongest advantages of the BLK-FD-200 platform is its ability to support parallel operation of multiple freeze dryers. In a properly engineered production system, units can be operated according to staggered feeding, drying, unloading, and defrosting schedules.
When one unit enters the final drying stage or requires cold-trap defrosting, other units can remain in operation. Shared refrigeration, vacuum, and control technologies can help maintain system stability while individual chambers move through different stages of the production cycle.
The supplied product information states that two units can achieve an output comparable to three units under suitable parallel-production conditions. This advantage is associated with staggered operation, shared system resources, and reduced idle time. The actual result depends on product recipes, batch duration, defrosting requirements, loading logistics, and the design of the complete production line.
Parallel operation can shorten batch intervals and improve the utilization of auxiliary infrastructure. It can also provide greater flexibility when products have different drying cycles. One chamber may process fruit, another may process medicinal materials, and a third may be prepared for a subsequent product, subject to sanitation and process-management requirements.
The optional patented intermediate isolation valve further supports continuous production planning. The valve separates the drying chamber from the cold trap during selected operating conditions. This helps control water-vapor flow direction and vacuum status during freeze drying and cold-trap defrosting.
By reducing the risk of vapor backflow and allowing more precise isolation, the intermediate valve can shorten transition intervals between production stages. It also helps protect product quality and improve operational safety during defrosting.
The performance of a large-scale freeze dryer depends heavily on manufacturing precision. A system may contain a pressure chamber, shelves, refrigeration circuits, heat-transfer circuits, vacuum piping, pumps, valves, sensors, control cabinets, insulation, trolleys, and auxiliary equipment. These components must work together reliably after installation at the customer’s facility.
The manufacturer applies five core inspection workflows and 58 inspection procedures to verify overall machine craftsmanship. A multi-stage inspection approach allows quality checks to be performed throughout production instead of relying only on a final visual examination.
Inspection may include material verification, dimensional checks, welding and surface evaluation, pressure testing, vacuum testing, electrical inspection, control-system verification, refrigeration performance testing, and functional operation. Each stage helps identify issues before shipment and reduces the risk of costly corrections during installation.
The refrigeration system undergoes more than 48 hours of pressure-holding testing. Extended pressure holding helps reveal leaks that may not become evident during a short test. Stable pressure over the required period provides greater confidence in the integrity of refrigeration piping, joints, valves, and related components.
The complete machine undergoes two pressure tests, including high-pressure and low-pressure testing. A dedicated high-pressure test lasting 48 hours is used to verify the ability of the system to withstand defined operating and safety conditions.
Pressure testing is especially important for large equipment because the length and complexity of piping increase the number of potential connection points. A disciplined test procedure supports safer commissioning, more stable operation, and easier maintenance planning.
Factory inspection is not limited to individual components. The complete machine must be checked as an integrated system. Pumps, refrigeration units, heating circuits, valves, sensors, and controls must respond correctly to operating commands and protective functions.
By combining component-level and system-level inspection, the manufacturer can improve shipment readiness. This approach is valuable for international projects, where equipment may travel long distances and installation costs can be substantial. Detecting a problem before delivery is generally more efficient than diagnosing it after the equipment has arrived at the customer’s plant.
The BLK-FD-200 is suitable for processing a broad range of materials. The correct process parameters depend on the raw material, formulation, target moisture, desired texture, and applicable industry standards.
Fruits, vegetables, instant foods, prepared meals, meat products, seafood, dairy-based products, beverages, flavor ingredients, and specialty food products can benefit from freeze drying. The low-temperature process helps preserve shape, color, aroma, nutritional value, and rehydration characteristics.
Freeze-dried food is also valued for its low final moisture content, long shelf life, reduced transportation weight, and rapid preparation. The BLK-FD-200 provides the surface area and loading capacity required by food manufacturers serving industrial and export markets.
Medicinal herbs and botanical materials may contain heat-sensitive components that can be affected by conventional drying methods. Vacuum freeze drying provides a lower-temperature alternative that can help preserve appearance and selected functional properties.
Uniform shelf temperature and controlled vacuum are especially important when processing products with different shapes, densities, or moisture levels. Stable conditions can help reduce variation between trays and improve the consistency of finished materials.
Health supplements may be processed as extracts, liquid formulations, powders, or structured products. Freeze drying can help create porous, rapidly rehydratable materials while protecting sensitive ingredients from excessive heat.
The 4,000-liter liquid loading capacity makes the equipment suitable for large-volume liquid preparations, subject to the formulation’s foaming behavior, viscosity, freezing characteristics, and final product requirements.
Biological products can require highly controlled temperature and vacuum conditions. Freeze drying may be used for selected biological materials, laboratory products, cultures, and related supplies where preserving activity and storage stability is important.
For these applications, equipment selection must be combined with validated process development, appropriate cleaning procedures, data management, and applicable regulatory controls.
Certain chemical materials, catalysts, specialty compounds, and temperature-sensitive intermediates can be processed by vacuum freeze drying. The suitability of the process depends on material compatibility, solvent behavior, flammability, toxicity, and the design of the vacuum and exhaust systems.
Before production, customers should conduct a technical review covering material safety, solvent recovery, equipment materials, ventilation, and compliance requirements.
The capacity of a freeze dryer varies according to material density and loading characteristics. Based on a tray area of approximately 200 square meters and a loading height of 35 millimeters, the per-chamber processing capacity of the BLK-FD-200 may vary as shown below.
Material Category |
Indicative Processing Capacity |
Important Consideration |
Food category |
3,000–4,000 kg |
Depends on bulk density, moisture, and loading uniformity |
Solution category |
2,500–3,000 kg |
Depends on solids content, viscosity, and freezing behavior |
Fruits and vegetables |
2,000–2,500 kg |
Depends on cut size, shape, water content, and tray arrangement |
These figures are indicative and should be adjusted according to material density and process conditions. Product trials are recommended before finalizing production capacity, cycle time, and utility requirements.
The BLK-FD-200 offers several advantages over conventional large freeze-drying systems that rely on fixed-speed pumps, isolated refrigeration units, welded radiation plates, limited control integration, and long transition times.
First, its energy-management strategy addresses both cold and heat recovery. Traditional systems may consume substantial energy because compressors operate continuously at high load and waste heat is discharged. The BLK-FD-200 can reuse available energy and adjust equipment output according to process demand.
Second, the one-piece radiation plate and specialized heat-transfer circuit support improved temperature uniformity. Consistent shelf conditions are especially valuable in large chambers, where uneven heat transfer can lead to quality variation.
Third, the equipment supports multiple vacuum-pump combinations. This gives users greater flexibility than a fixed pump arrangement and allows the system to be configured around the required vacuum speed, product load, maintenance strategy, and available utilities.
Fourth, parallel operation can improve productivity. Instead of waiting for one machine to complete every stage, several units can be scheduled in a coordinated sequence. Shared vacuum and refrigeration technologies can reduce idle periods and make better use of plant infrastructure.
Fifth, the optional intermediate isolation valve improves process continuity. It helps separate the chamber and cold trap during defrosting and reduces the risk of water-vapor backflow. This can support shorter batch intervals and safer transitions.
Sixth, the system offers flexible heating choices. Electric heating may suit facilities without steam infrastructure or those requiring highly responsive control. Steam heating may be preferred where a reliable central steam supply already exists and operating costs favor that arrangement.
Finally, the equipment can be customized in terms of chamber location, unit placement, trolley handling, refrigeration configuration, control language, and production-line integration. This flexibility can be more valuable than a single headline specification when a machine must fit an existing factory.
Jiangsu Bolaike Freezing Technology Development Co., Ltd. was established in 2014 in Changzhou, Jiangsu, China. Its predecessor, Changzhou Zhongleng Refrigeration Equipment Co., Ltd., entered the refrigeration industry in 2003 and began developing vacuum freeze-drying technology at an early stage.
The company specializes in the research, development, manufacturing, and sales of vacuum freeze-drying and refrigeration equipment. Its engineering experience covers food, fruits and vegetables, medicinal herbs, health supplements, biological products, chemical materials, and other industries.
Rather than operating only as an equipment assembler, the company maintains an integrated team covering research and development, engineering, sales, installation, commissioning, and after-sales service. This integrated model helps connect product design with actual production requirements.
The company has established long-term partnerships with universities and research organizations, including the Chinese Academy of Agricultural Sciences, the Jiangsu Academy of Agricultural Sciences, and Jiangnan University. Cooperation with research institutions can support process development, equipment improvement, material testing, and technical innovation.
More than 100 national invention and utility model patents are associated with the company. These include technologies related to cold recovery, heat recovery, heat-pump and economizer systems, isolation valves, and vacuum freeze-drying system design.
The manufacturing base covers approximately 24,000 square meters. A modern production facility of this scale can support the fabrication, assembly, testing, and inspection of large industrial equipment. It also provides space for organizing different manufacturing stages, storing components, conducting system tests, and preparing equipment for shipment.
The company reports that its equipment achieves energy savings of approximately 20% to 30% in suitable applications and that its products have been exported to more than 30 countries and regions. International project experience can help the manufacturer understand different electrical standards, utility conditions, factory layouts, documentation requirements, and customer expectations.
Large freeze dryers require careful installation because they connect to electrical power, refrigeration utilities, vacuum systems, heating sources, cooling systems, drainage, ventilation, and production-handling areas. The equipment must also be aligned, insulated, connected, tested, and integrated with the customer’s operating procedures.
Installation support helps ensure that the system is assembled according to engineering specifications. Commissioning verifies that the refrigeration, vacuum, heating, control, safety, and material-handling systems operate as intended under site conditions.
After commissioning, operators should receive training in loading procedures, recipe management, alarm response, cleaning, defrosting, maintenance, and basic troubleshooting. A well-trained operating team can improve production consistency and reduce avoidable downtime.
After-sales support is particularly important for a large industrial machine because the cost of an unplanned interruption can be substantial. Technical support may include remote diagnosis, spare-parts guidance, control-system assistance, maintenance recommendations, and process consultation.
Customers should begin with the product rather than the equipment size. The manufacturer needs information about the raw material, initial moisture, target final moisture, loading thickness, tray format, desired texture, temperature sensitivity, expected annual output, and required cycle time.
The second step is to review utilities. Electrical capacity, steam pressure, cooling water, ambient temperature, drainage, compressed air, ventilation, and available floor area all affect the final configuration. The choice between electric and steam heating should be based on both technical suitability and long-term operating economics.
The third step is to determine the desired automation level. Manual trolley handling may be suitable for certain facilities, while automatic handling can reduce labor requirements and improve repeatability in high-throughput production. The central-control system should be matched to the customer’s data, traceability, remote-monitoring, and language requirements.
The fourth step is to consider future expansion. If the customer expects production growth, the layout should reserve space for additional chambers, refrigeration units, vacuum pumps, cold storage, and handling equipment. Parallel system design can make later expansion more practical.
The fifth step is to define quality and compliance requirements. Food, pharmaceutical, biological, and chemical applications may have different requirements for materials, cleaning, documentation, validation, data recording, and environmental control. These requirements should be established before equipment design is finalized.
The BLK-FD-200 has a freeze-drying area of 202.2 square meters. The product information also refers to a tray area of approximately 200 square meters when describing indicative batch capacity.
The standard loading capacity is 2,000 kilograms. Actual capacity depends on material density, moisture content, loading thickness, product shape, formulation, and the selected freeze-drying cycle.
The stated liquid loading capacity is 4,000 liters. The practical capacity for a specific liquid depends on solids concentration, viscosity, foaming behavior, freezing characteristics, and the desired tray loading depth.
The ultimate vacuum level is specified at no more than 10 Pa. Actual operating pressure depends on product vapor load, chamber conditions, pump configuration, piping, seals, and process parameters.
Yes. Electric and steam heating options are available. The appropriate selection depends on the customer’s utility infrastructure, process requirements, energy costs, control preferences, and site conditions.
The system uses one-piece radiation plates without welded joints and a specially designed heat-transfer-fluid circuit. These features are intended to keep inter-shelf temperature deviation within approximately ±1°C.
The system can combine screw pumps with Roots pump sets, rotary vane pumps with Roots pump sets, or water-ring pumps with Roots pump sets. The final configuration should be selected according to pumping speed, product characteristics, maintenance requirements, and available utilities.
Yes. The BLK-FD-200 supports parallel operation of multiple units. Staggered feeding, drying, unloading, and defrosting can help reduce production interruptions and improve equipment utilization.
The optional intermediate isolation valve separates the drying chamber from the cold trap during selected operating conditions. It helps control vapor flow and vacuum status, reduce vapor backflow, support safer defrosting, and shorten batch intervals.
Yes. External and built-in refrigeration configurations are available. The choice depends on factory layout, maintenance access, available space, heat management, utility planning, and customer preferences.
The equipment can be used for fruits, vegetables, food products, solutions, medicinal herbs, health supplements, biological supplies, chemicals, and other suitable materials. Product trials and process evaluation are recommended before commercial production.
The manufacturing process includes five core inspection workflows and 58 inspection procedures. The equipment also undergoes extended refrigeration pressure-holding tests, high- and low-pressure testing, and integrated machine inspection before shipment.
Yes. Chamber and unit positions can be customized, and manual or automatic material trolleys can be selected. Refrigeration configuration, heating method, control language, vacuum-pump combination, and production-line arrangement can also be reviewed during engineering design.
Remote monitoring through a mobile application is supported. Authorized personnel can use remote access to review equipment status and respond to selected operating conditions or alarms.
Customers should provide the product type, batch size, initial and target final moisture, loading thickness, expected output, desired cycle time, available utilities, factory dimensions, automation preferences, heating source, and any industry-specific quality or compliance requirements.
The BLK-FD-200 is designed for manufacturers that require high-capacity freeze drying with stable process control, energy-conscious operation, and the flexibility to support future production growth. Its 202.2-square-meter freeze-drying area, 2,000-kilogram standard loading capacity, 4,000-liter liquid capacity, and vacuum capability of no more than 10 Pa provide a strong foundation for industrial processing.
Its main advantages come from the combination of technologies rather than from capacity alone. One-piece radiation plates, uniform heat-transfer circuits, flexible vacuum-pump arrangements, variable-frequency control, cold and heat recovery, optional intermediate isolation, parallel operation, and intelligent central control all contribute to a more efficient production system.
The equipment is further supported by heavy-duty 304 stainless-steel construction, extended pressure testing, comprehensive inspection procedures, customized layouts, multiple heating choices, and international engineering experience. These characteristics make the BLK-FD-200 suitable for demanding applications in food, agricultural products, medicinal materials, supplements, biological supplies, and chemicals.
For companies comparing large-scale freeze-drying systems, the most important evaluation should include total production performance, energy consumption, cycle intervals, maintenance requirements, process stability, factory integration, and long-term technical support. When these factors are considered together, the BLK-FD-200 provides a practical platform for building efficient, reliable, and scalable freeze-drying production capacity.
1. Jiangsu Bolaike Freezing Technology Development Co., Ltd. Product technical materials for the BLK-FD-200 large-scale freeze-drying equipment.
2. Jiangsu Bolaike Freezing Technology Development Co., Ltd. Company profile, manufacturing capabilities, engineering services, and technical development information.
3. General principles of vacuum freeze drying, sublimation, heat transfer, vapor removal, and secondary drying in industrial lyophilization.
4. Technical information concerning industrial refrigeration systems, vacuum pumping arrangements, cold-trap operation, heat recovery, and energy-efficient process control.
5. Materials and hygienic design considerations for 304 stainless-steel processing equipment used in food, pharmaceutical, biological, and chemical applications.
6. Industrial equipment quality-control practices involving pressure testing, refrigeration-system inspection, vacuum verification, commissioning, and preventive maintenance.
 2026/05/28
 2026/05/28
2026/05/28


 Custom Industrial Lyophilizer Freeze Dryer Manufacturers


 English
 русский
 Español
 Français
 Deutsch
 عربى