/faq/part-e-food-applications/

News
Products & Solutions
CONTACT US

+86-18068757376

blk@jsblk.com

No. 29 North Tongjiang Road, Xinbei District, Changzhou City, Jiangsu Province, China
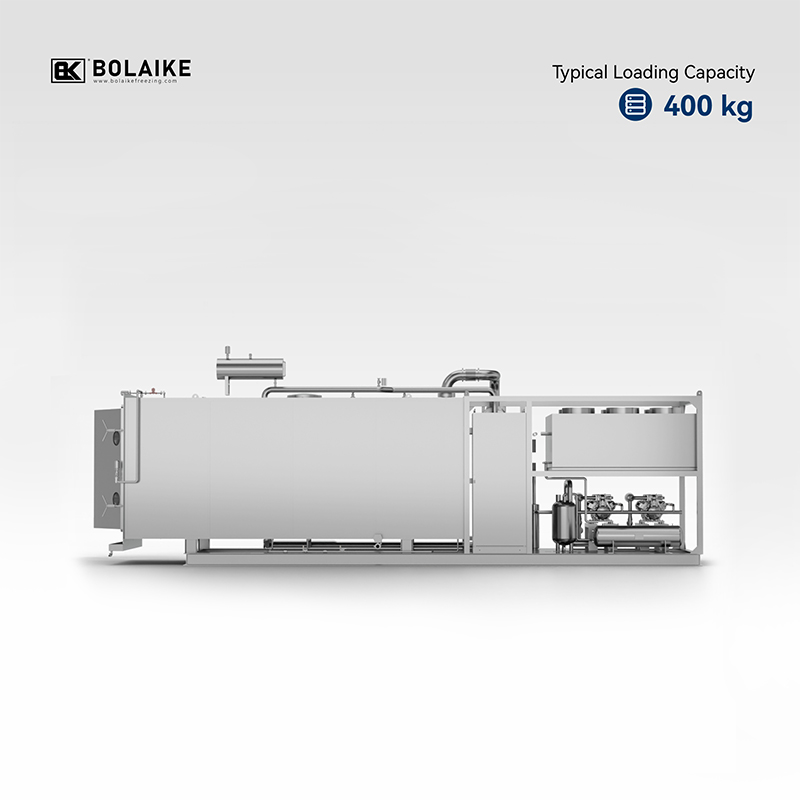
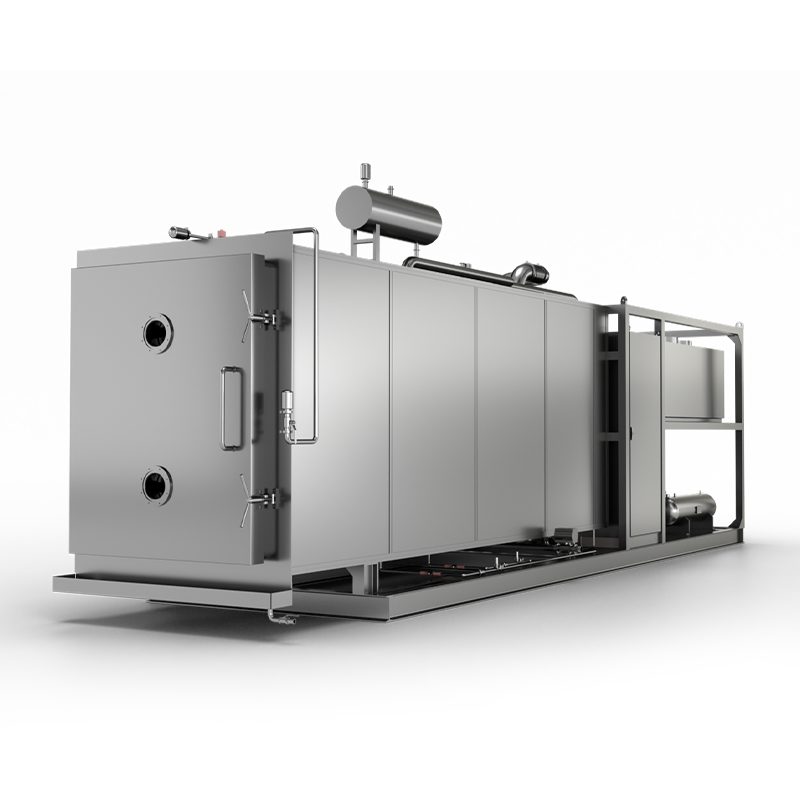
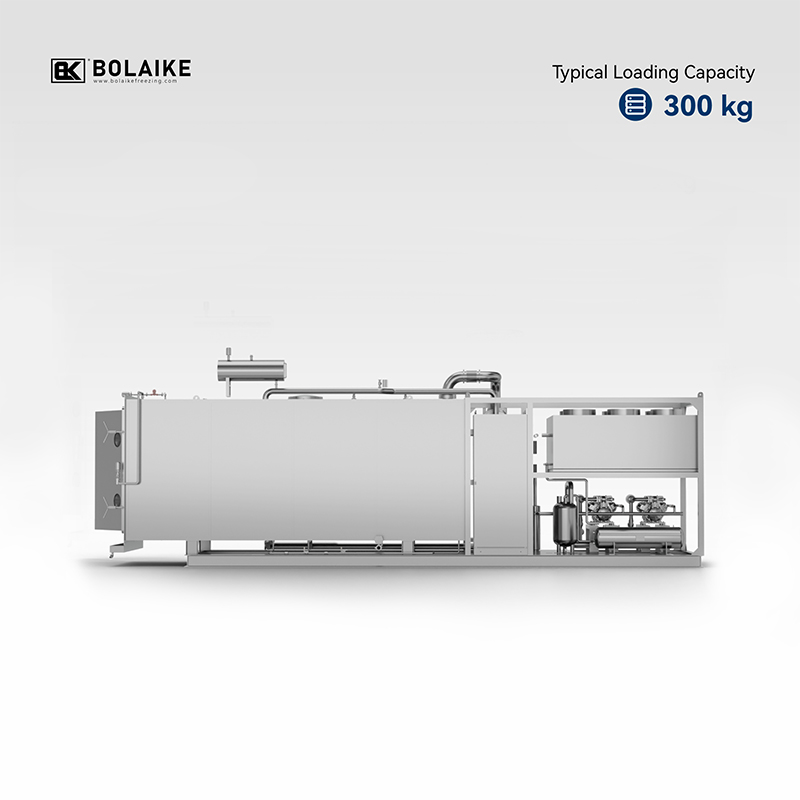
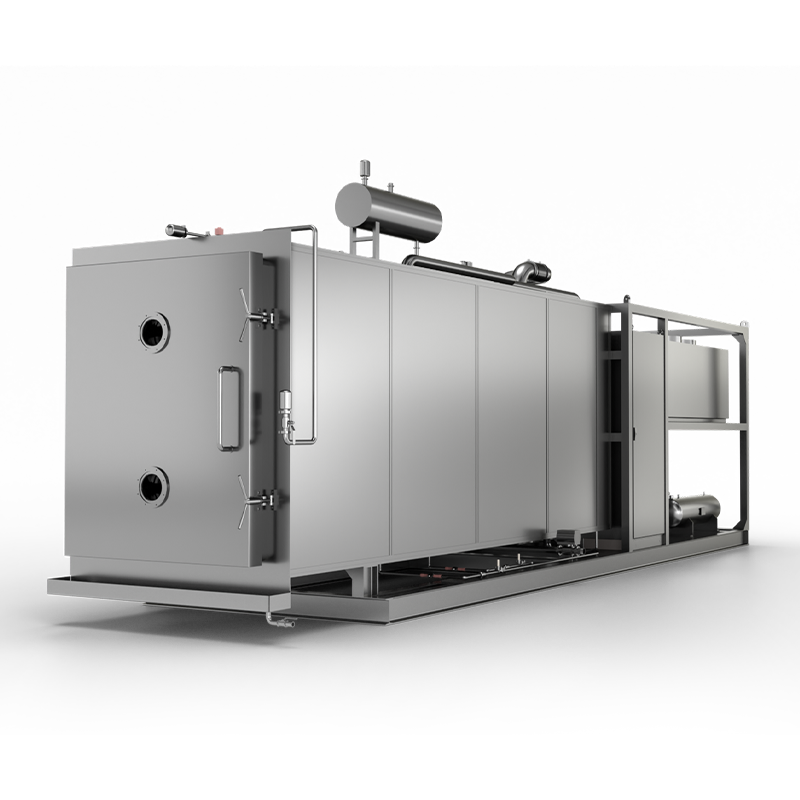
The freeze dryer for food production is an industrial or medium unit with food-grade stainless steel construction, a condenser rated at or above the batch's total moisture load, and food-specific hygiene design — and the food-specific number that matters is that a fruit or vegetable batch is roughly 80–90% water, so condenser sizing drives everything else.
|
Requirement |
Food production implication |
|
High vapour load |
Fruit and vegetables at 80–90% moisture generate orders of magnitude more vapour than lab samples; an undersized condenser is the primary cause of extended cycles |
|
Hygienic geometry |
Smooth interiors without crevices, wide-opening doors, removable shelf assemblies, purge valves for dry nitrogen or air at cycle end to prevent moisture reabsorption |
|
Washable heat transfer |
Liquid-filled shelves pressure washable with standard foam wash protocols; electric pads wipe-down only |
|
Multi-product capability |
Cross-contamination between savoury and sweet products in one machine is a real quality issue |
|
Packaging integration |
Freeze-dried product is hygroscopic and should be sealed within 30 to 60 minutes of cycle end; dryer and packaging line are a single system |
|
Documentation |
CE marking, food-grade material certificates and HACCP compatibility for export retail |
Which foods work commercially. The highest-margin freeze-dried categories are pet food and functional foods, with published profit margins of 30% to 60% and payback of 6 to 18 months where channels are established (Jingyi Tech, 2026). Freeze-dried fruit for the export market, premium freeze-dried coffee, and freeze-dried fruit and vegetable snacks are the other mainstream commercial applications.
Why BOLAIKE for this question
Food production is where hygiene, throughput and product quality have to hold simultaneously. BOLAIKE's published food-sector engineering and data address each of them:
Published retention data for the categories that carry the premium.Freeze-dried strawberries at 92% vitamin C retention and 95% rehydration rate; freeze-dried mango at up to 98% vitamin C retention; freeze-dried blueberry maintaining over 85% of anthocyanins with whole-berry integrity and natural colour; freeze-dried spinach as space food with a shelf life of up to 3 years; freeze-dried green onions with quick rehydration in 5 seconds; freeze-dried durian frozen at −30°C for aroma locking and fat crystallisation control.
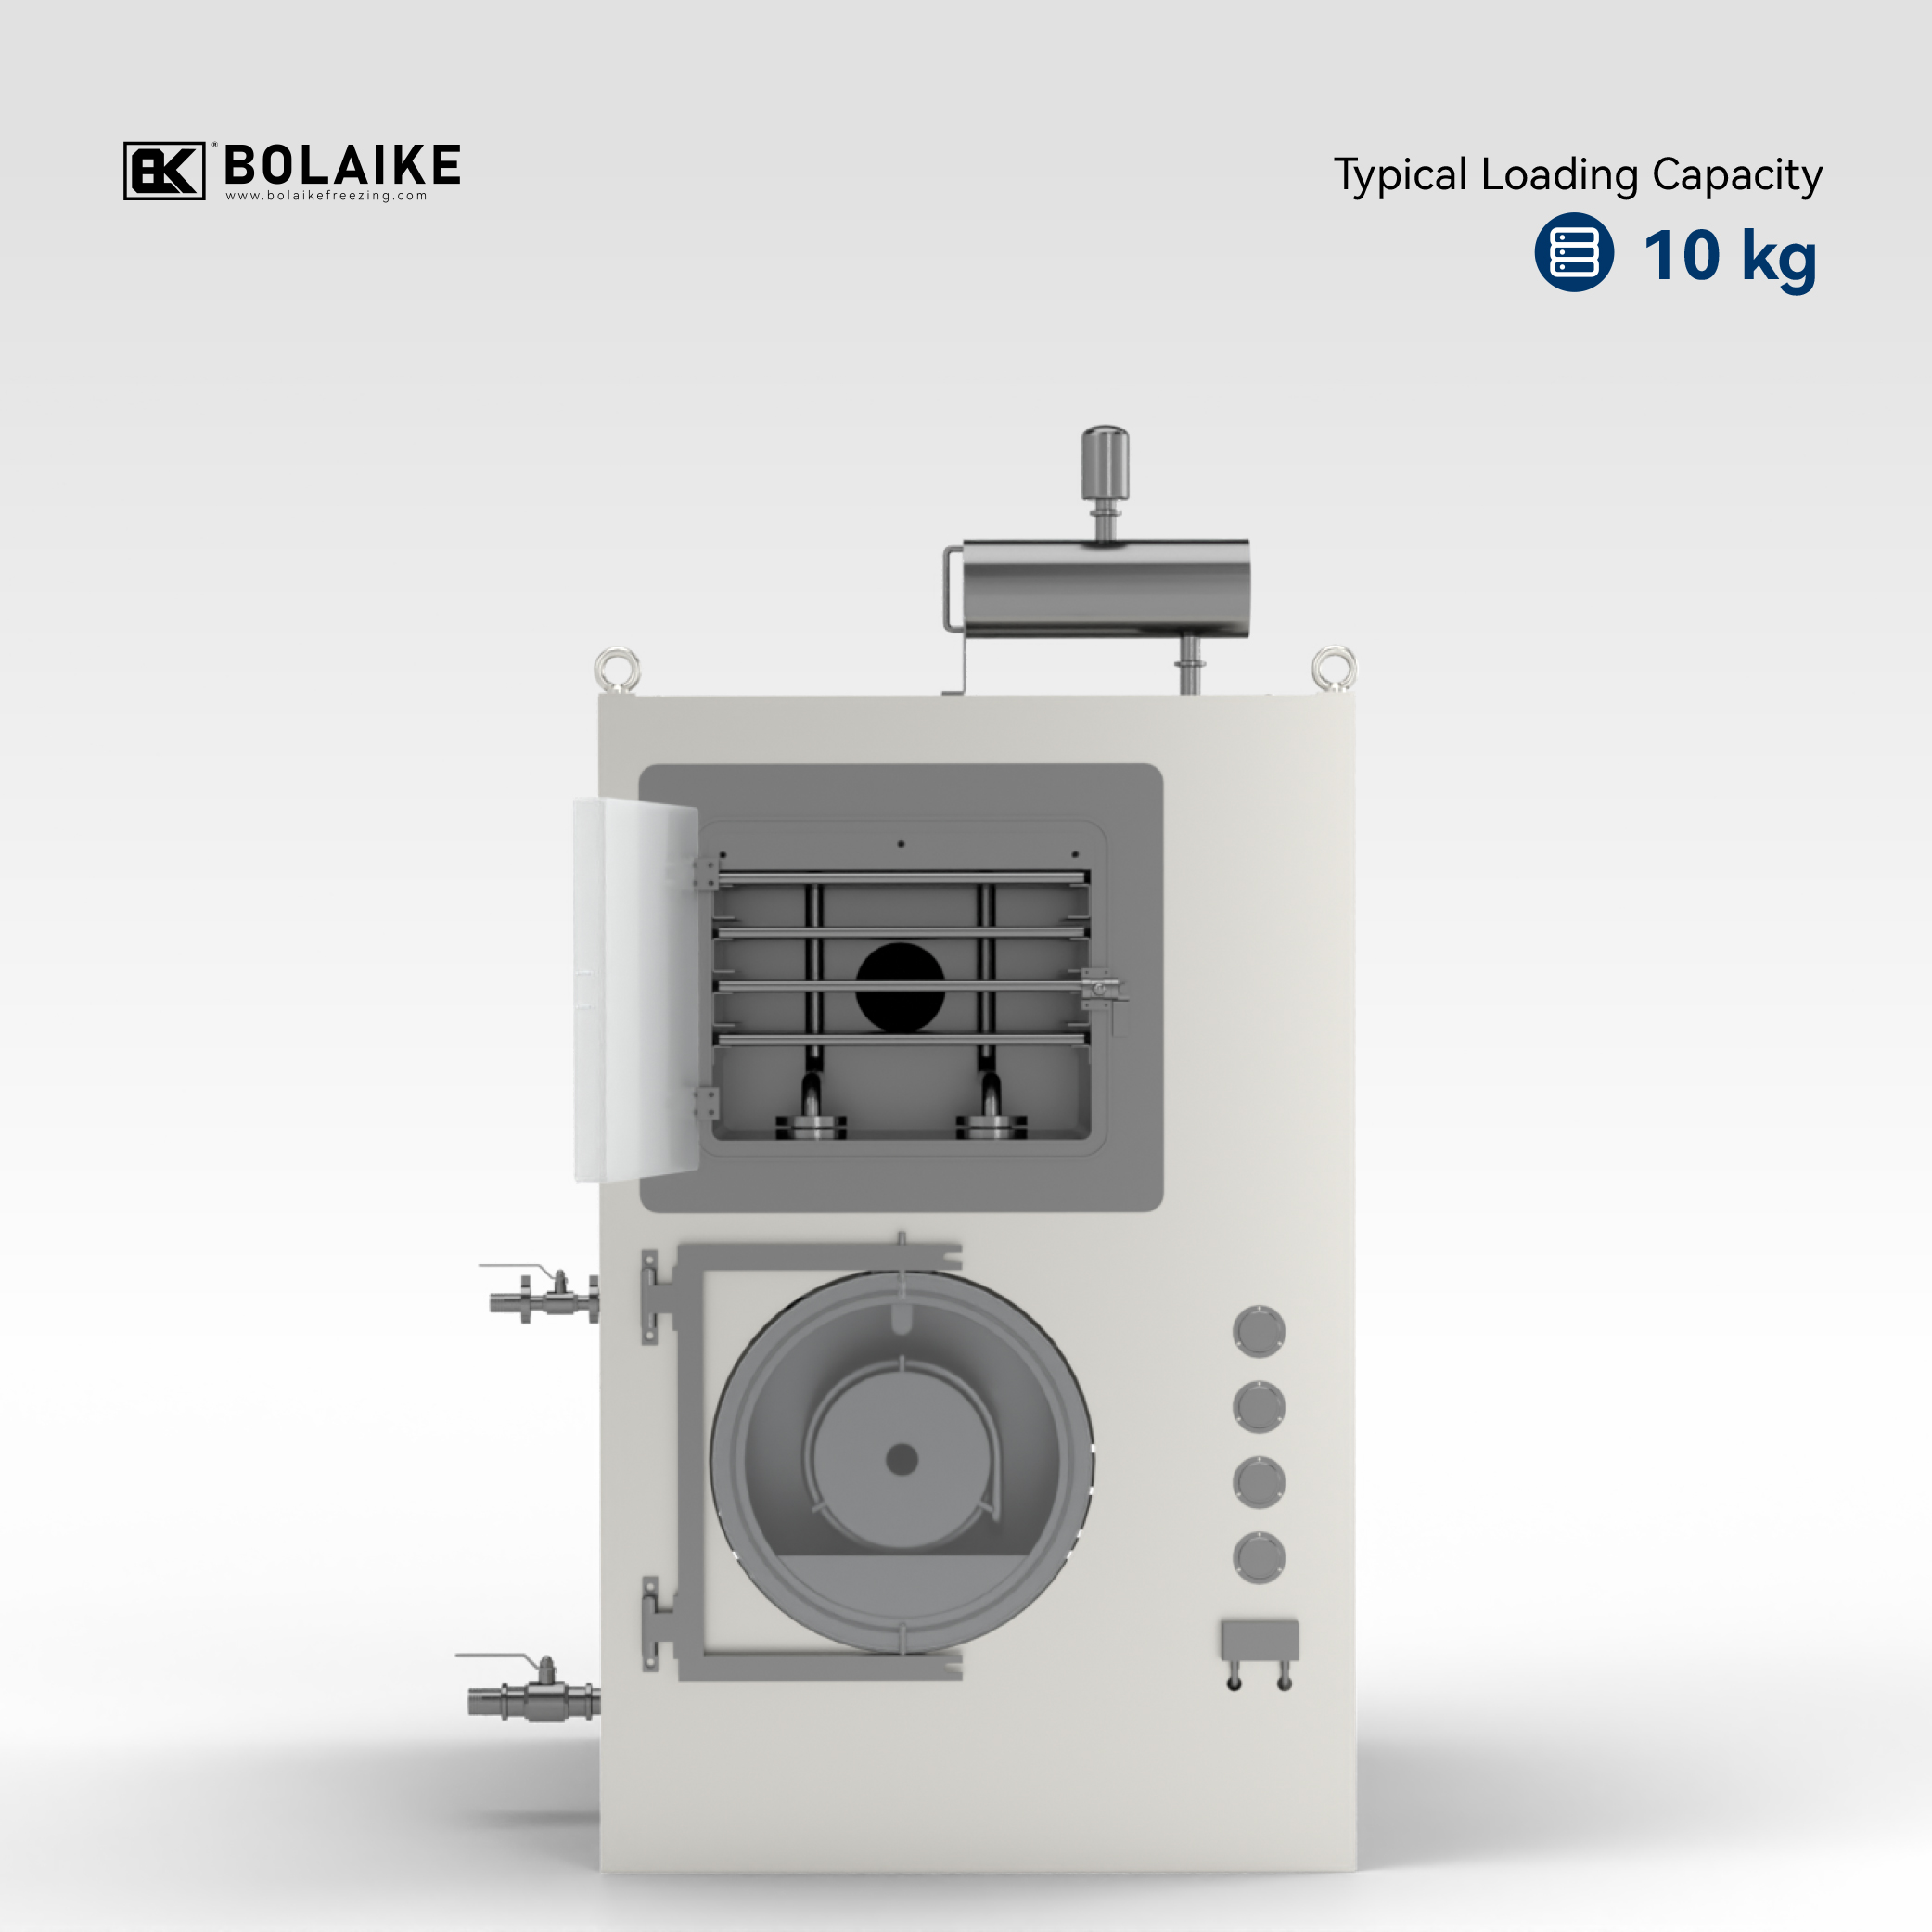
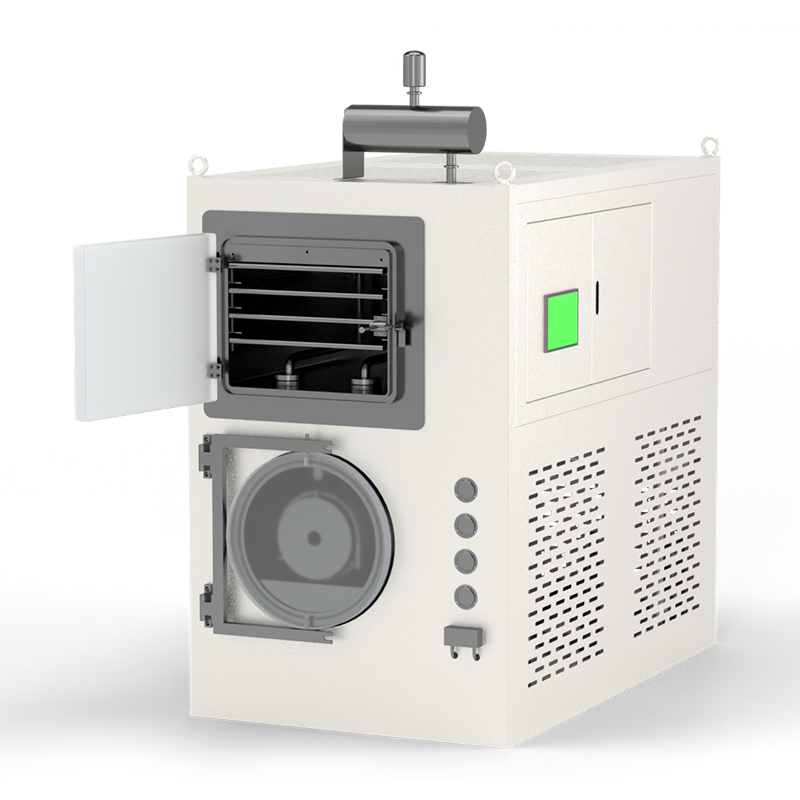
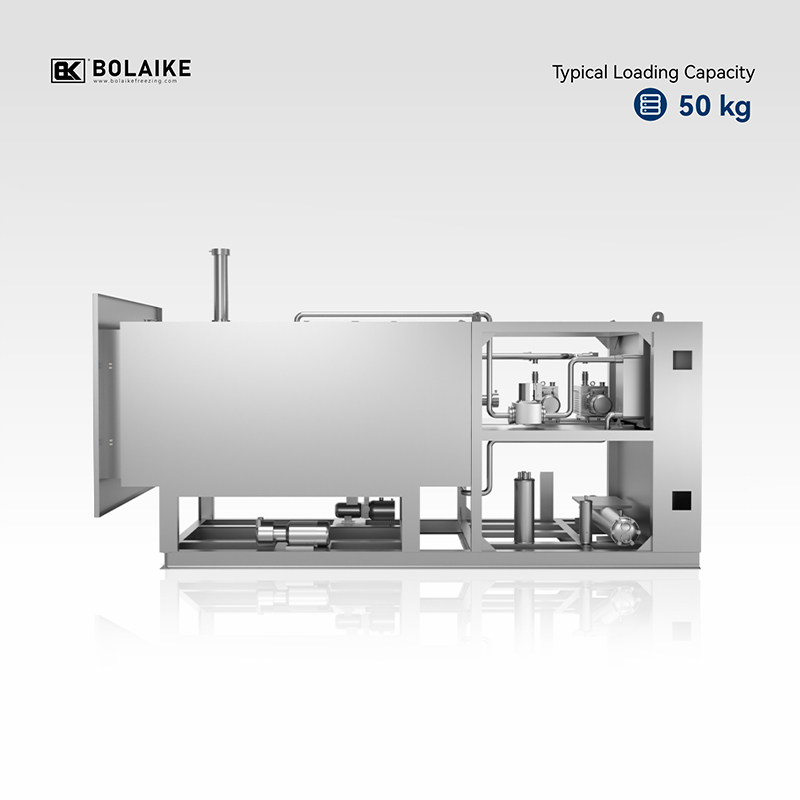
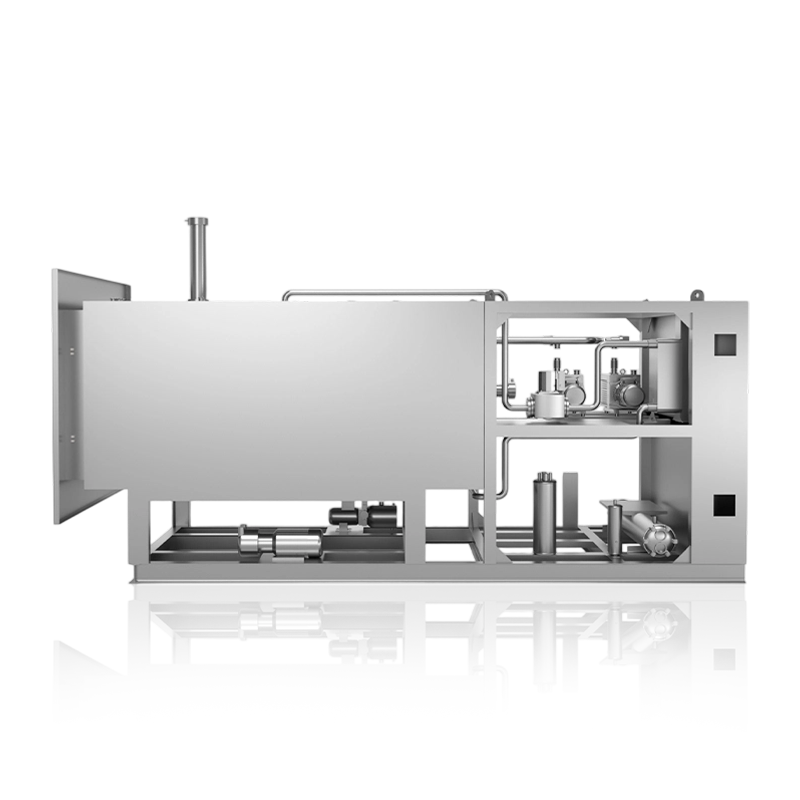
Hygienic geometry built for food. The rectangular chamber design for medium and small-scale machines delivers approximately 25% higher space utilisation and approximately 15% smaller footprint than cylindrical designs of equivalent capacity, and the liquid-circulated double-layer radiant panel system is pressure-washable — which is what makes a single machine viable for multiple product types.
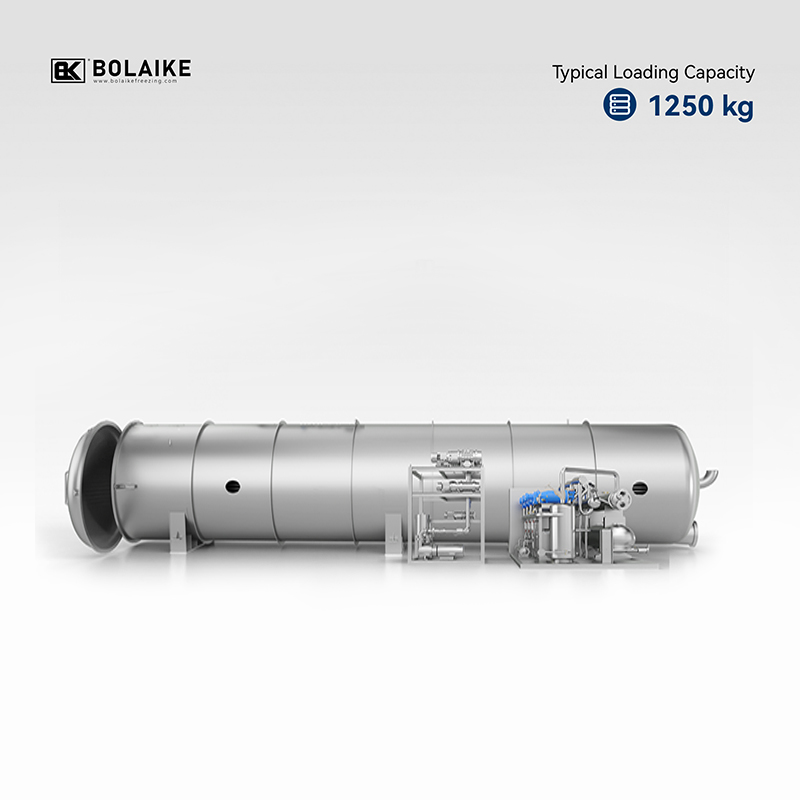
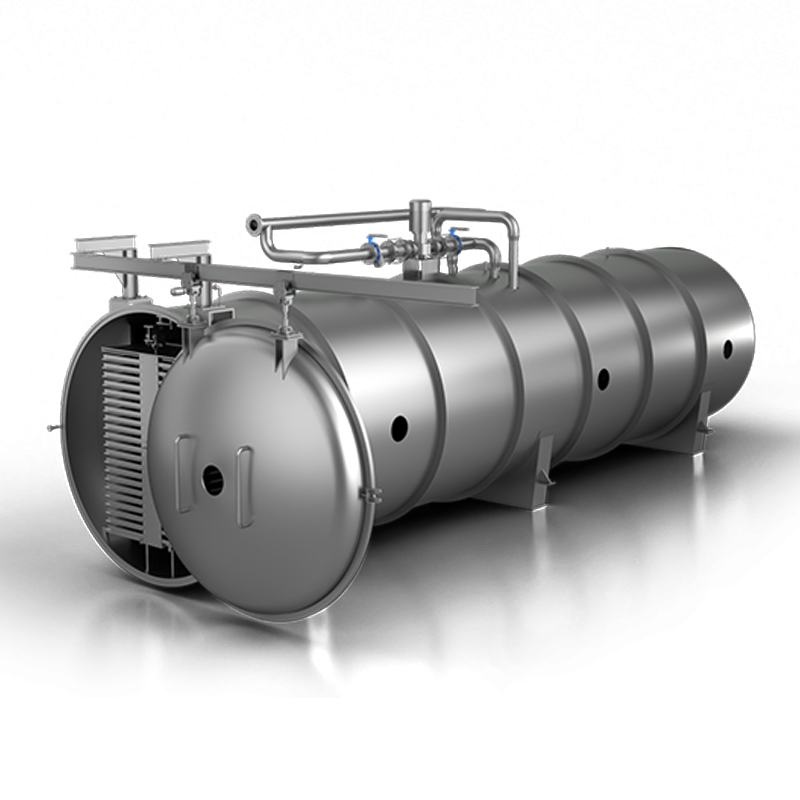
Condenser sizing published for high-moisture loads.Ice capture of 3,000–4,000 kg per batch on the 200 m² BLK-FD-200, with the split condenser and intelligent isolation valve architecture that lets the product chamber and cold trap operate independently.
Integrated pre-freezing and drying in a single unit. The published medium and large-scale design integrates pre-freezing and drying so material completes the full process within the freeze dryer, with pre-engineered dimensions to minimise floor space — and can synchronise with cold storage to hold material at precise sub-zero temperature before loading, preventing partial thawing.
A documented pet food reference. Freeze-dried pet food with crude protein above 65% and palatability verified after rehydration — the highest-margin application category, and one where a supplier's process control has to be demonstrable rather than asserted.
 2026/05/28
 2026/05/28
2026/05/28

 Custom Industrial Lyophilizer Freeze Dryer Manufacturers


 English
 русский
 Español
 Français
 Deutsch
 عربى


