/blog/
News
Products & Solutions
CONTACT US

+86-18068757376

blk@jsblk.com

No. 29 North Tongjiang Road, Xinbei District, Changzhou City, Jiangsu Province, China
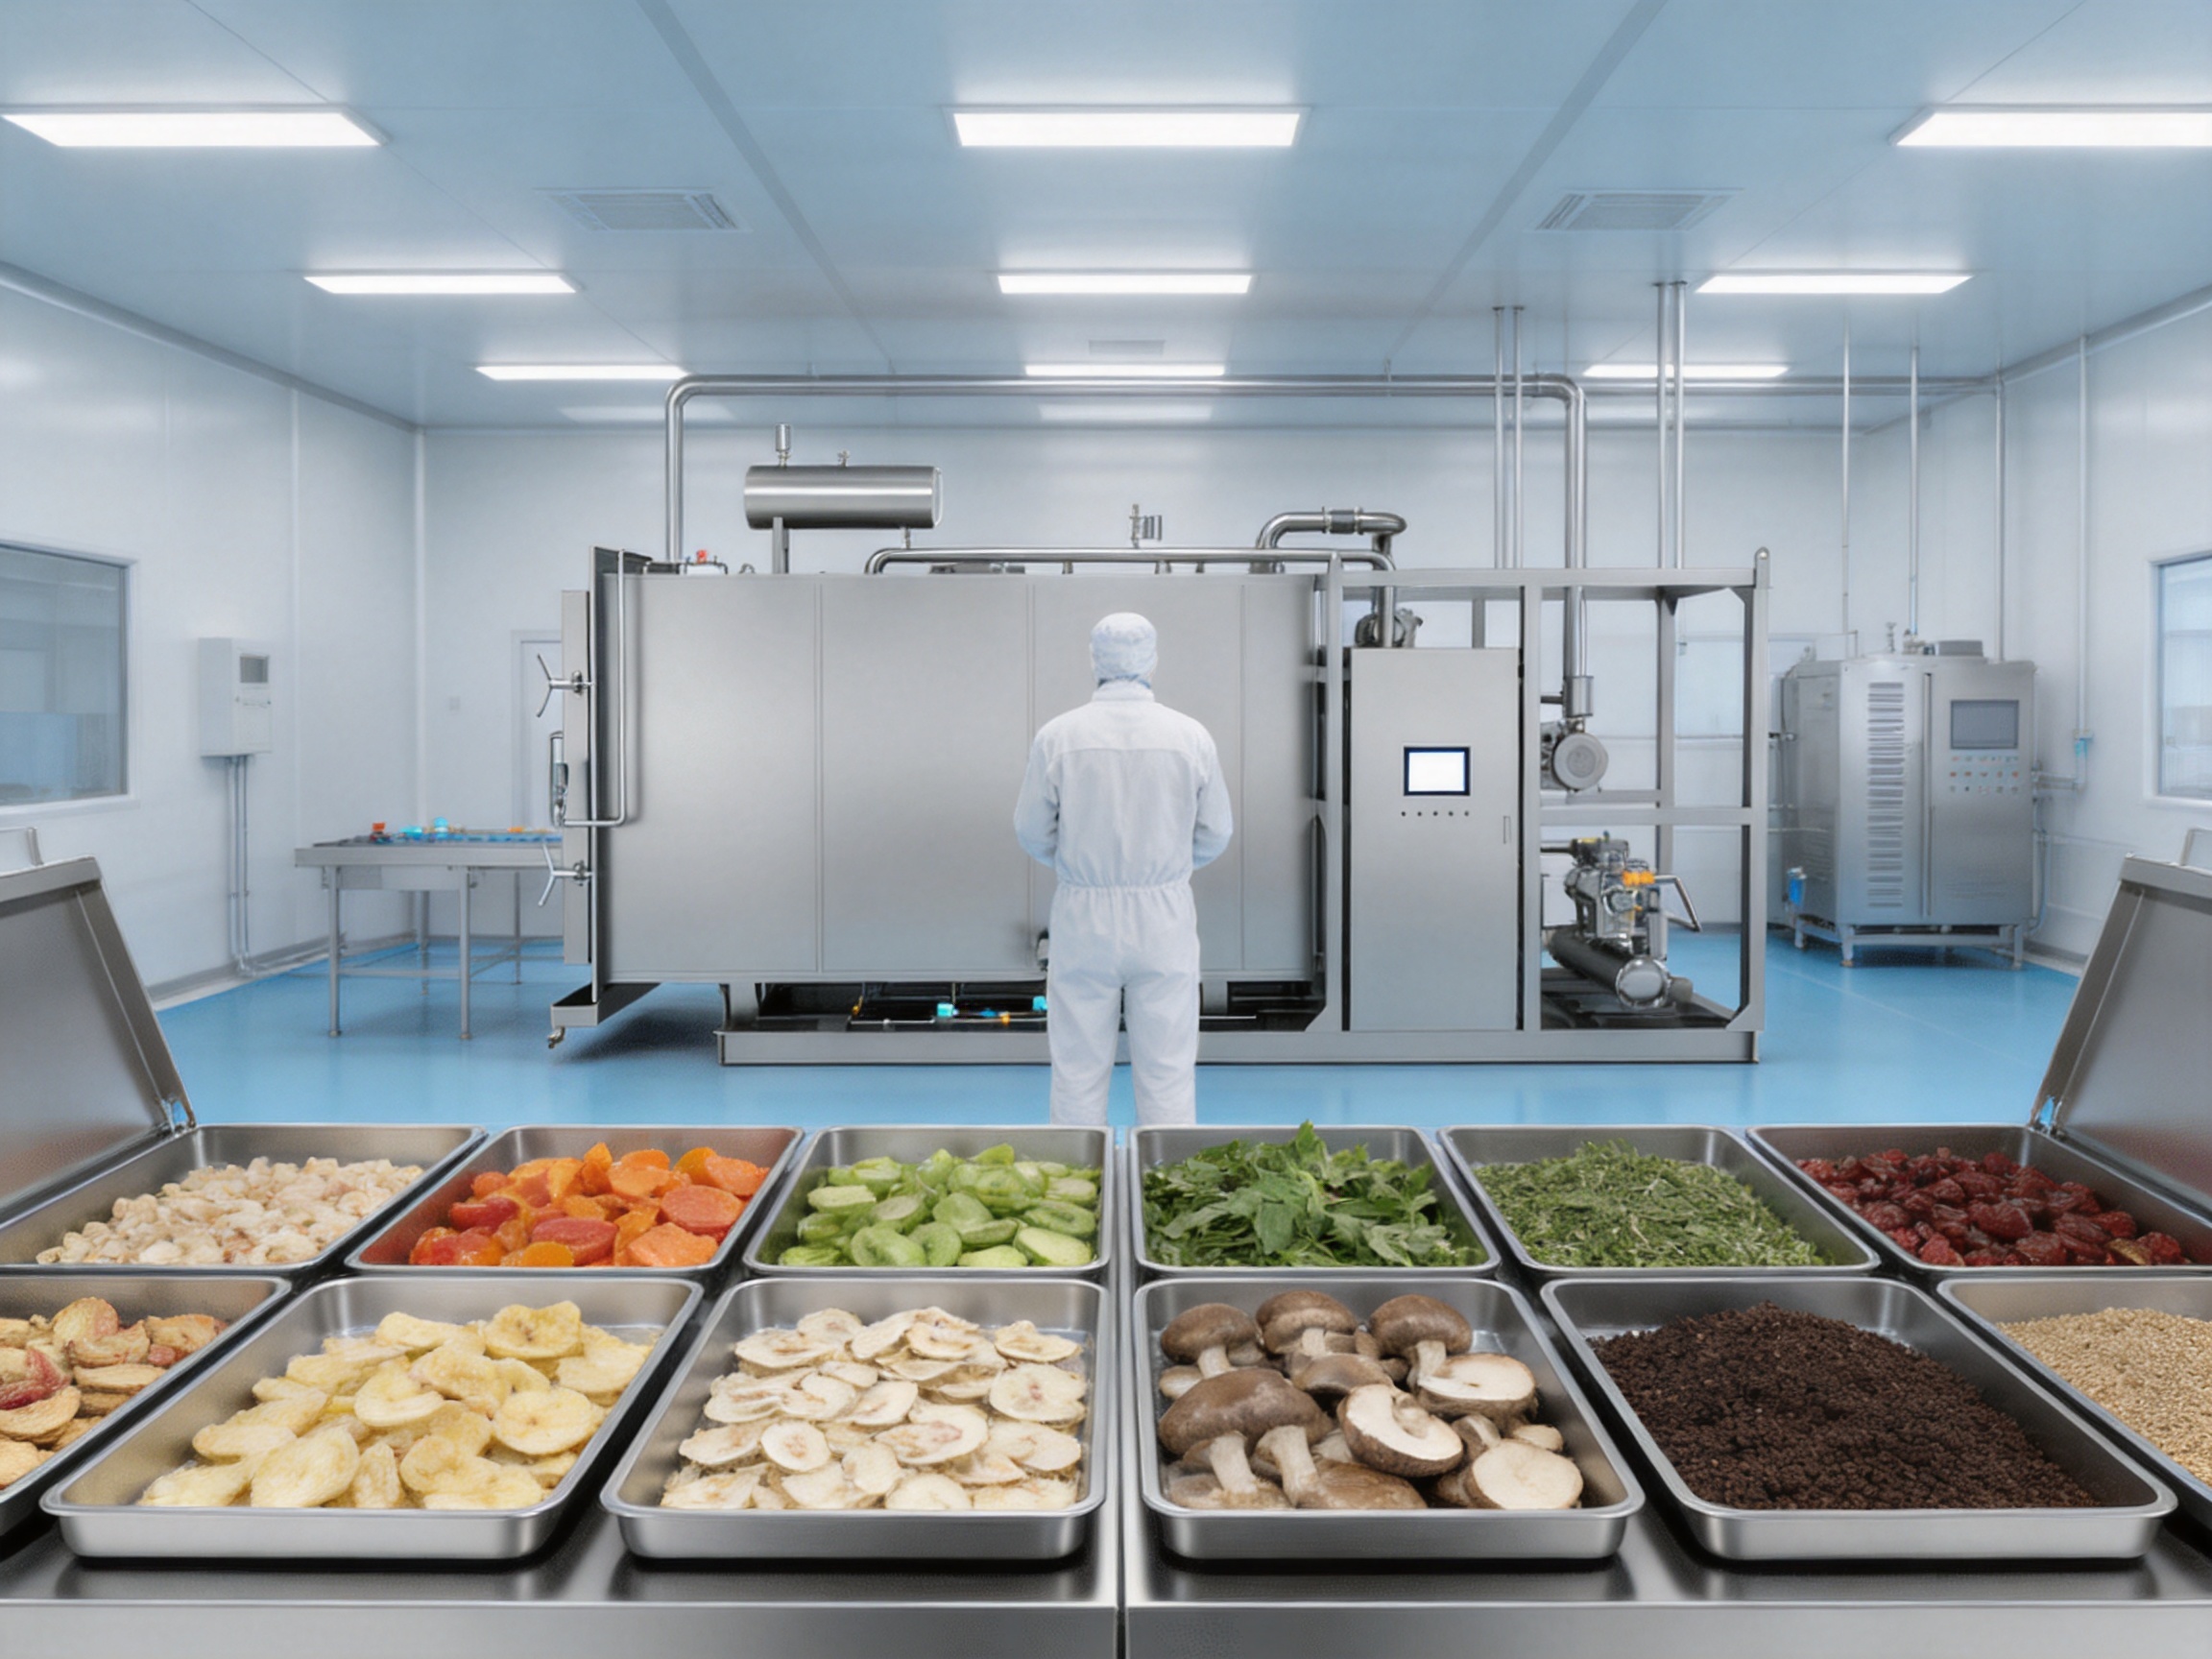
Freeze-drying is one of the most demanding preservation and stabilization technologies used in the food, agricultural, pharmaceutical, biological, chemical, and health-product industries. The process must remove moisture under vacuum while preserving product structure, color, aroma, nutritional value, active ingredients, and rehydration performance. At the same time, industrial users need equipment that is productive, reliable, energy-conscious, easy to install, and adaptable to changing production requirements.
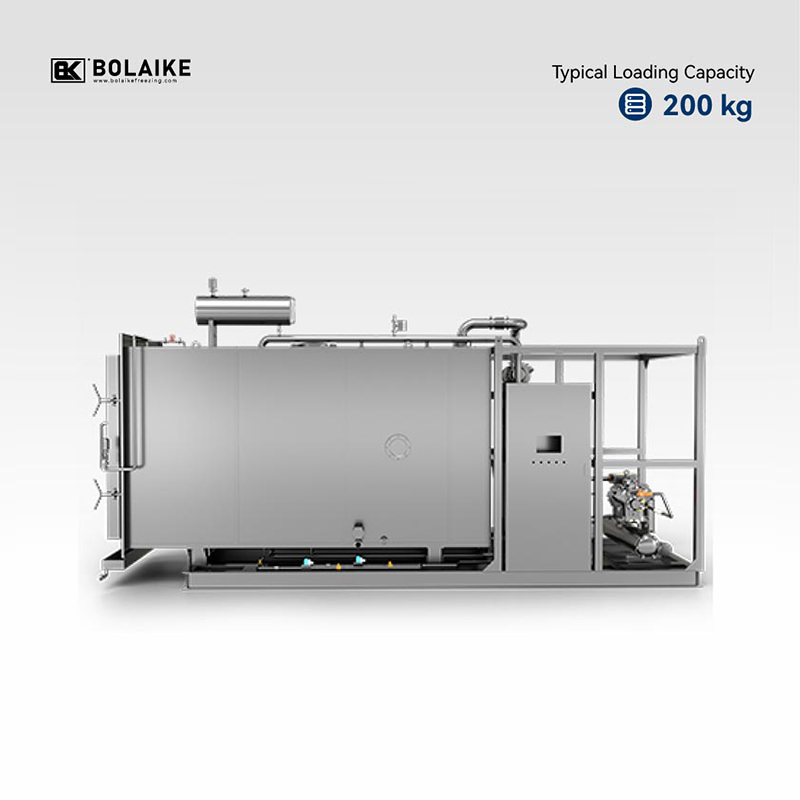
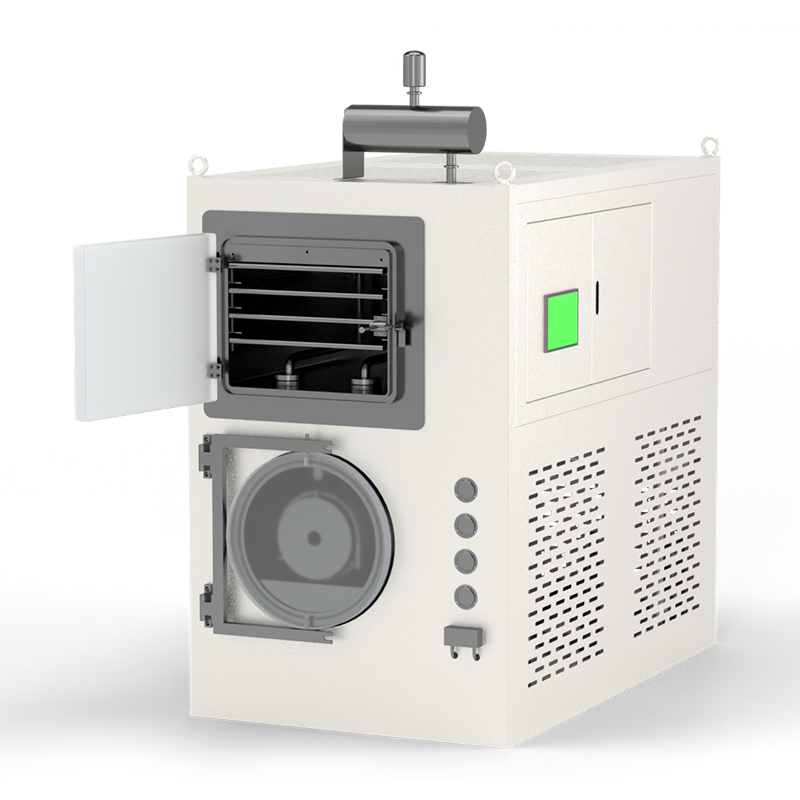
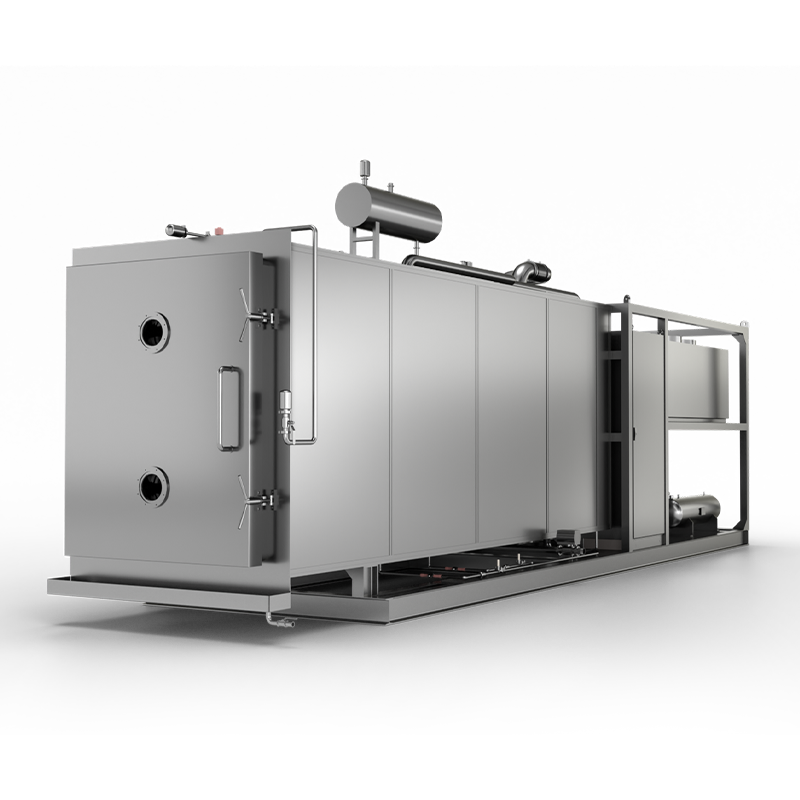
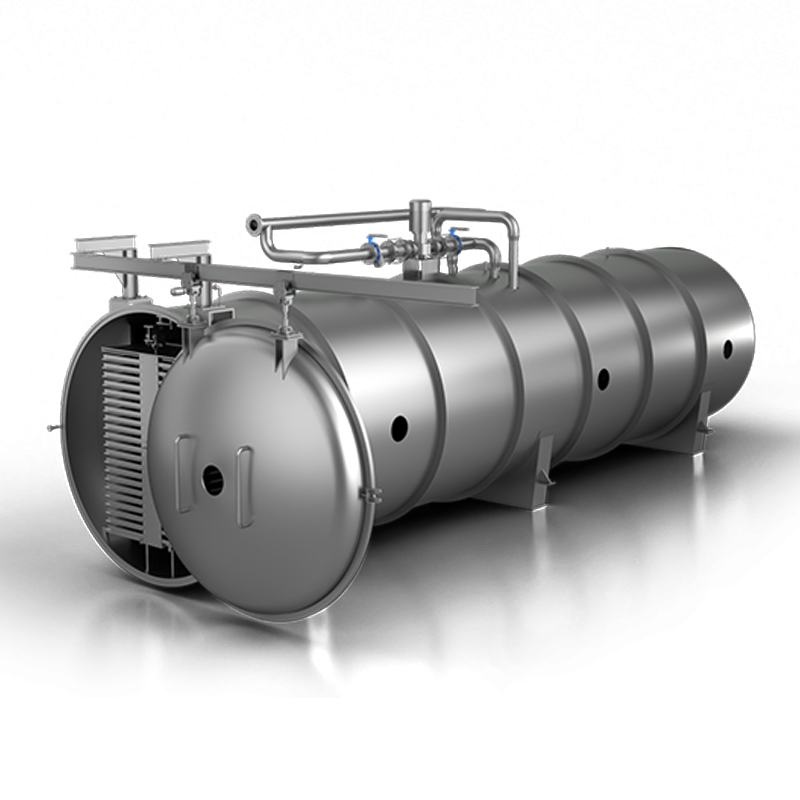
The BLK-FD-20 is a medium-sized pilot-to-production freeze dryer developed for companies that need substantially greater capacity than laboratory or experimental equipment but do not yet require a fully integrated large-scale production line. With a 20-square-meter freeze-drying area, a standard loading capacity of 200 kilograms, and a liquid loading capacity of up to 400 liters, the system provides a practical bridge between product development, pilot manufacturing, and regular commercial production.
Its design combines integrated pre-freezing and drying, a rectangular chamber, double-layer radiant panels, independent cooling and heating circuits, cold-energy recovery, intelligent central control, and flexible dimensional customization. These features allow the machine to address many of the limitations commonly associated with conventional circular-chamber freeze dryers, separate pre-freezing systems, duplicated energy systems, and equipment that is difficult to fit into existing workshops.
More than a single freeze-drying chamber, the BLK-FD-20 is a coordinated processing platform. It is engineered to help manufacturers shorten material transfer steps, improve process consistency, reduce unnecessary energy consumption, use factory space more efficiently, and scale validated recipes toward commercial output.
The BLK-FD-20 occupies an important position between experimental freeze dryers and large-scale industrial systems. Laboratory equipment is useful for formulation studies, process development, and small samples, but it cannot always provide sufficient throughput for market testing or regular batch production. Conversely, a large production line may require significant capital investment, extensive floor space, and a confirmed market demand before it becomes economically suitable.
The BLK-FD-20 provides an intermediate solution for manufacturers that are moving from research and development into commercialization. It can be used to validate production parameters at a meaningful scale, manufacture commercial samples, support seasonal production, and supply niche or premium products without installing a very large line.
Potential users include food processors, fruit and vegetable companies, producers of instant ingredients, suppliers of herbal and medicinal materials, nutraceutical manufacturers, biological product developers, chemical-material processors, and research institutions requiring a higher-throughput development platform. Its flexible format is also useful for contract manufacturers that process different products for multiple customers.
The equipment is particularly suitable where product quality is more important than simple moisture removal. Freeze-dried coffee, fruit pieces, vegetable products, mushrooms, herbs, biological materials, high-value ingredients, and heat-sensitive compounds can all benefit from the low-temperature and vacuum-based drying environment.
The machine is designed around a 20-square-meter freeze-drying area. Under standard operating conditions, the equipment has a loading capacity of approximately 200 kilograms. Its liquid loading capacity is up to 400 liters, although actual capacity depends on product density, filling thickness, tray arrangement, solids content, and the required drying cycle.
Specification |
BLK-FD-20 Value |
Practical Significance |
Freeze-drying area |
20 square meters |
Provides a substantial working area for pilot-to-production batches |
Standard loading capacity |
200 kilograms |
Supports commercial sampling and regular medium-scale production |
Liquid loading capacity |
400 liters |
Suitable for liquid formulations and slurry-based products |
Overall dimensions |
6,000 × 2,200 × 3,000 millimeters |
Designed for efficient workshop planning |
Overall weight |
Approximately 10.5 tons |
Reflects a robust industrial construction |
Ultimate vacuum level |
10 pascals or lower |
Creates the low-pressure environment required for sublimation drying |
These figures should be considered equipment reference values rather than a guarantee of identical output for every material. Freeze-drying capacity varies according to initial moisture, product thickness, freezing characteristics, target residual moisture, loading pattern, and the thermal behavior of the formulation. A technical evaluation and sample test are recommended before final production planning.
One of the most important advantages of the BLK-FD-20 is its integrated process architecture. In conventional layouts, materials may be frozen in a separate cold room or freezer before being transferred to the vacuum drying chamber. This arrangement can create additional handling requirements, consume more floor space, and expose the product to temperature fluctuations during transfer.
The integrated design allows materials to complete pre-freezing and drying within the same freeze-dryer system. This reduces the number of independent process steps and helps maintain a controlled thermal environment from freezing through primary and secondary drying. Fewer transfers can also lower the risk of contamination, product damage, and loading errors.
For food and agricultural products, reduced handling may help preserve the physical appearance of delicate pieces. For biological or pharmaceutical materials, the integrated configuration can support better control of process continuity. For manufacturers with limited factory space, it eliminates or reduces the need for a separate pre-freezing installation.
The integrated design also supports more direct automation. A centralized control system can coordinate freezing, vacuum operation, shelf temperature, drying stages, and equipment status. This approach gives operators a clearer view of the complete cycle instead of requiring them to manage several disconnected systems.
In addition, a combined freezing and drying system can reduce duplicated infrastructure. Separate systems may each require independent refrigeration circuits, controls, pumps, insulation, and service access. By sharing key thermal and control resources, the BLK-FD-20 is designed to reduce system complexity and improve the efficiency of the overall process.
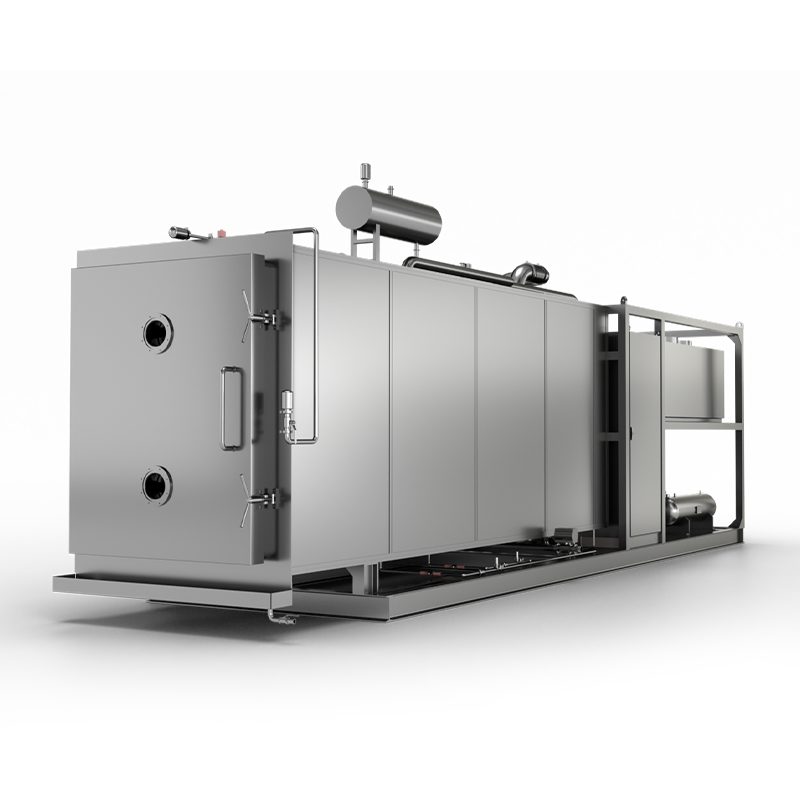
Many traditional freeze dryers use circular chambers because cylindrical pressure vessels are structurally efficient. However, chamber geometry also affects tray arrangement, usable space, floor planning, and the relationship between the chamber and radiant shelves. For medium-sized and small-scale systems, a rectangular chamber can provide practical advantages in manufacturing environments.
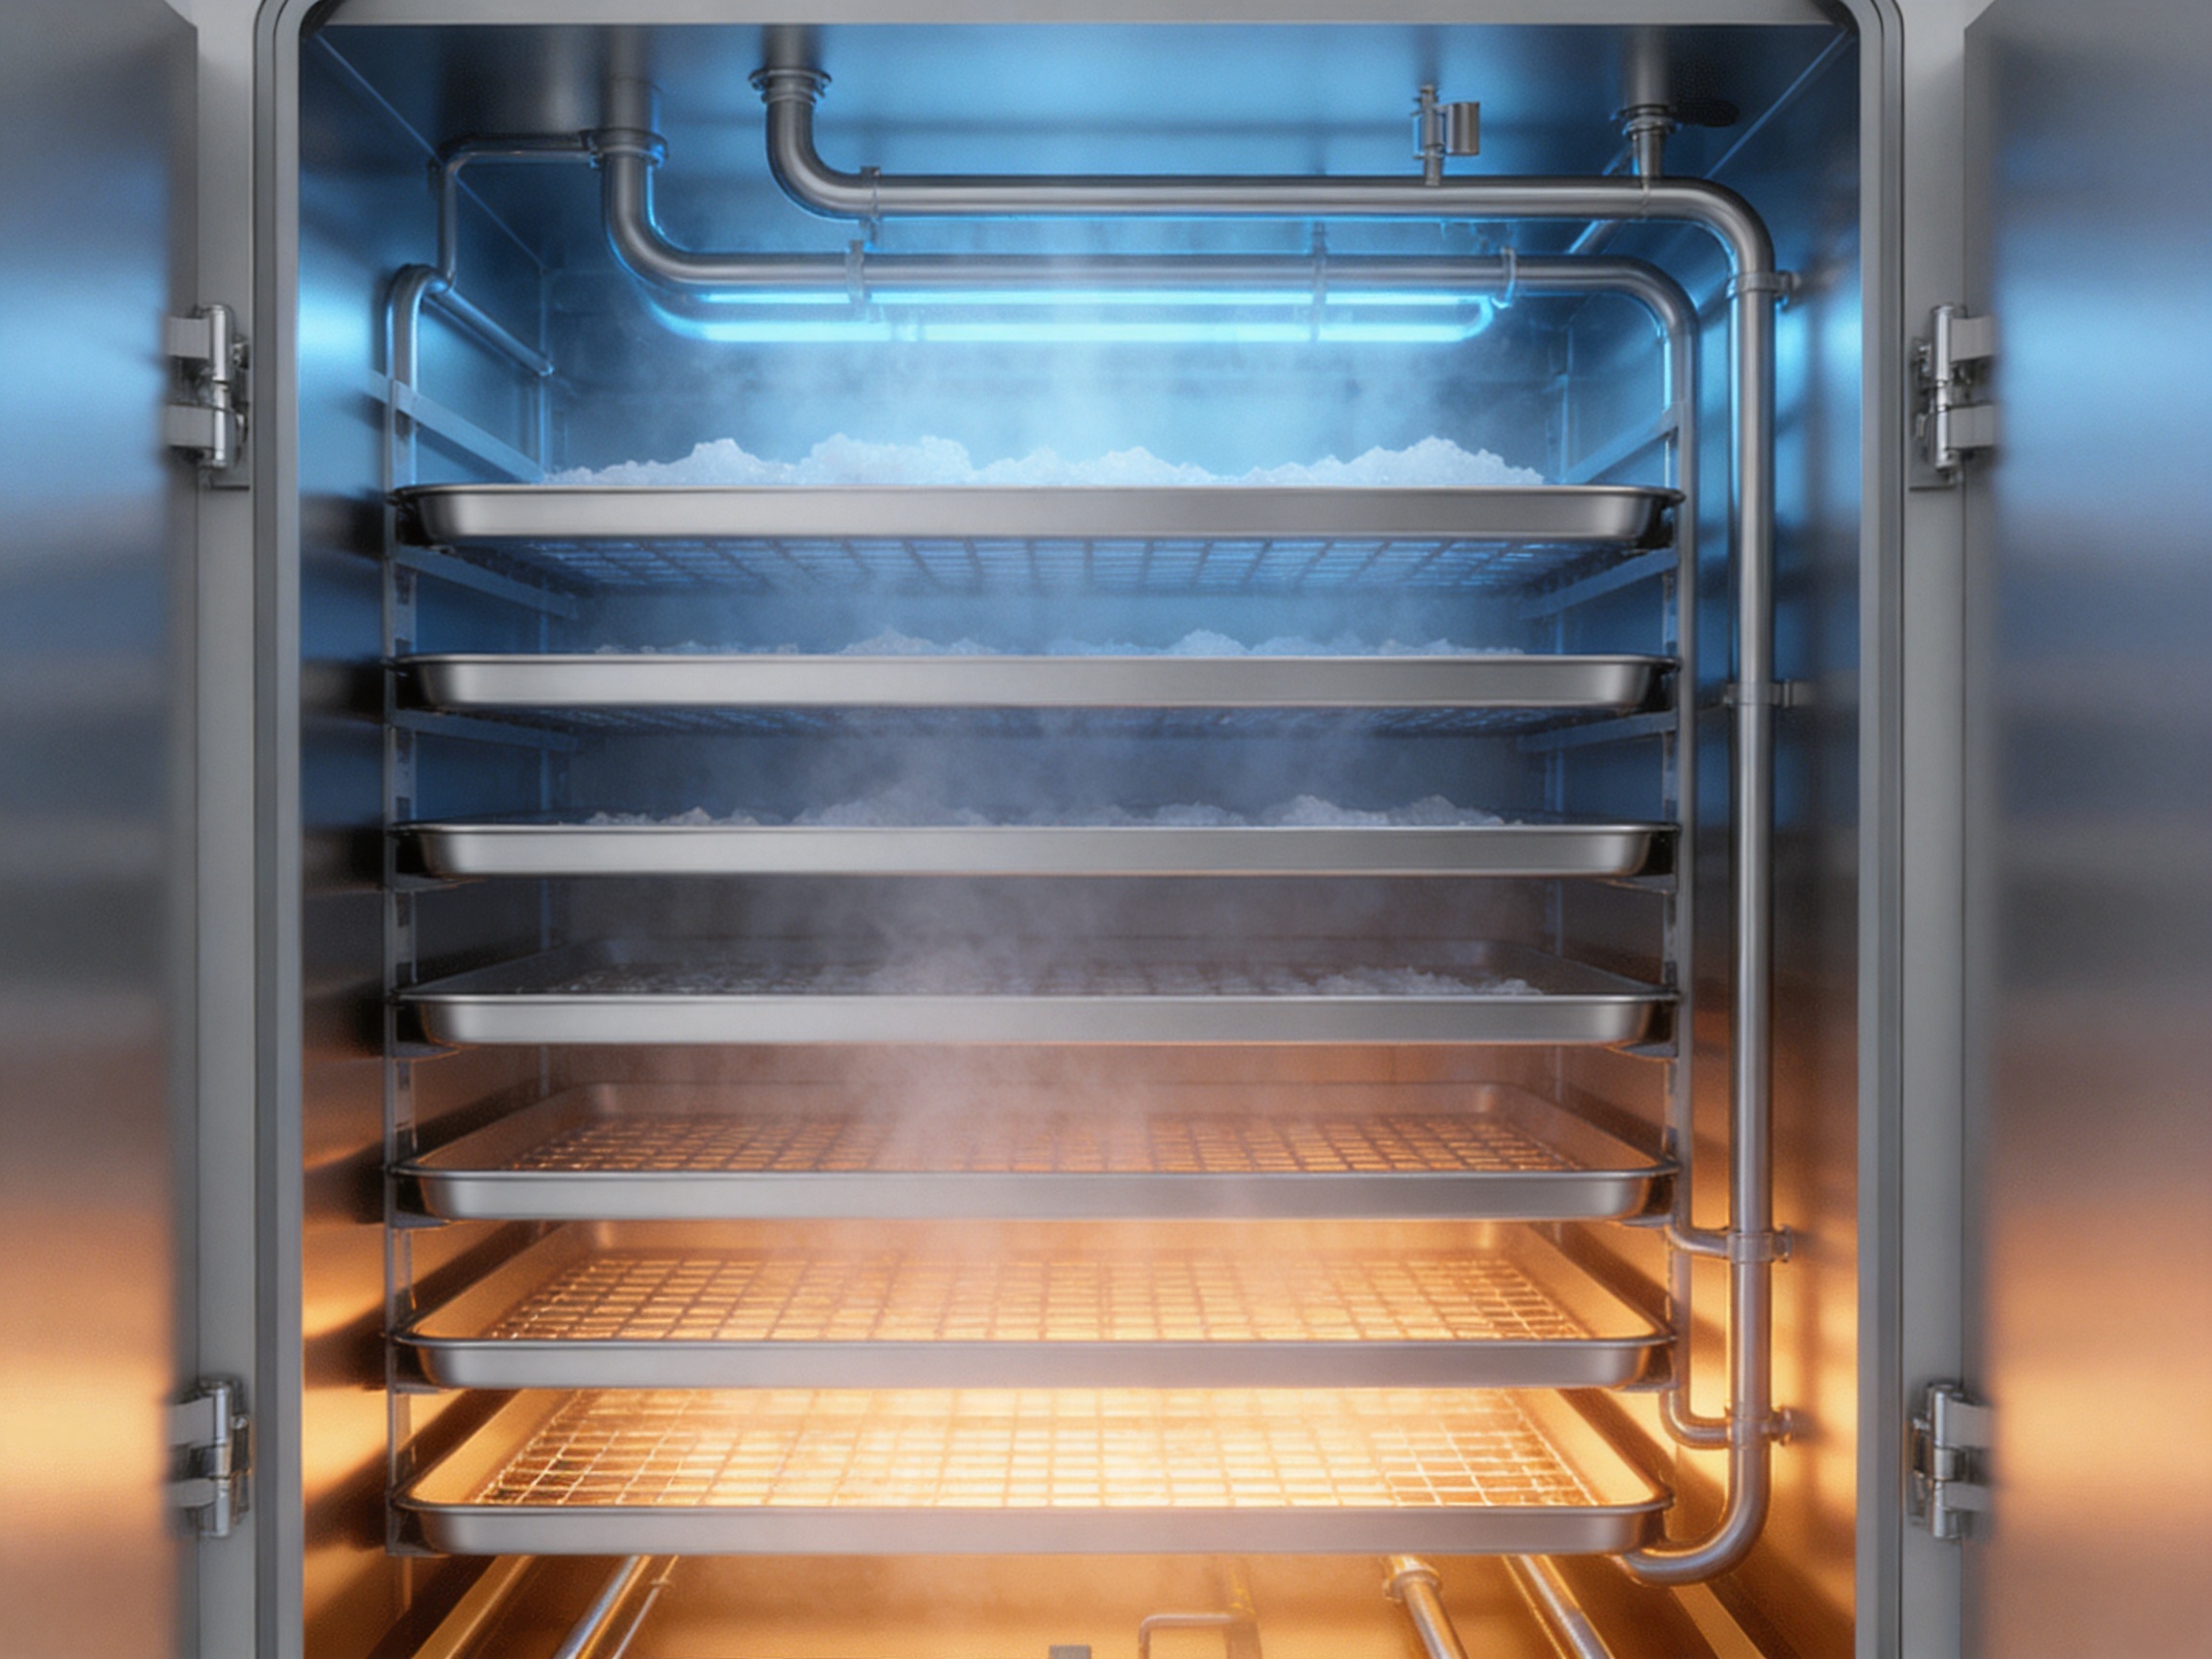
The BLK-FD-20 uses a rectangular chamber structure intended to make better use of workshop space. A rectangular body can align more naturally with walls, service corridors, loading areas, and adjacent equipment. This can simplify factory layout and reduce unused areas that may occur around circular equipment.
For the same nominal freeze-drying area, a square or rectangular chamber can require a smaller footprint than a circular chamber. This is especially valuable in facilities that are expanding within an existing building rather than constructing a new plant. Efficient use of space may reduce renovation work, simplify utility routing, and leave more room for material preparation and packaging.
The chamber shape also works effectively with rectangular trays and radiant panels. When the shelves, trays, and chamber walls follow compatible dimensions, fewer gaps are created between processing surfaces. This increases the effective utilization of the internal volume and supports a more organized loading pattern.
Air movement and temperature distribution are also important considerations. The rectangular chamber is designed to provide stable internal conditions when paired with appropriately arranged radiant panels and controlled vacuum operation. Stable heat transfer can help reduce differences between product positions and support more consistent drying quality across the batch.
Compared with a circular chamber of similar capacity, the rectangular arrangement may also reduce the refrigeration and vacuum-pump power required for a given loading target, depending on the process configuration. The actual energy benefit depends on product and operating conditions, but the chamber concept is intended to improve overall system efficiency rather than optimize only one isolated component.
The standard overall dimensions of the BLK-FD-20 are approximately 6,000 millimeters in length, 2,200 millimeters in width, and 3,000 millimeters in height. However, length, width, and height can be customized according to workshop conditions and project requirements.
Dimensional customization can help address doorway limitations, ceiling height restrictions, production-flow requirements, and the position of existing utilities. A customized configuration may also support better separation between raw-material handling, freeze-drying, unloading, and packaging areas.
Once the unit has been assembled and placed in position, the basic site connection requirements are water and electricity. This simplifies installation compared with projects that involve extensive on-site assembly of multiple independent systems. Final utilities, foundation requirements, drainage, ventilation, electrical ratings, and clean-room conditions should be confirmed during engineering design.
BLK-FD-20
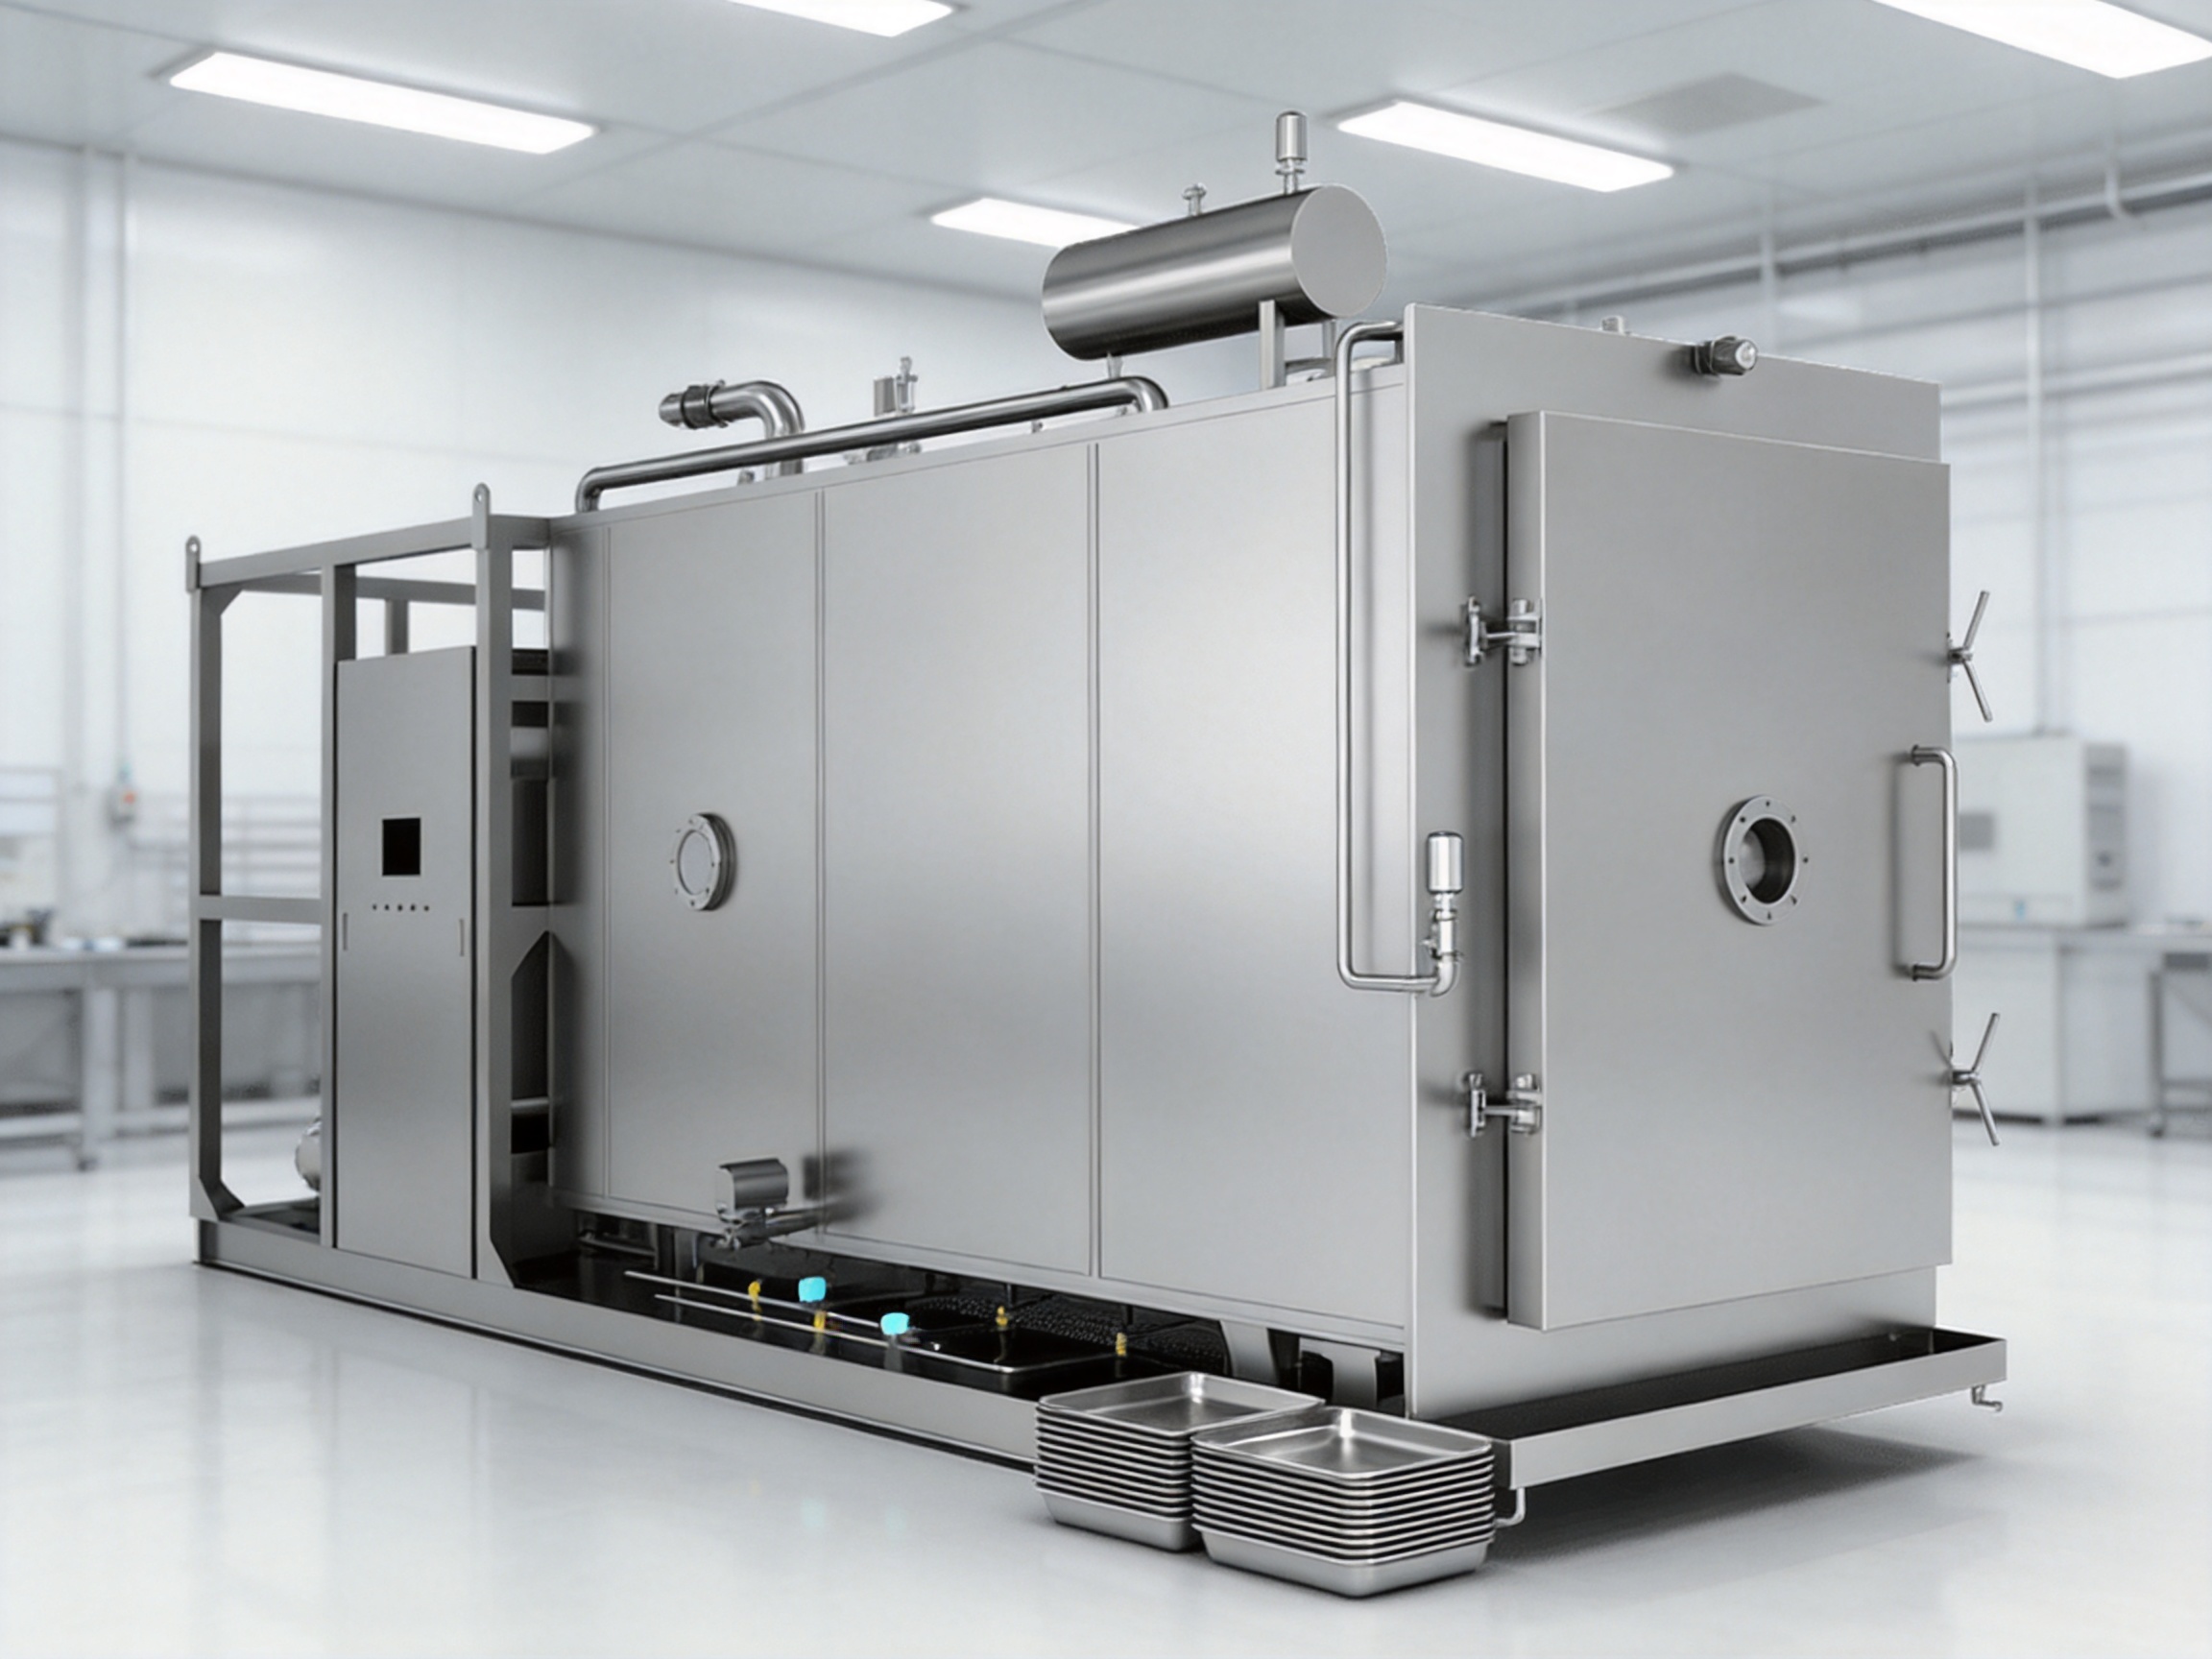
Heat transfer is central to freeze-drying performance. During primary drying, energy must be supplied carefully so that ice sublimates at a controlled rate without causing collapse, melting, excessive shrinkage, or other quality defects. During freezing, the system must remove heat efficiently and create a suitable ice structure. A radiant-panel design that supports both functions can improve process coordination.
The BLK-FD-20 uses patented double-layer radiant panels with independent upper and lower circuits. The upper layer functions as the cooling circuit, while the lower layer functions as the heating circuit. This arrangement allows the same panel structure to support both low-temperature freezing and controlled drying operations.
Independent circuits provide greater separation between cooling and heating functions. Rather than relying on a single surface to switch between different thermal duties without dedicated internal pathways, the double-layer structure is designed to improve heat-transfer control and temperature uniformity. It can also reduce the thermal delay associated with changing between freezing and drying stages.
The geometry of the radiant panels is matched to the rectangular chamber and tray arrangement. This helps distribute thermal energy across the loading area and supports more even shelf temperatures. Uniform shelf temperature is important because temperature differences can result in different sublimation rates, variable residual moisture, and inconsistent product structure within the same batch.
For products with strict appearance and texture requirements, more uniform heat transfer can reduce the need for excessive safety margins. Operators can develop drying cycles that are sufficiently efficient while maintaining product quality. Better temperature control can also make process validation more repeatable from one batch to the next.
The panel technology is supported by patent registrations associated with radiant-panel and double-radiant-panel structures, including CN209030727U and CN204392676U. Patent references indicate the technical protection of the design, while actual process performance still depends on product formulation, loading practice, control settings, and maintenance conditions.
Energy consumption is one of the largest operating costs in freeze-drying. Refrigeration, vacuum generation, shelf heating, cooling-water circulation, and auxiliary systems all contribute to the total energy requirement. Because freeze-drying cycles can be long, even moderate efficiency improvements can produce meaningful savings over the equipment lifetime.
The BLK-FD-20 incorporates several energy-saving concepts instead of relying on one isolated improvement. These include integrated freezing and drying, cold-energy recovery, heat recovery options, a shared refrigeration structure, and a heat-pump and economizer system.
The standard configuration includes a residual cold recovery system. In a conventional arrangement, cold energy may be used once and then discharged. The compressor must then operate continuously at a relatively high load to provide the next required cooling step. A recovery system can capture and reuse available cold energy for pre-cooling or for the next refrigeration stage.
According to the supplied technical information, the standard cold recovery system can reduce energy consumption by approximately 10 to 15 percent compared with traditional equipment under comparable operating conditions. The broader system description also indicates that recycling cold energy can reduce overall compressor load by approximately 20 to 30 percent. These figures describe different performance indicators and should not be added together. Actual savings depend on batch scheduling, product temperature, ambient conditions, cycle design, and operating discipline.
Reusing cold energy can reduce unnecessary thermal losses and help the refrigeration system operate more efficiently. It may also improve the transition between process stages by making cooling resources available with less delay.
Freeze-drying processes can generate recoverable heat during sublimation and heating stages. In many conventional systems, this heat is discharged even though another part of the process may require thermal energy. The BLK-FD-20 can be configured with a heat recovery system that recycles waste heat or steam heat for material drying.
Heat recovery is identified as a customization option rather than a universal standard configuration. This distinction is important because the appropriate system depends on the product, required shelf temperature, facility utilities, process sequence, and local energy infrastructure.
The supplied information indicates that when the material heating temperature is no higher than 35 degrees Celsius, the recovered-energy structure may provide very high energy savings under suitable conditions. It also indicates that when the required heating temperature is below 80 degrees Celsius, approximately 10 percent of energy consumption may be saved through waste-heat enhancement. These values should be verified through application-specific testing and engineering calculations.
Traditional layouts may use separate energy systems for cold storage and freeze-drying chambers. Such duplication can increase equipment cost, maintenance requirements, and energy losses. The integrated energy structure of the BLK-FD-20 allows cooling and drying processes to share a refrigeration circuit where appropriate.
Sharing a refrigeration circuit can reduce repeated components and improve resource utilization. It may also simplify the control strategy because the central system can coordinate thermal demand across the integrated process rather than treating every stage as an independent installation.
The integrated energy structure is associated with patent CN205784249U. As with all equipment advantages, the resulting energy performance depends on how the equipment is configured, loaded, operated, and maintained.
The optional heat-pump and economizer system is designed to increase compressor coefficient of performance. The supplied material states that the system can raise compressor COP to approximately 4.8 to 5.9, improving energy efficiency compared with traditional freeze-drying equipment.
A higher COP means that more useful thermal output can be obtained for each unit of electrical energy consumed under the relevant operating conditions. This can lower operating costs, particularly for facilities running frequent or long production cycles. The heat-pump and economizer system is associated with patent CN209612254U.
For customers comparing equipment, it is important to assess energy consumption using complete-cycle data rather than a single rated value. A meaningful comparison should include freezing, primary drying, secondary drying, defrosting, vacuum pumping, refrigeration, heating, and standby conditions.
The 20-square-meter shelf area provides a practical platform for processing materials with different bulk densities. The standard capacity is approximately 200 kilograms, while the liquid loading capacity can reach approximately 400 liters. However, the actual batch quantity varies according to the physical properties of the material.
Loading height, product density, moisture content, tray thickness, particle size, and desired final moisture all influence throughput. A low-density fruit product may occupy a different volume and produce a different drying load than a dense food slurry or medicinal extract. For this reason, the equipment should be selected according to both mass and volume requirements.
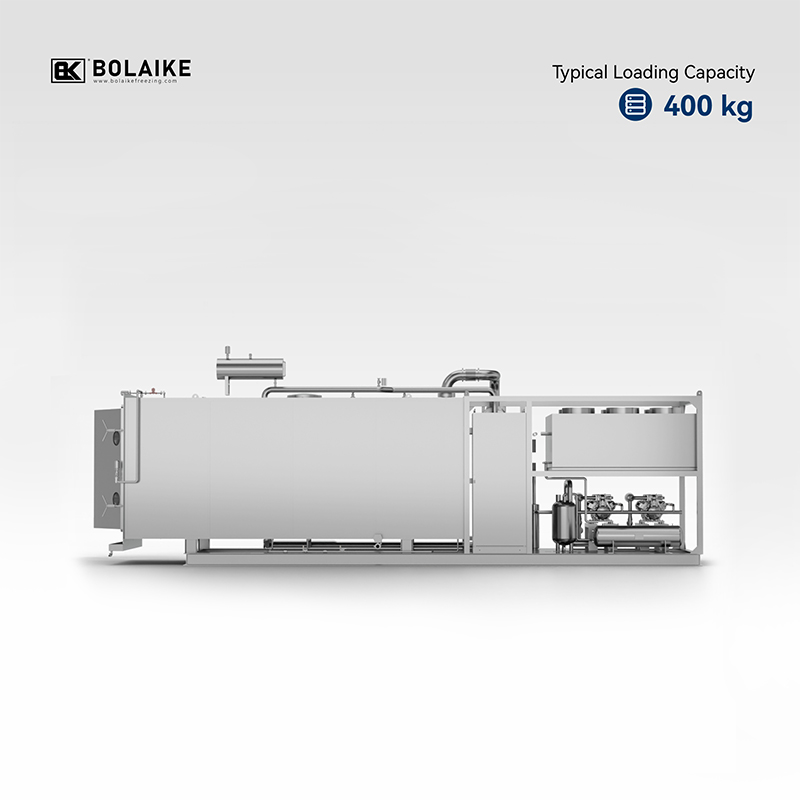
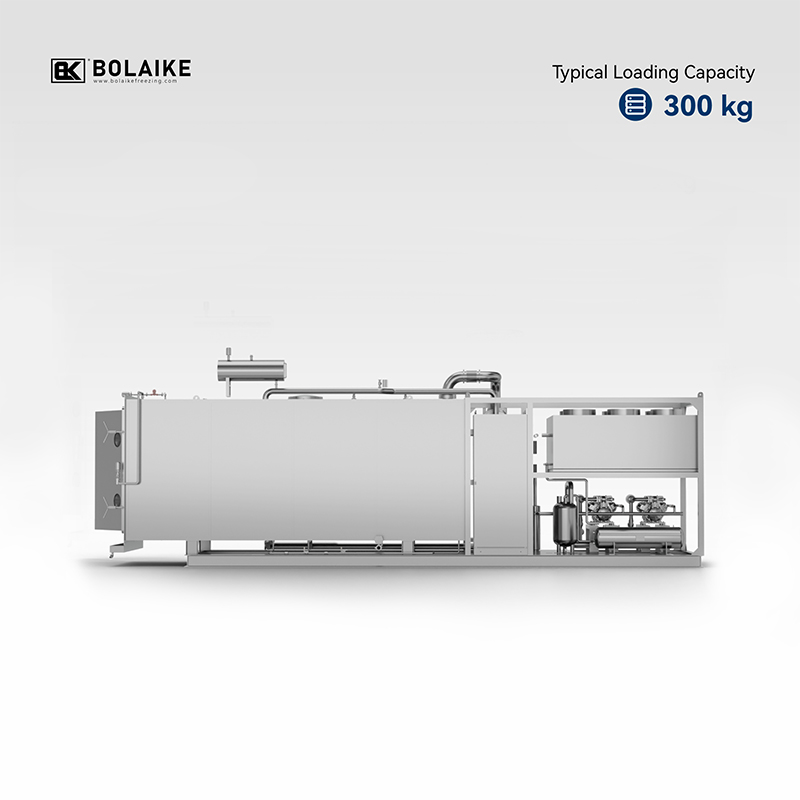
The supplied capacity model indicates that the per-chamber material processing capacity varies by category and material density. Food materials may be processed in a range of approximately 300 to 400 kilograms under one reference classification, while solution-based materials may fall in a range of approximately 200 to 300 kilograms, and fruits and vegetables may be in a range of approximately 150 to 200 kilograms. These figures are reference ranges and must be adjusted through material testing.
For product developers, this flexibility is valuable because one machine can support different product families. A facility may use the equipment for fruit pieces during one season, vegetable products during another, and high-value extracts or formulated materials for the remainder of the year. With proper cleaning and process management, the equipment can support a diversified production strategy.
Flexible production also reduces dependence on a single product. If market demand changes, the manufacturer can use the same freeze dryer for new formulations or contract-processing projects. This can improve asset utilization and shorten the payback period for the equipment investment.
Freeze-drying quality is determined by more than the final moisture level. Customers may evaluate color, shape, aroma, taste, texture, porosity, rehydration speed, nutrient retention, active-component stability, and shelf life. A suitable freeze dryer must therefore provide stable process conditions throughout the batch.
The BLK-FD-20 supports quality consistency through controlled freezing, uniform shelf temperatures, low ultimate vacuum pressure, integrated process stages, and centralized monitoring. Its ultimate vacuum level is specified at 10 pascals or lower, creating the low-pressure environment required to promote sublimation rather than conventional liquid evaporation.
Controlled freezing is particularly important because ice-crystal size influences the structure of the dried product. Freezing conditions affect pore size, mechanical strength, drying resistance, and rehydration behavior. By integrating pre-freezing and drying, the equipment can help reduce uncontrolled changes between the freezing and drying stages.
Uniform radiant-panel performance helps reduce hot and cold spots. If one region of the chamber receives more heat than another, the warmer product may dry too quickly while colder product remains under-dried. Independent cooling and heating circuits are intended to support more consistent thermal behavior across the shelves.
Quality assurance still requires product-specific development. Operators must establish suitable freezing temperatures, shelf-temperature ramps, vacuum settings, primary-drying endpoints, secondary-drying conditions, and unloading procedures. The equipment provides the controlled environment, but successful process development depends on disciplined testing and documentation.
Modern freeze-drying requires accurate coordination among refrigeration, vacuum, heating, cooling, sensors, valves, pumps, and safety systems. Manual operation of each subsystem can increase operator workload and create the possibility of inconsistent settings. The BLK-FD-20 uses an intelligent central control system to manage connected equipment and coordinate the production sequence.
The central control system can monitor operational status across the equipment. Depending on the selected configuration, it can manage process stages, temperature targets, vacuum conditions, timing, alarms, and equipment interlocks. A unified interface helps operators understand the current state of the cycle and respond more quickly to abnormal conditions.
Remote monitoring through a mobile application is supported. Remote access can help production managers review equipment status, receive alerts, and supervise operations without remaining beside the machine throughout the entire cycle. This is especially useful for long freeze-drying programs and facilities with multiple production areas.
Multiple language options are available for customization. A multilingual interface can simplify training for international operators and reduce the risk of misunderstanding important process or safety instructions.
Central control also supports data-based process improvement. Historical records can be reviewed to compare batch performance, identify deviations, evaluate energy consumption, and refine recipes. In industries where traceability is important, digital records can contribute to production documentation and quality management.
Industrial freeze dryers must manage low pressure, very low temperatures, heated surfaces, refrigerant systems, electrical equipment, and heavy access doors or trays. Safety functions should therefore be integrated into the control architecture and mechanical design.
The BLK-FD-20 is designed according to international equipment specifications and is described as compliant with European CE mechanical health and safety standards. It is also supported by China quality management system certification. Certification and compliance provide an important foundation, but safe operation additionally requires proper installation, operator training, preventive maintenance, and adherence to site procedures.
Safety interlocks, alarm management, vacuum protection, thermal monitoring, electrical protection, and emergency procedures should be reviewed with the supplier during technical acceptance. Customers should also confirm the standards applicable in their own country before purchasing and commissioning the equipment.
The equipment is manufactured by Jiangsu Bolaike Freezing Technology Development Co., Ltd., a Chinese high-technology enterprise specializing in vacuum freeze-drying and refrigeration equipment. The company was established in 2014 in Changzhou, Jiangsu, and developed from a refrigeration business that entered the industry in 2003.
This background is significant because freeze-drying equipment depends on the integration of refrigeration engineering, vacuum technology, thermal design, automation, pressure-vessel construction, mechanical fabrication, and process application knowledge. A supplier that understands only one of these fields may struggle to optimize the complete system. A company with long-term refrigeration experience can approach the freeze dryer as an integrated thermal and mechanical platform.
The company operates professional teams covering research and development, engineering, sales, installation, commissioning, and after-sales service. This integrated structure can provide advantages over suppliers that outsource most of the technical work to unrelated contractors.
Its manufacturing base covers approximately 24,000 square meters. A modern manufacturing facility provides space for component fabrication, assembly, inspection, testing, control integration, and pre-delivery verification. For large or heavy equipment, the ability to assemble and inspect systems in a controlled factory environment can reduce the amount of corrective work required at the customer site.
The company has obtained more than 100 national invention and utility model patents. These patents cover areas associated with freeze-drying structures, energy recovery, radiant panels, heat pumps, and related systems. A substantial patent portfolio indicates ongoing investment in technical development and provides evidence that the supplier is building proprietary solutions rather than relying exclusively on standard imported components.
The company also maintains partnerships with universities and research institutions, including agricultural and food-science organizations. Cooperation with universities can support material testing, process research, thermal analysis, and the development of new applications. This is valuable for customers whose products require customized cycles rather than standard operating recipes.
Equipment quality is affected by the complete project process, not only by the final machine. Engineering begins with understanding the product, required throughput, loading method, facility layout, utility conditions, and quality objectives. The design team can then determine the appropriate chamber dimensions, panel arrangement, refrigeration configuration, control functions, and optional recovery systems.
Factory assembly allows the main equipment to be built and checked before shipment. Pre-engineered assembly can reduce on-site connection work and support a faster transition from delivery to operation. After installation, commissioning is required to verify vacuum performance, refrigeration behavior, shelf-temperature uniformity, control communication, alarm functions, and process operation.
After-sales support is equally important because freeze-drying is a long-term production process. Service personnel may support installation, commissioning, operator training, troubleshooting, maintenance planning, and process optimization. A supplier with in-house engineering and service capabilities is better positioned to maintain continuity between the original design and later technical support.
When comparing the BLK-FD-20 with conventional medium-sized freeze dryers, several differences deserve attention. The first is the integration of freezing and drying. Equipment that requires separate pre-freezing may involve additional transfer equipment, greater floor-space requirements, and more handling exposure. The integrated BLK-FD-20 reduces these complications.
The second difference is chamber geometry. A circular chamber can be mechanically strong, but it may not use workshop space or tray area as efficiently as a rectangular chamber. The BLK-FD-20 is designed around a rectangular layout that supports practical installation and better alignment with radiant panels and trays.
The third difference is the double-layer radiant-panel system. Conventional equipment may use a single circuit or a less specialized panel structure. The independent cooling and heating circuits of the BLK-FD-20 are intended to improve thermal control, reduce transition losses, and promote more uniform shelf temperatures.
The fourth difference is energy recovery. Traditional systems may discharge usable cold or heat. The BLK-FD-20 includes standard cold recovery and offers heat recovery as a customization option. This allows users to select a configuration according to their product, operating schedule, and energy strategy.
The fifth difference is the level of control. A central intelligent control system, remote monitoring, and multilingual options can provide a more accessible operating experience than equipment with fragmented controls or limited data visibility.
The sixth difference is customization. The ability to adjust the length, width, and height helps the equipment fit more effectively into existing factories. Many standardized machines force customers to modify buildings or accept inefficient layouts. Dimensional flexibility can reduce these constraints.
Finally, the BLK-FD-20 is supported by a supplier with expertise across research, refrigeration, manufacturing, installation, commissioning, and after-sales service. This complete capability can reduce the risk of communication gaps between equipment design and project execution.
Freeze-dried foods retain much of their original shape, flavor, and nutritional value while achieving a long shelf life after suitable packaging. The BLK-FD-20 can support fruit pieces, vegetables, mushrooms, herbs, prepared meals, ingredients, dairy-based products, and other heat-sensitive foods.
Its liquid loading capacity also makes it suitable for liquid or semi-liquid formulations that are spread onto trays before freezing. Products such as coffee extracts, beverage ingredients, sauces, purees, and nutritional mixtures may be processed after appropriate recipe development.
Fruits and vegetables often require careful control to maintain color, structure, and aroma. The controlled freezing and drying environment can help preserve the open cellular structure needed for rapid rehydration. The rectangular chamber and tray system can also support systematic arrangement of individual pieces or thin layers.
Herbs, botanical materials, extracts, and health supplements may contain heat-sensitive components. Vacuum freeze-drying lowers the product temperature during moisture removal compared with many conventional hot-air processes. The process can therefore be considered where preservation of volatile compounds, appearance, and biological activity is important.
Biological materials can be sensitive to temperature, oxygen, and moisture. Freeze-drying may help stabilize selected biological products when combined with appropriate formulation and sterile or controlled processing practices. The equipment should be configured according to the required cleanliness, containment, and validation standards.
Some chemical materials and specialty formulations benefit from controlled sublimation because it can produce a porous, easily reconstituted, or more stable final structure. The appropriate chamber materials, sealing systems, and process controls should be selected according to chemical compatibility and safety requirements.
A freeze dryer should be evaluated as part of a complete production system. Before installation, the customer should confirm floor loading, access routes, ceiling clearance, electrical capacity, cooling-water conditions, drainage, ventilation, vacuum exhaust, environmental temperature, and available service space.
Because the BLK-FD-20 weighs approximately 10.5 tons, foundation and structural requirements must be reviewed by qualified engineering personnel. Transport and lifting plans should account for the equipment dimensions and the route from unloading to the final production area.
Operators should receive training in material preparation, tray loading, freezing, vacuum operation, cycle selection, alarm response, cleaning, defrosting, and batch documentation. Overloading trays or creating uneven product layers can reduce drying consistency even when the machine is operating correctly.
Routine maintenance should include inspection of refrigeration components, vacuum pumps, seals, valves, sensors, electrical cabinets, control interfaces, and safety devices. Door gaskets and chamber seals deserve particular attention because small leaks can increase pump operating time and extend the drying cycle.
Cleaning procedures must be adapted to the material being processed. Food and pharmaceutical applications may require defined sanitation methods, approved cleaning agents, and documented verification. If the same equipment processes different products, changeover procedures should be carefully designed to prevent cross-contamination.
Energy performance should be tracked over time. A gradual increase in cycle duration or electricity consumption may indicate vacuum leakage, fouled heat-transfer surfaces, refrigerant problems, pump wear, sensor drift, or incorrect loading practices. Preventive maintenance can protect both product quality and operating cost.
The standard BLK-FD-20 includes the integrated freeze-drying structure, double-layer radiant panels, central control, and residual cold recovery. Customers may require additional customization depending on their application.
Important configuration questions include whether the product is liquid, solid, granular, or mixed; whether the process requires high cleanliness; whether heat recovery is beneficial; whether steam or hot water is available; whether the product needs special containment; and whether the equipment must connect with upstream filling or downstream packaging systems.
The expected annual operating schedule is also important. A machine that operates several cycles per week may have different energy and maintenance priorities from a machine that operates continuously during a seasonal harvest. Batch scheduling affects the value of cold recovery because recovered energy is most useful when the next cooling demand occurs within a suitable time window.
Customers should also identify the target final moisture, acceptable cycle time, product temperature limits, and required rehydration performance. These parameters guide the design of process trials and may affect the choice of vacuum-pump capacity, refrigeration capacity, shelf-temperature range, condenser arrangement, and control functions.
Where product information is confidential, the supplier can work from general physical data and controlled sample testing. A technical proposal should clearly separate standard specifications, optional systems, expected performance, and conditions used to calculate capacity or energy-saving estimates.
A successful freeze-drying investment should serve more than the first product introduced by a company. It should provide a platform that can grow with the business. The BLK-FD-20 supports this objective by combining meaningful batch capacity with flexible product application.
For a start-up, it can provide a commercial-scale foundation without requiring the investment associated with a very large production line. For an established processor, it can add capacity for specialty products, seasonal materials, new product development, or regional production. For a research organization, it can connect laboratory results with industrially relevant processing conditions.
The equipment can also support phased investment. A company may begin with standard cold recovery and later add customized heat-recovery functions or other integration features as production volume increases. Dimensional customization allows the original machine to fit the available facility rather than forcing the facility to be redesigned around a rigid standard.
Energy efficiency contributes to long-term competitiveness. Reduced compressor load, recovered cold energy, integrated thermal circuits, and improved COP can lower production costs over repeated cycles. Shorter cycle times, where achieved through suitable process optimization, can increase annual throughput without increasing the number of chambers.
Consistency contributes to customer satisfaction. A product that looks, tastes, and rehydrates consistently is more likely to meet commercial specifications. Uniform shelf temperatures, controlled vacuum, and stable automation help reduce batch-to-batch variability and support stronger quality management.
Prospective users should begin with a clear product and capacity assessment. The supplier should receive information about product type, initial moisture, expected batch weight, tray thickness, target residual moisture, product temperature limitations, desired cycle time, and annual production volume.
The next step should be a sample trial or process-development study. Testing can determine freezing behavior, drying resistance, product shrinkage, rehydration quality, endpoint conditions, and practical throughput. It can also identify whether heat recovery, specialized tray materials, or additional controls are necessary.
Factory acceptance testing should verify mechanical completion, vacuum performance, temperature control, refrigeration operation, control logic, alarm functions, and safety interlocks. Customers should request documentation covering operating manuals, electrical diagrams, maintenance requirements, component lists, and recommended spare parts.
Site acceptance testing should confirm that the equipment performs properly under the customer’s actual utility and environmental conditions. The process should include representative loads rather than only an empty-chamber test. Production personnel should be trained during commissioning so that the equipment is operated correctly from the first commercial batch.
A total-cost comparison should include purchase price, installation, utilities, labor, maintenance, spare parts, cleaning, validation, packaging, and expected energy consumption. The lowest initial price does not always represent the lowest lifetime cost. A system with better energy recovery, stronger technical support, and more efficient space utilization may provide greater value over its operating life.
The BLK-FD-20 is a medium-sized pilot-to-production vacuum freeze dryer. It is intended for companies moving beyond laboratory processing and requiring meaningful batch capacity without installing a very large production line.
The standard freeze-drying area is 20 square meters. The equipment has a standard loading capacity of approximately 200 kilograms and a liquid loading capacity of up to 400 liters, subject to material density and process conditions.
Yes. The equipment uses an integrated pre-freezing and drying design. Materials can complete the freezing and drying stages within the freeze dryer, reducing transfers and helping maintain process continuity.
The rectangular chamber can provide better workshop space utilization and more efficient alignment with trays and radiant panels. It can also offer greater layout flexibility than a circular chamber of comparable capacity, particularly in medium-sized facilities.
The double-layer panels contain independent cooling and heating circuits. The upper layer is used for cooling and the lower layer for heating. This design is intended to provide more uniform shelf temperatures and more efficient transitions between freezing and drying.
The standard configuration includes a residual cold recovery system. Heat recovery is available as a customization option. The exact energy-saving benefit depends on product characteristics, cycle design, operating schedule, and site conditions.
The specified ultimate vacuum level is 10 pascals or lower. Actual operating vacuum during production depends on product load, moisture release, condenser conditions, sealing performance, and vacuum-pump operation.
Yes. The length, width, and height can be customized to suit workshop access, ceiling height, floor planning, utility locations, and production-flow requirements. Engineering confirmation is required before final construction.
The equipment can be used for many food, fruit, vegetable, herbal, medicinal, health-supplement, biological, and chemical materials. Each product requires its own process-development study because freezing and drying behavior varies considerably.
Yes. Remote monitoring through a mobile application is supported. Multiple language options can also be customized for international production teams.
It may be suitable for selected pharmaceutical, biological, and medicinal-material applications when configured and validated according to the required regulatory, cleanliness, containment, and documentation standards. Customers should define their compliance requirements before ordering.
Customers should provide product type, batch size, initial moisture, target final moisture, tray thickness, expected cycle time, annual production volume, facility dimensions, available utilities, and any special cleanliness or automation requirements. This information allows the supplier to recommend an appropriate configuration.
The BLK-FD-20 is designed for manufacturers that need a practical transition from experimental freeze-drying to reliable commercial processing. Its 20-square-meter drying area, 200-kilogram standard load, and 400-liter liquid capacity provide a useful scale for product development, market testing, specialty production, and medium-sized manufacturing.
Its major advantages arise from the way the system is integrated. Pre-freezing and drying are combined in one unit. The rectangular chamber is designed for efficient workshop layout. Double-layer radiant panels use independent cooling and heating circuits to support thermal uniformity. Standard cold recovery reduces wasted refrigeration energy, while optional heat recovery and heat-pump systems provide additional efficiency opportunities.
The equipment is also supported by intelligent centralized control, mobile monitoring, multilingual interface options, flexible dimensions, international-oriented design, and a manufacturing organization with experience in refrigeration, freeze-drying, engineering, installation, commissioning, and after-sales service.
Compared with conventional equipment that depends on separate freezing rooms, circular chambers, single-function radiant panels, duplicated energy systems, or limited control integration, the BLK-FD-20 offers a more coordinated approach. Its value is not limited to nominal capacity. It lies in the combination of product quality control, space efficiency, energy management, process flexibility, and long-term technical support.
For organizations evaluating a medium-sized lyophilizer, the most reliable decision should be based on product trials, complete-cycle energy data, factory and site acceptance testing, and a clear understanding of future production needs. When properly configured and operated, the BLK-FD-20 can provide a strong foundation for scaling freeze-dried products from development batches to repeatable industrial production.
1. Product technical specifications and application information for the BLK-FD-20 pilot-to-production freeze dryer.
2. General principles of vacuum freeze-drying, including freezing, primary drying, secondary drying, sublimation, and residual-moisture control.
3. Technical information concerning double-layer radiant-panel structures and independent cooling and heating circuits.
4. Technical information concerning integrated refrigeration and drying energy structures, including patent reference CN205784249U.
5. Technical information concerning radiant-panel and double-radiant-panel designs, including patent references CN209030727U and CN204392676U.
6. Technical information concerning cold-energy recovery systems, including patent reference CN206047043U.
7. Technical information concerning heat-pump and economizer systems, including patent reference CN209612254U.
8. European CE mechanical health and safety principles for industrial machinery.
9. General quality-management and equipment-commissioning practices for industrial food, biological, chemical, and pharmaceutical processing systems.
 2026/05/28
 2026/05/28
2026/05/28


 Custom Industrial Lyophilizer Freeze Dryer Manufacturers


 English
 русский
 Español
 Français
 Deutsch
 عربى